Engineering Showcase: Certified Interface Solutions
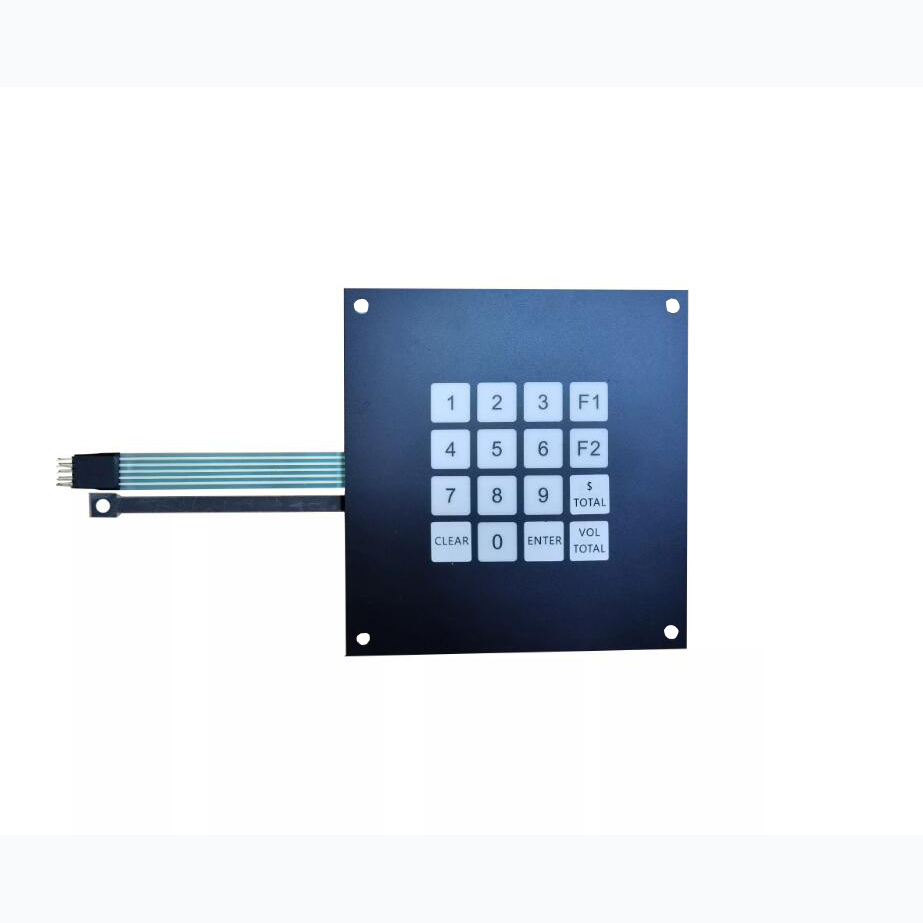
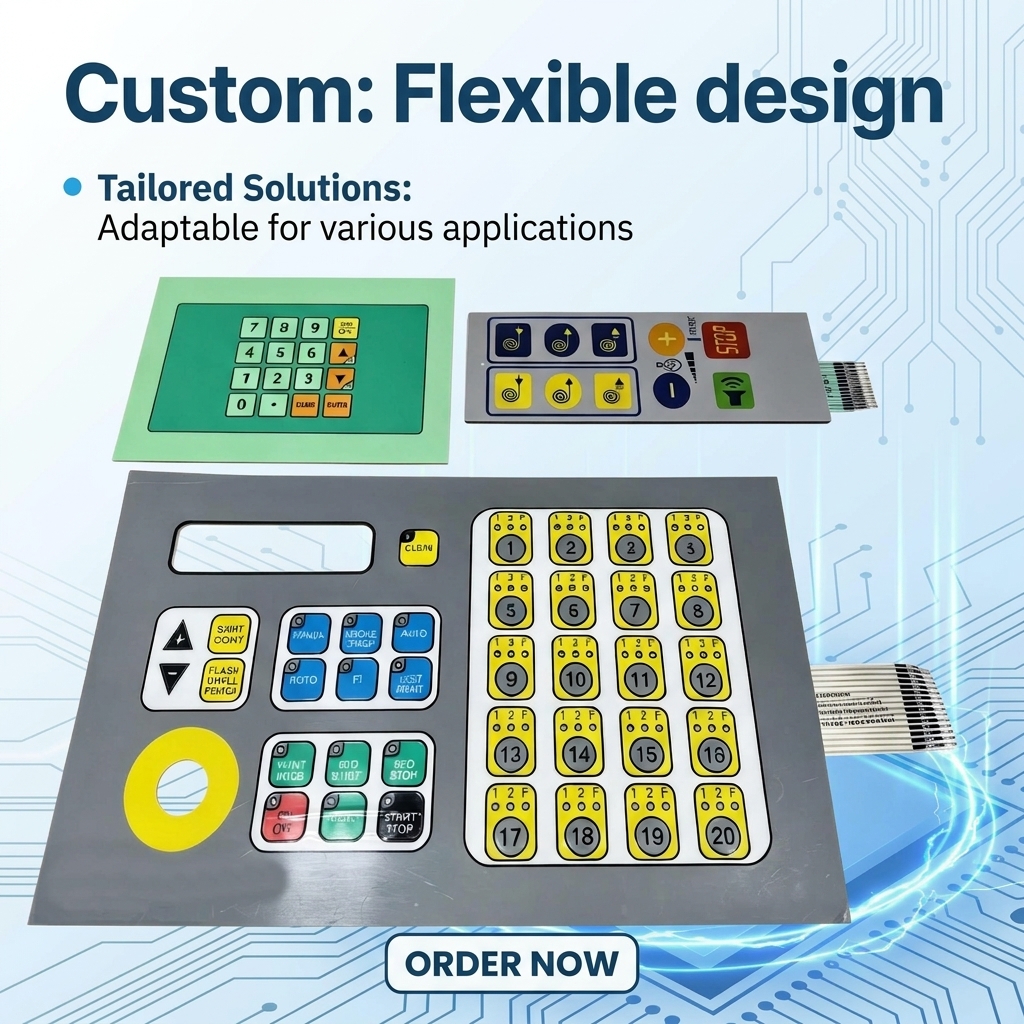
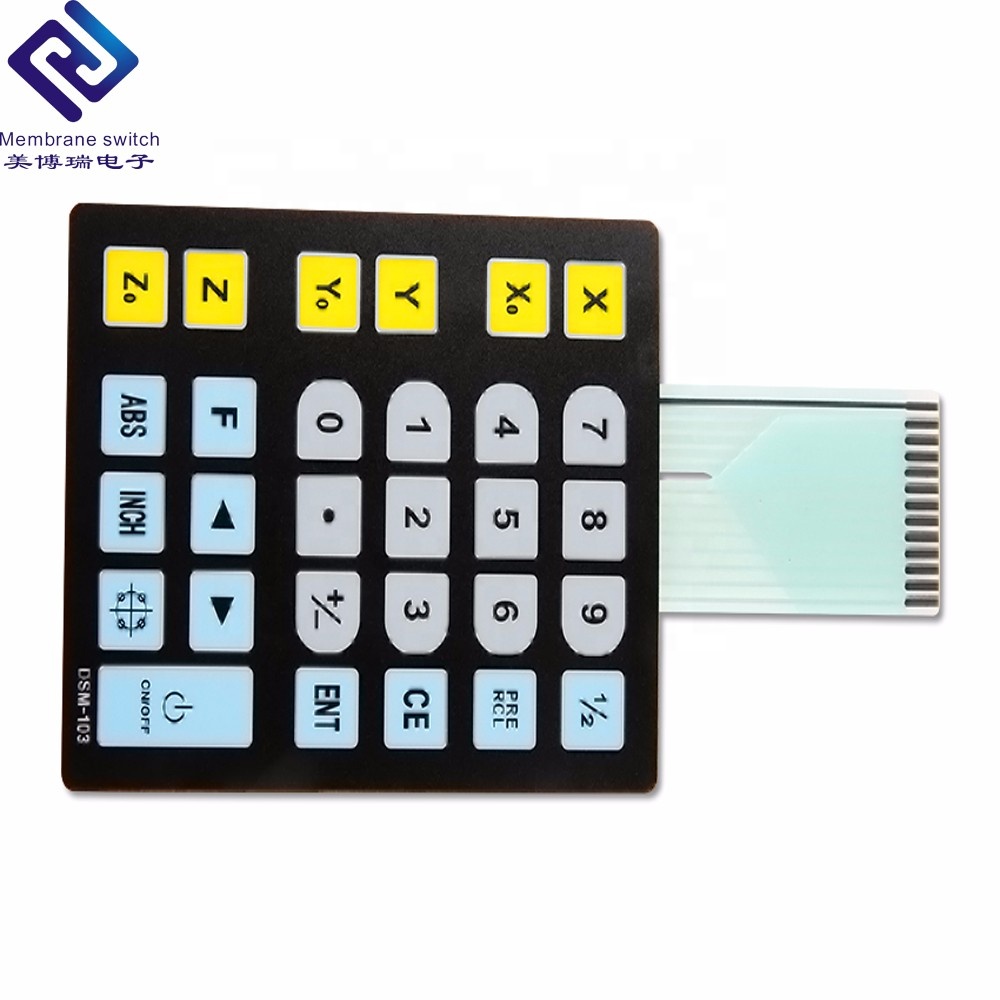
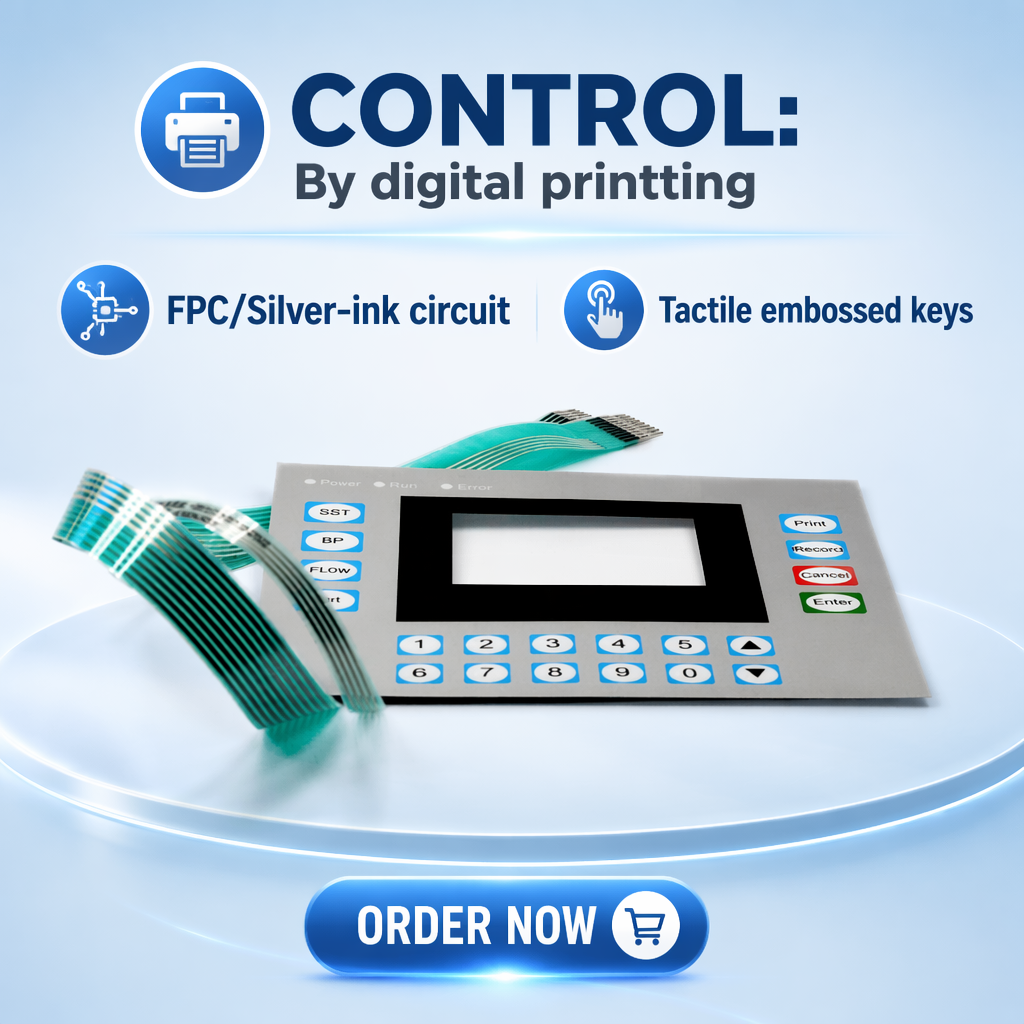
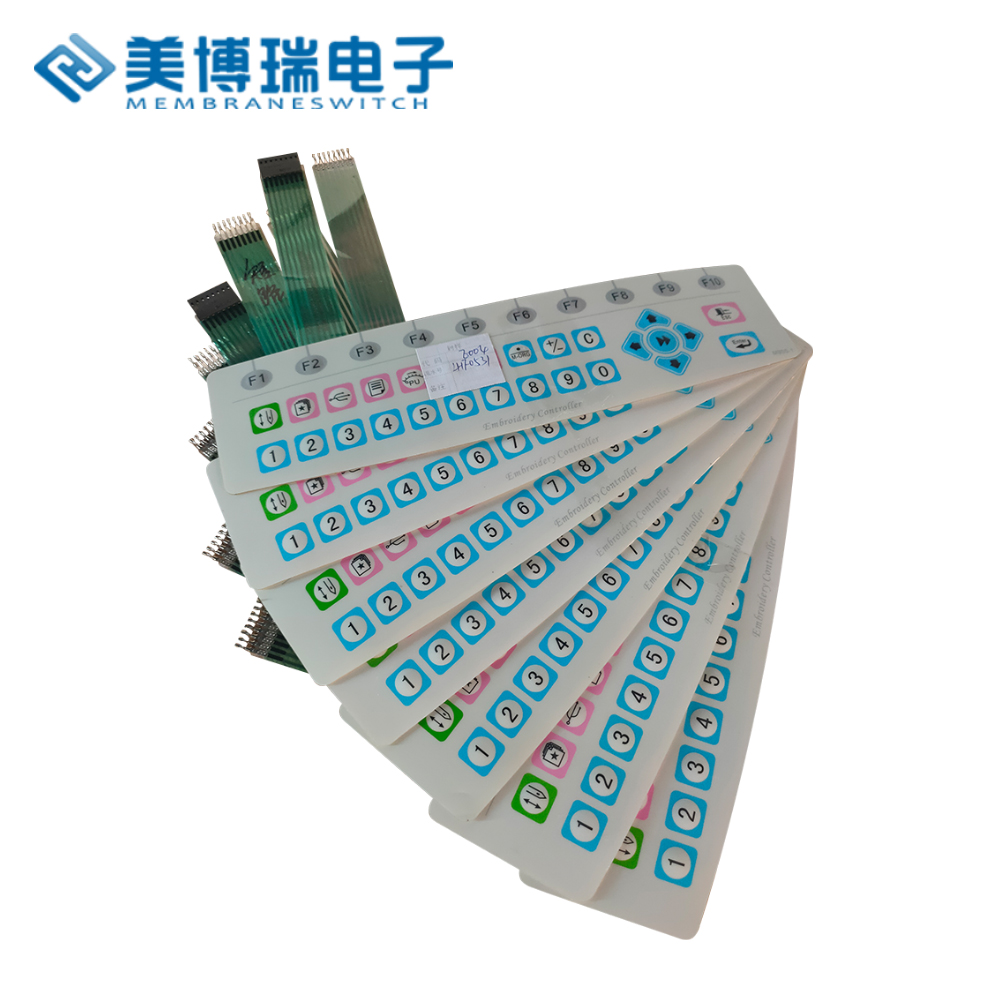
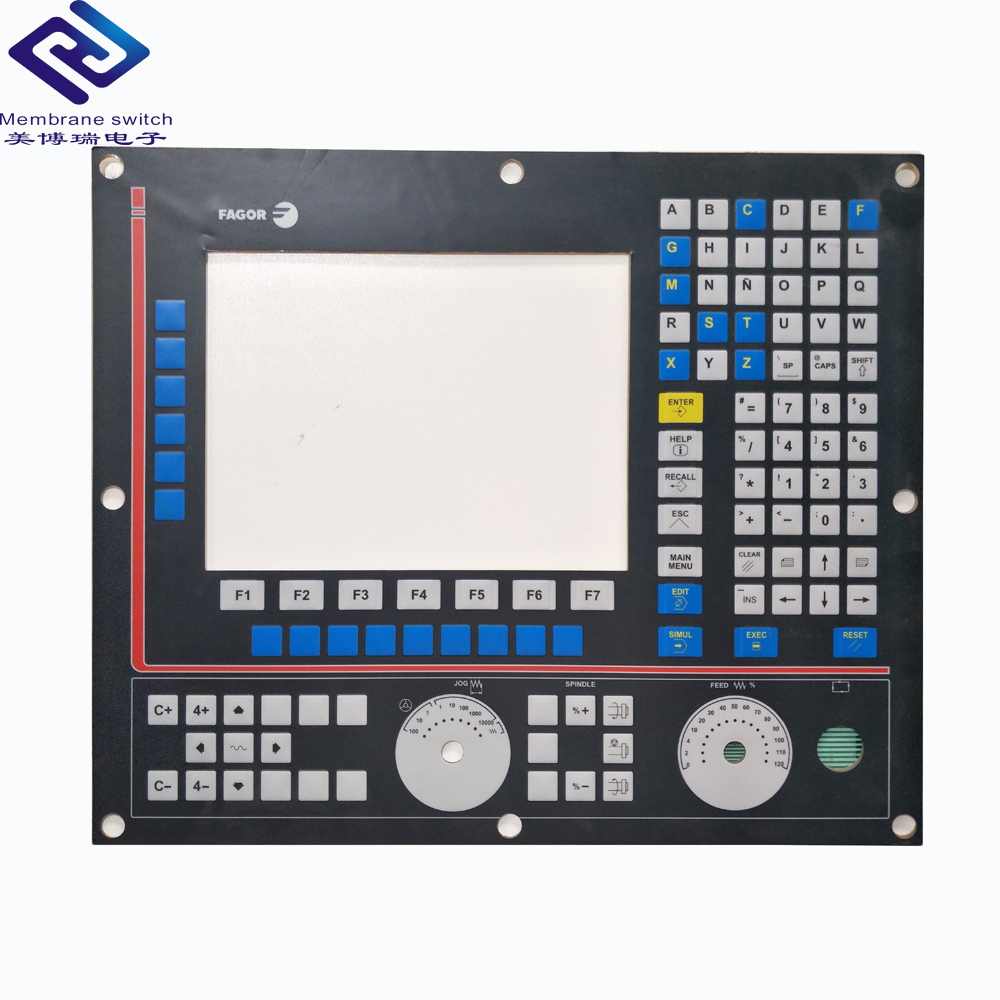
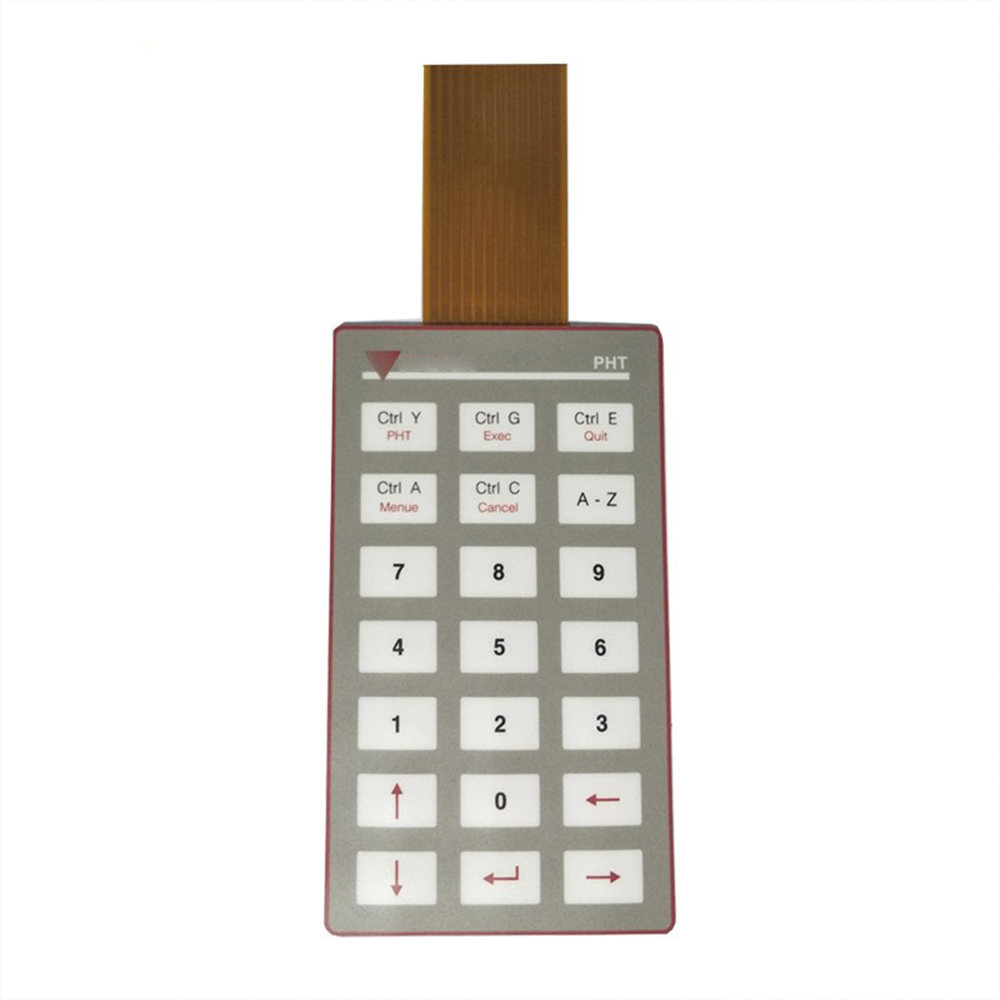
Precision-calibrated membrane keyboards, laser-etched silicone units, and flexible printed circuits optimized for industrial endurance and harsh operating climates.
1. The Strategic Mandate for CE & UKCA Compliance in Greater London
For hardware designers, tier-1 OEMs, and procurement specialists operating within the London-Oxford-Cambridge Innovation Corridor and the greater Thames Estuary industrial districts, selecting a human-machine interface (HMI) partner transcends dimensional tolerances. Following structural updates to European safety harmonization and post-Brexit statutory requirements, human-machine switches destined for high-integrity equipment must align simultaneously with CE (Conformité Européenne) directives and UKCA (UK Conformity Assessed) standards.
In high-density commercial hubs and municipal infrastructure across London—ranging from Transport for London (TfL) ticketing terminals to automated logistics centers in Dartford and clinical diagnostics centers in White City—control pads are subjected to aggressive operating cycles. A standard off-the-shelf keypad regularly suffers legend degradation, dielectric rupture, or contact impedance fluctuation when subjected to industrial sanitization agents and ambient condensation. True CE-marked laser-etched silicone and membrane assemblies resolve these failure modes through rigorous testing against the Low Voltage Directive (LVD) 2014/35/EU, Electromagnetic Compatibility (EMC) Directive 2014/30/EU, and the RoHS 3 Directive (EU) 2015/863.
EMC & RFI Attenuation
Integrated selective vacuum metal deposition and printed carbon-nickel grids deliver superior shielding effectiveness exceeding 65 dB from 30 MHz to 1.5 GHz, preventing spurious keystrokes in electrically noisy environments.
Extreme Actuation Fatigue
Stainless steel tactile domes (nickel or gold plated) combined with laser-ablated silicone actuators deliver tactile snap ratios above 45%, certified beyond 5,000,000 continuous switch cycles without tactile decay.
Hermetic Micro-Environment
Utilizing high-cohesion modified acrylic 3M 467MP/468MP laminates creates an airtight, moisture-impermeable internal cavity rated to IP67 and IP68, completely impervious to coastal dampness and particulate ingress.
2. Precision Laser Etching Mechanics: Optical Clarity & Material Morphology
Traditional silkscreen printing overlays legends onto top surface planes, leaving inks vulnerable to mechanical friction, micro-scratching, and aggressive chemical washing with solvent cleaners like IPA or chlorine-based biocides. Our computer-controlled multi-axis laser ablation process fundamentally transforms interface resilience by employing negative material removal.
The manufacturing process begins with optical-grade liquid silicone rubber (LSR) formulated with translucency calibrated between 88% and 93%. Key caps undergo dual or triple-tier spray coating: an inner high-opacity pigment (often pure optical white or high-saturation corporate colors) followed by an exterior polyurethane or UV-cured matte black coating. High-pulse-repetition Nd:YAG or fiber laser beams, controlled down to 0.02 mm focus spot sizes, systematically ablate the dark coating layer without degrading the underlying elastomer substrate. This creates razor-sharp alphanumeric legends and custom iconographies that illuminate cleanly when coupled with Light Guide Film (LGF) or direct SMT LEDs mounted on underlying flexible circuits.
| Performance Dimension | Silkscreen Surface Graphic | Laser Etched Coated Silicone | TAVO Hardcoated Sub-Surface PET |
|---|---|---|---|
| Abrasion Endurance (RCA Cycles) | < 75,000 cycles before legend lift | > 1,000,000 cycles (legend encapsulated) | > 5,000,000 cycles (reverse printed) |
| Night Vision / NVIS Backlight Uniformity | Irregular, edge hot-spotting | ±8% candela variation via micro-apertures | Balanced via optical diffusion layers |
| Chemical / Disinfectant Resistance | Susceptible to MEK, IPA & Bleach | Resistant to broad-spectrum medical sterilisers | Chemical hardcoat (3H-4H pencil hardness) |
| Tactile Ratio Stability (ΔF) | Subject to bubble collapse under heat | Stable -40°C to +125°C elastic recovery | Hermetically encapsulated snap domes |
| CE / BS EN 60529 Ingress Protection | Typically IP40 to IP54 max | IP66 to IP68 continuous submersion | IP67 with gas-tight perimeter gaskets |
3. British Regional Sourcing Vectors & Industry Applications
The UK manufacturing landscape is uniquely specialized, characterized by low-to-medium batch volumes of high-complexity, mission-critical systems. TAVO's engineering configuration is purposely tuned to address these technical clusters throughout Greater London and the home counties:
Cleanroom Bio-Tech & Healthcare Instrumentation (London Bioscience Innovation Centre, Whitechapel): Medical analysis suites, infusion pumps, and surgical laser controls require interfaces with strictly continuous planar profiles to avoid bio-burden traps. Our laser-ablated panels provide fully smooth or selectively tactile surfaces that withstand harsh hypochlorite wipedowns without legend fading or optical hazing.
Advanced Transport & Railway Infrastructure (Stratford, Park Royal, TfL Networks): Modern rolling stock driver cabin interfaces and passenger information points require compliance with BS EN 45545-2 (fire behavior and toxic fume emission). TAVO employs flame-retardant silicone compounds and halogen-free polyimide flexible printed circuits (FPC) engineered specifically for low smoke-density envelopes.
Subsea, Energy, & Extreme Fuel Processing (Thames Gateway Industrial Corridor): Petrochemical distribution centers, fuel dispenser pumps, and offshore pipeline diagnostic controllers demand spark-free intrinsic safety and barrier seals. Our ATEX-compatible tactile switches incorporate grounding meshes that drain static discharge harmlessly within microseconds, avoiding spark hazards in combustible atmospheres.
4. Complete Vertical Integration: Why Direct Factory Sourcing Outperforms Resellers
London procurement teams commonly source via local brokerages or component catalog distributors, incurring 35% to 65% middleman markups along with prolonged technical communication channels. TAVO Electronic Information Technology Co., Ltd. eliminates these inefficiencies by functioning as your direct manufacturing partner.
Drawing on foundational membrane switch manufacturing expertise dating back to 1990, our facility encompasses 2,219 square meters of verified cleanroom infrastructure located across the Xianghe Robot Industry Port and Huizhou electronics hubs. Our direct technical cooperation with German industrial partners provides European-tier dimensional disciplines backed by Chinese scale efficiencies.
60 CNC Precision Tooling Centers
We do not outsource toolmaking. In-house mold design and precision wire EDM drastically compress tooling delivery cycles from weeks to 5 business days, accelerating your time-to-market.
Mimaki UV Digital & Silkscreen Hybrid
Featuring 37 silkscreen stations alongside 4 high-definition Mimaki UV digital engines. This enables economical short-run prototypes without fixed plate tooling costs, scaling seamlessly into mass production.
Autonomous Reliability Testing Lab
Every lot is subjected to salt-fog corrosion chambers, button actuation life-cycle testers, xenon UV weathering tubes, and computer-automated continuity analysis for complete quality traceability.
5. Advanced Procurement Guidance: Avoiding Common HMI Failure Modes
When our engineers audit legacy keypad assemblies that have failed in UK outdoor environments, three underlying root causes repeatedly surface:
1. Silver Dendrite Migration Induced by Micro-Venting: In unsealed silver ink circuits, humidity coupled with continuous DC bias triggers electrochemical migration, generating silver dendrites across circuit tracks that cause catastrophic short circuits. TAVO prevents this failure by employing carbon-overprinted protective caps or transiting critical applications to copper-etched Polyimide FPC substrates with zero migration risk.
2. Adhesive Delamination at Thermal Extremes: Cheap synthetic rubber glues fail when components expand and contract under severe thermal shifts. We exclusively employ genuine 3M acrylic adhesive transfer films (such as 3M 200MP, 300LSE for low surface energy plastics, and VHB structural bonds) laminated within precise hygrometric and thermal windows.
3. Polycarbonate Yellowing & Embrittlement: Standard standard-grade polycarbonates deteriorate under outdoor UV exposure. For UK-bound equipment exposed to the elements, our bill of materials specifies Autotex XE UV-resistant textured polyester films, which resist yellowing and embrittlement for over a decade of continuous outdoor exposure.
Frequently Asked Questions by London Engineers & Procurement Officers
Key technical, commercial, and regulatory questions regarding custom membrane switches and laser etched keypads.
Q1: How does TAVO ensure compliance with both CE and UKCA directives?
We supply full Technical Construction Files (TCF), material Declarations of Conformity (DoC), and accredited third-party lab testing certifications covering RoHS 3, REACH, and EMC emissions. Whether your product is targeted for continental Europe or the domestic UK market, our documentation completely satisfies local statutory requirements.
Q2: What are the standard lead times for custom laser-etched prototypes shipped to the UK?
Leveraging in-house CNC mold production and laser cutting capabilities, functional engineering prototypes are typically completed within 7 to 10 working days following artwork and schematic sign-off. Air express delivery via DHL/FedEx to Heathrow or London Stansted takes approximately 3 to 4 business days.
Q3: Can you achieve uniform backlighting with variable color schemes on one keypad?
Yes. By combining ultra-thin Light Guide Film (LGF) with side-firing bi-color or RGB SMT LEDs mounted on a flexible circuit layer, we can direct illumination precisely to selective laser-etched legends while preventing cross-talk light leakage between adjacent keys.
Q4: How do you accommodate low-volume, high-mix development cycles?
Unlike rigid volume manufacturers who demand MOQ commitments of thousands of units, our digital UV printing and direct laser ablation workflows allow us to support prototype validation batches and low-volume pilot builds without prohibitive NRE tooling charges.
Q5: What design files are required to initiate an engineering review?
We accept CAD mechanical outlines in DXF, DWG, or STP formats, combined with vector graphic legends in AI, PDF, or CDR files specifying Pantone or RAL color references. If electrical integration is involved, a circuit schematic or pin-out diagram ensures our team optimizes your circuit layout accurately.
Q6: How do you prevent ESD strikes from destroying sensitive internal electronics?
We integrate full perimeter wrap-around shielding layers composed of aluminum foil, copper flex sheets, or printed conductive carbon-silver ground grids. This dissipates electrostatic discharges up to 15 kV harmlessly away from microcontrollers and display drivers.
Accelerate Your HMI Development Cycle
Consult directly with our senior application engineers. We evaluate your drawings, recommend cost-effective stack-up architectures, and deliver detailed DFM reports within 24 hours.
Inquire Now