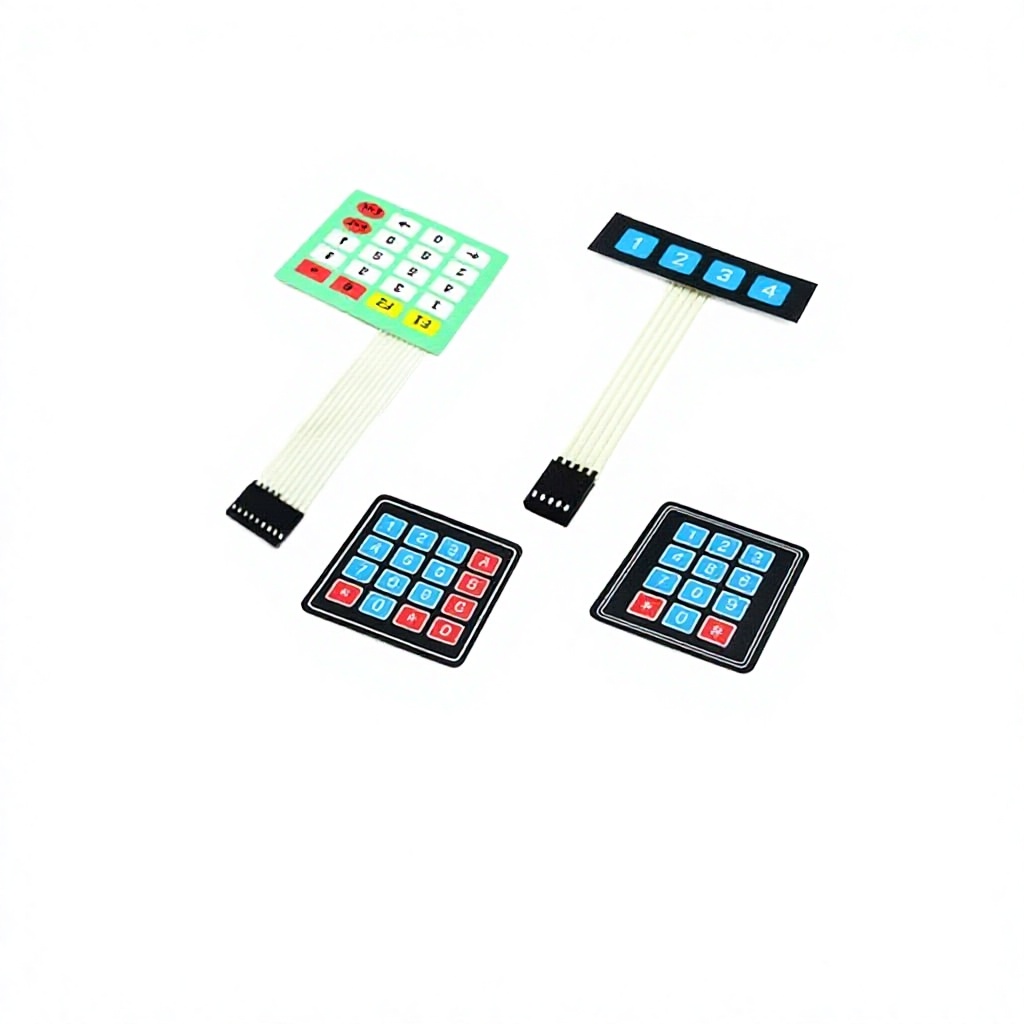
Precision Manufacturing Portfolio
Recommended Backlit Membrane Switches & Flexible Assemblies
Explore custom-engineered interface modules designed for high duty cycles, luminous uniformity, and superior environmental resistance in Panamanian operating conditions.
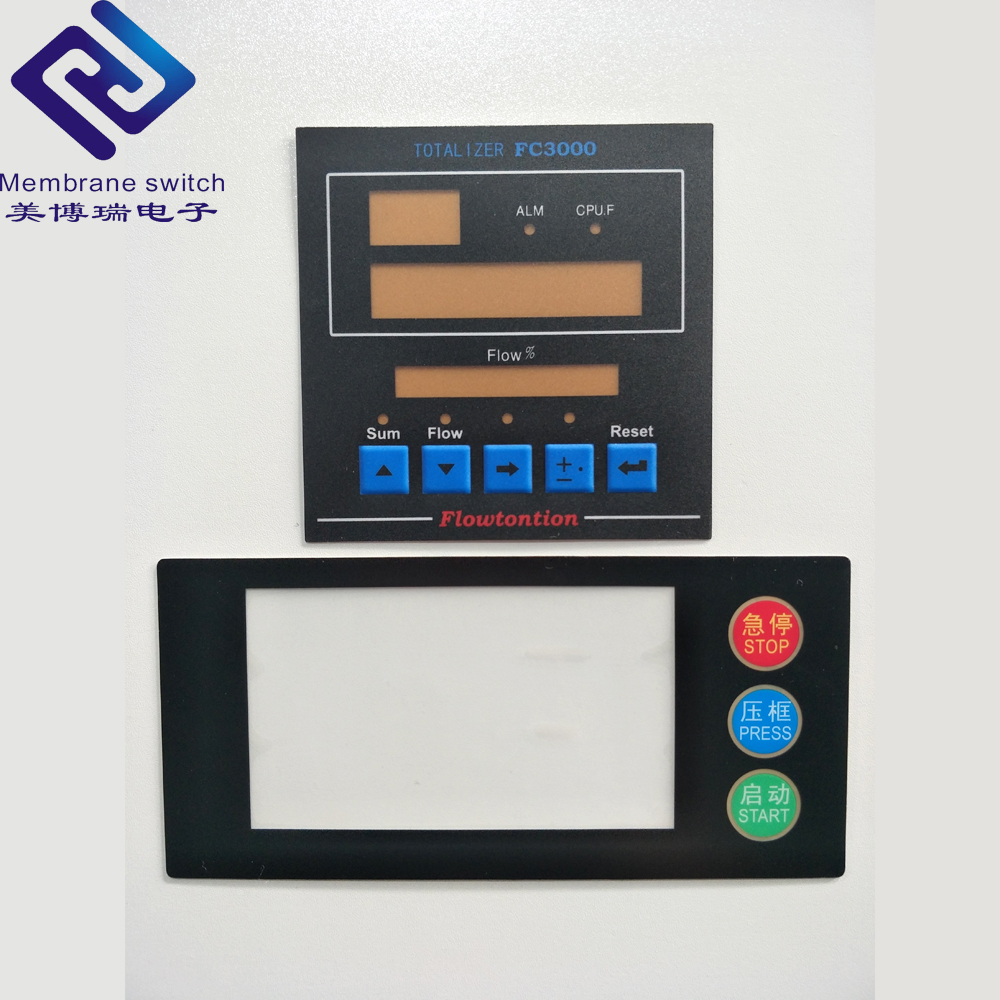
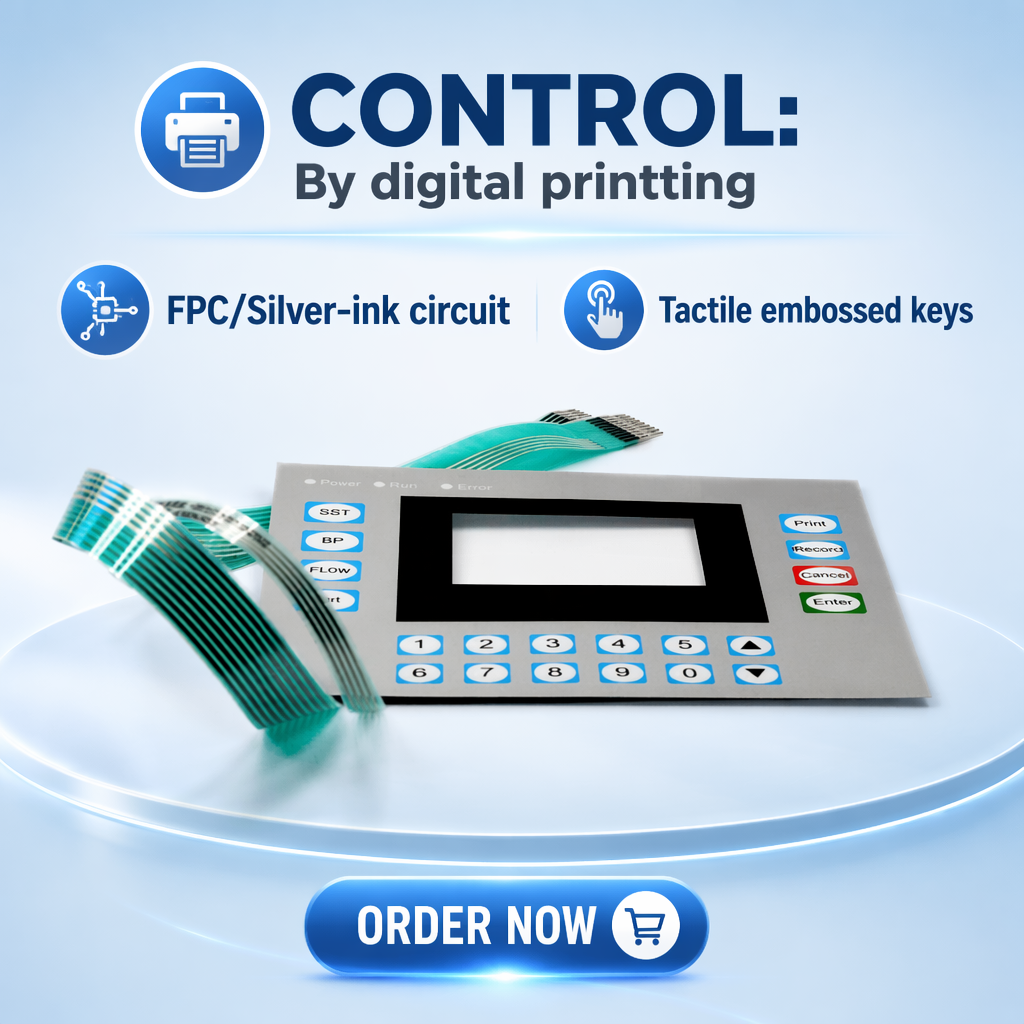
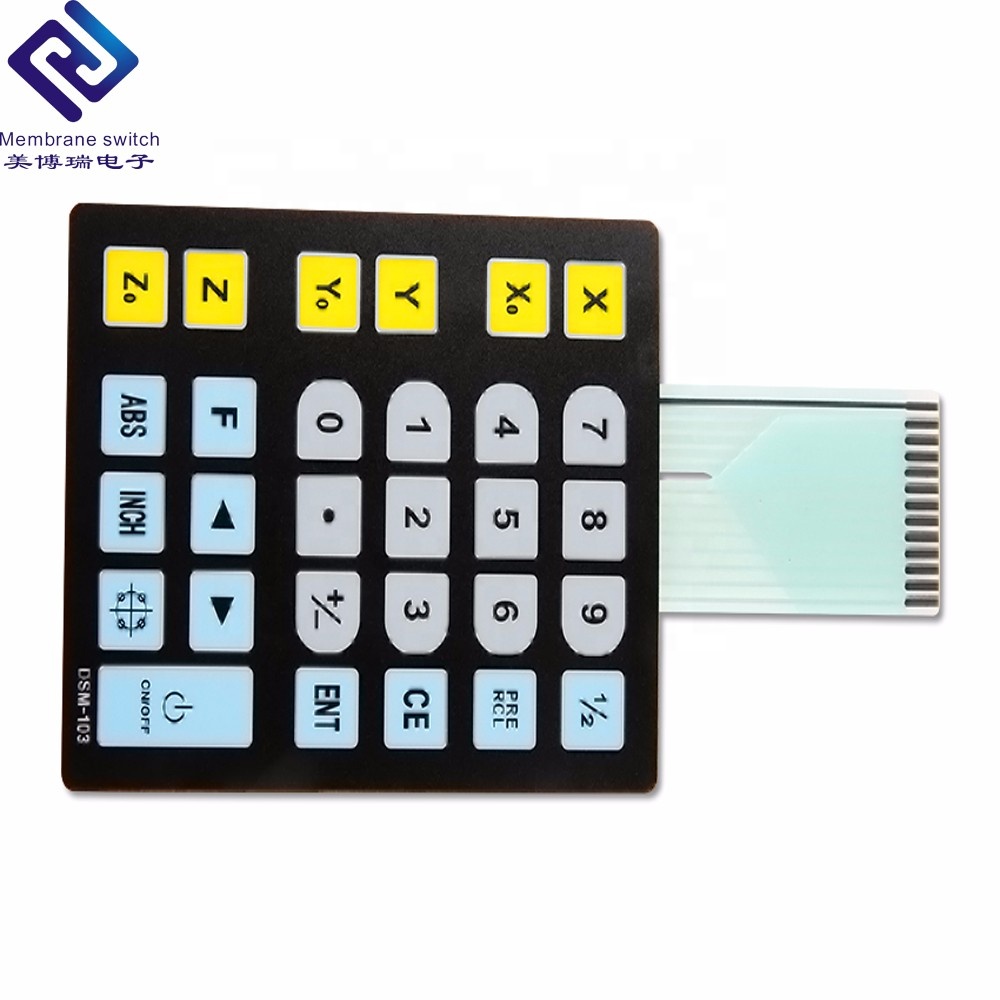
Whitepaper Technical Overview
Engineering Backlit Human-Machine Interfaces for Mission-Critical Reliability
Analyzing light guide films (LGF), embedded surface-mount LEDs, and barrier encapsulation for harsh tropical environments.
In modern industrial automation, interoceanic logistics, and marine navigation systems, the backlit membrane keypad serves as the definitive point of physical interaction between human operators and advanced control logic. Unlike conventional mechanical switches or unlit elastomeric overlays, an integrated backlit membrane assembly must resolve competing physical challenges: maintaining absolute IP67 hermetic sealing against aggressive moisture while providing uniform, color-calibrated illumination across intricate tactile switch layouts.
For industrial design teams deploying hardware into coastal and equatorial regions such as Panama, standard commercial silver-printed membranes frequently suffer premature micro-cracking, silver migration, and delamination due to high relative humidity (>85%) combined with elevated ambient temperatures. As a premier Chinese manufacturer specializing in high-reliability HMI production, TAVO combines proprietary multi-layer laminations, precision-etched Flexible Printed Circuits (FPC), and microscopic optical dot-patterning on Light Guide Films (LGF) to guarantee over 1,000,000 actuation cycles without luminous decay or electrical failure.
1990
Membrane Switch Manufacturing Heritage
1,000,000+
Switch Actuation Rating (Stainless Domes)
IP67 / NEMA 4X
Waterproof & Salt Fog Certified Enclosure
100%
Automated Optical & Electrical Testing
Thin Light Guide Film (LGF) Systems
Utilizing micro-replication dot matrices embossed onto 0.125mm–0.25mm optical-grade polycarbonate, LGF assemblies redirect side-firing ultra-compact SMD LEDs across entire key legends. This eliminates bright spots (hotspotting), minimizes total profile thickness to under 1.2mm, and slashes power consumption by up to 70% compared to direct-backlit LED matrix boards.
Surface-Mounted Discrete LED Integration
Direct SMT component bonding upon treated polyester circuits or polyimide FPC layers permits targeted keycap highlighting, multi-color state annunciation (Red/Green/Amber/Blue), and backlit brand badging. Embedded LEDs are potted in UV-curable dielectric resins to insulate against vibrational stress, thermal cycling, and humidity intrusion.
Electroluminescent (EL) & Fiber Optics
For ultra-uniform, shadow-free backlighting across low-profile keyboards, EL phosphor layers deliver balanced glow in green, blue-green, and white wavelengths. Combined with woven optical fiber mesh backlighting, these solutions deliver zero electromagnetic interference (EMI) for precision aerospace and sensitive marine radio communication interfaces.
Regional Engineering Adaptations
Localized Backlit Membrane Applications in the Republic of Panama
Addressing the severe environmental and operational criteria dictated by Panama's pivotal logistics corridors, ports, and industrial infrastructure.
Maritime Systems & Canal Tugboat Automation
Operating inside the Panama Canal corridor (Balboa, Cristobal, and Cobre Panamá port terminals) exposes consoles to constant saline mist, heavy spray, and high solar UV. Our IP67-rated backlit membrane keypads employ Autotex XE UV-resistant hardcoated polyester and non-corroding 3M 300LSE/VHB high-tack adhesives. Nighttime pilot navigation demands variable-dimming LGF backlighting (NVIS compatible) preventing nocturnal blindness during lock transits.
Cold Storage, Logistics & Colón Free Trade Zone Hubs
As the premier redistributor of Latin America, the Colón Free Trade Zone (Zona Libre de Colón) operates massive chilled pharmaceutical and agro-export cold storage facilities. Our customized membrane keypads feature specialized low-temperature sub-surface acrylic adhesives functioning down to -40°C, paired with stainless steel tactile domes (snap force: 300g–450g) ensuring crisp tactile confirmation even through heavy thermal gloves.
Tropical Agro-Industrial & Beverage Processing
From coffee processing hubs in Chiriquí to sugar refineries in Aguadulce and brewing plants in Panama City, HMI terminals must withstand high-pressure washdowns (IP66/IP67) containing acidic cleansers and caustic sterilizers. Our continuous front graphic overlays prevent microbial colonization, dust ingress, and chemical degradation while backlit legends provide clear operational prompts in steam-laden control rooms.
Emerging Industry Trajectory
Macro Trends Shaping Membrane Keypad Adoption Across Panama
How industrial digitization, infrastructure expansion, and nearshoring trends influence HMI component procurement.
Accelerated Port Automation (Panama Ports & Rail)
The transition toward semi-autonomous rubber-tired gantry (RTG) cranes, terminal tractors, and railway signaling demands rugged interfaces capable of 24/7 continuous duty. Procurement engineers are systematically replacing standard mechanical pushbuttons with backlit membrane panels equipped with aluminum backplates, achieving electromagnetic immunity (EMI/RFI shielding) and resistance to heavy shock loads.
Nearshoring & EMMA Special Economic Regimes
Under Panama's SEM (Multinational Headquarters) and EMMA (Manufacturing Services for Multinational Companies) frameworks, regional assembly and engineering facilities are growing rapidly. This trend creates acute demand for agile prototyping, fast custom iterations, and certified turnkey HMI assemblies shipped reliably from China's primary manufacturing hubs with complete international compliance paperwork.
Hybrid Capacitive Touch & Backlit Membrane Switches
Panamanian medical device integrators and municipal smart infrastructure developers increasingly select hybrid interfaces. These combine high-clarity scratch-resistant polycarbonate overlays, transparent OCA optical windows for display screens, and capacitive touch sensors surrounded by localized LGF backlit perimeter keys—marrying clean, modern aesthetics with rugged environmental survivability.
Integrated Manufacturing Superiority
Why Engineering Teams Choose TAVO as Their Chinese Partner
Full in-house process ownership, Intertek-verified facilities, and three decades of specialized switch fabrication.
Complete Closed-Loop Production
End-to-End In-House Control: From CAD to Precision Assembly
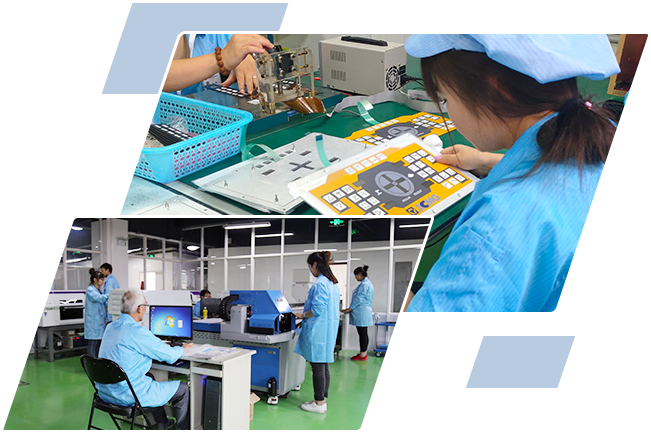
Unlike trading intermediaries, TAVO executes every phase of membrane switch fabrication under our own roofs across our dual facilities in Xianghe (Robot Industry Port, Hebei) and Huizhou (Guangdong). With over 2,219 m² of verified production space and 111+ dedicated specialists, we eliminate third-party subcontractor delays and unmonitored quality variations.
37 Silkscreen Printing Units
4 Mimaki UV Digital Presses
18 Precision Laser Cutters
60 CNC Mold Processing Stations
7 Digital Engraving Systems
Rigorous Testing & Reliability
Certified to ISO 9001 with Intertek Onsite Verification
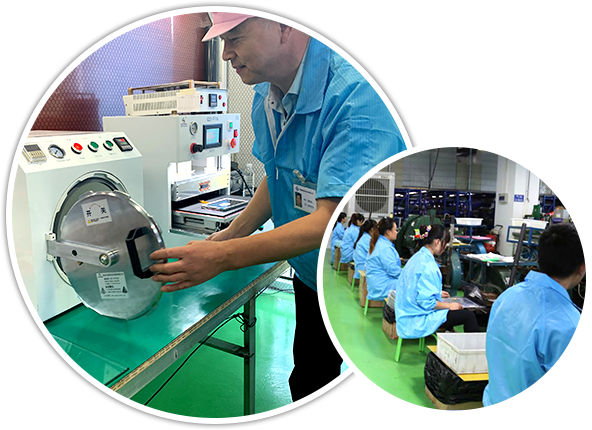
Every keypad intended for Panamanian deployment undergoes strict validation in our on-site environmental and electrical reliability laboratories. We subject switches to continuous programmable temperature and humidity stress (-40°C to +85°C at 95% RH), accelerated xenon UV degradation, cyclic automated salt fog testing (ASTM B117), and computerized 100% circuit loop resistance verification.
Automated Circuit Loop Testers
Actuation Life-Cycle Simulators
Salt Spray Corrosion Chambers
Xenon Arc Weatherometers
German Technical Cooperation
Global Export Competence
Proven International Supply Chain for Latin American OEMs
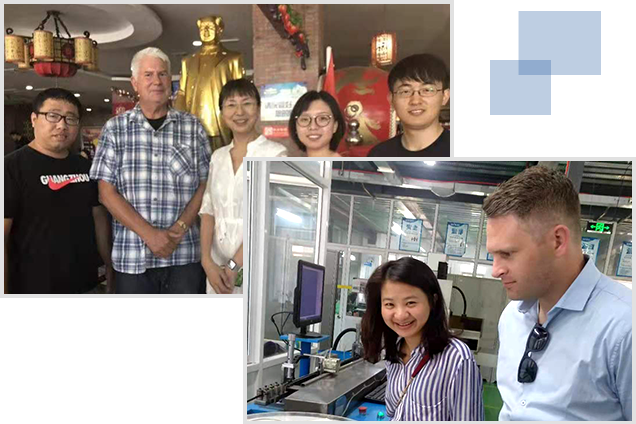
TAVO ships more than 1,000,000 units annually to highly regulated markets across Germany, the United States, Canada, and Western Europe. Our dedicated 20-person foreign trade division coordinates seamless delivery under FOB, CFR, CIF, and EXW terms, providing custom export crating, moisture-proof barrier foil packing with desiccant indicators, and full commercial documentation compliant with Panamanian customs clearance (Aduanas de Panamá).
FOB / CIF / CFR / EXW Delivery
T/T, L/C, D/P Flexible Terms
Confidential NDA Agreements
Low Prototyping MOQ
4.9/5 Global Buyer Satisfaction
Procurement Intelligence
Frequently Asked Questions by Panamanian Buyers
Technical, logistical, and commercial guidelines for engineers and procurement managers sourcing custom membrane keypads from China.
How do you protect backlit membrane keypads against Panama's extreme humidity and maritime salt air?
To prevent silver trace oxidation, electromigration, and short-circuits caused by high humidity (>85% RH) and coastal saline atmospheres, we employ three engineering safeguards: First, we utilize etched Copper Flexible Printed Circuits (FPC) with polyimide encapsulation or print high-density carbon dielectric overcoats on silver conductive inks. Second, we integrate peripheral water-barrier gasket tracks (IP67 submersible seal) using genuine 3M 300LSE acrylic adhesives or closed-cell polyurethane foam spacers. Third, all SMD LEDs and internal solder joints are sealed beneath moisture-impervious UV optical adhesives.
Can we order small prototype batches before committing to high-volume production for Panama projects?
Yes. Unlike conventional factories requiring thousands of units per run, TAVO supports agile engineering development. By leveraging Mimaki digital UV printing systems and computer-guided laser plotting machines, we produce prototype evaluation units (5 to 50 pieces) without the heavy tooling costs associated with steel-rule die sets and silkscreen stencils. Once your hardware layout is verified in Panama, we seamlessly transition the project to automated high-volume production.
What CAD files, graphic formats, and engineering specifications must we supply to initiate tooling?
To commence production drawings, provide: 1) Graphic artwork in vector format (.AI, .CDR, .EPS, or .PDF) referencing exact Pantone Matching System (PMS) color codes; 2) Mechanical dimensions and hole cutouts in .DXF or .DWG format; 3) Circuit schematic or pin-out table detailing key matrix intersections, LED polarity, and connector tail pitch (e.g., standard 1.0mm, 1.27mm, or 2.54mm pitch Female/Nicomatic/FCI housings); 4) Operating environment parameters. Our 10-person CAD engineering team generates a comprehensive approval drawing for your engineering sign-off prior to fabrication.
What are the standard lead times and shipping methods from your factory to Panama?
Rapid prototype units typically ship within 7–10 business days following technical drawing approval. Standard mass production runs (500 to 20,000 units) require 15–20 business days. For urgent deliveries to Panama City or Colón, air express couriers (DHL, FedEx, UPS) deliver door-to-door in 5–8 business days via Tocumen International Airport (PTY). For large freight orders, sea container shipments transit directly from Shenzhen or Tianjin ports to Balboa or Manzanillo International Terminal (MIT) in approximately 24–30 sailing days.
Can you integrate rigid aluminum plates, PCB backer boards, and LCD display windows into the keypad?
Absolutely. Over 40% of our production comprises integrated turnkey assemblies. We laminate membrane keypads directly to CNC-milled aluminum backers (with threaded mounting studs and PEM nuts), rigid FR4 PCB motherboards containing soldered SMT microcontrollers, and optically bonded (OCA) anti-glare acrylic or polycarbonate windows for LCD and OLED screens. This provides a plug-and-play front-panel module that drops directly into your final equipment chassis.
What international payment terms, trade currencies, and quality warranties do you provide?
We accept wire transfer (T/T), Letter of Credit (L/C at sight), and D/P or D/A terms settled in USD (the official legal tender in Panama) or CNY. All shipments are supported by an ISO 9001 Certificate of Conformance (CoC), 100% electrical test reports, and a standard 12-month quality replacement warranty against manufacturing or material defects.
Request Complete Backlit Membrane Technical Catalog & Design Guide
Connect with our senior engineering team to receive full material stack-up diagrams, LGF illumination benchmarks, tactile force recommendations, and custom sample kits for Panamanian OEM and replacement projects.
Get Catalog