Fast Delivery
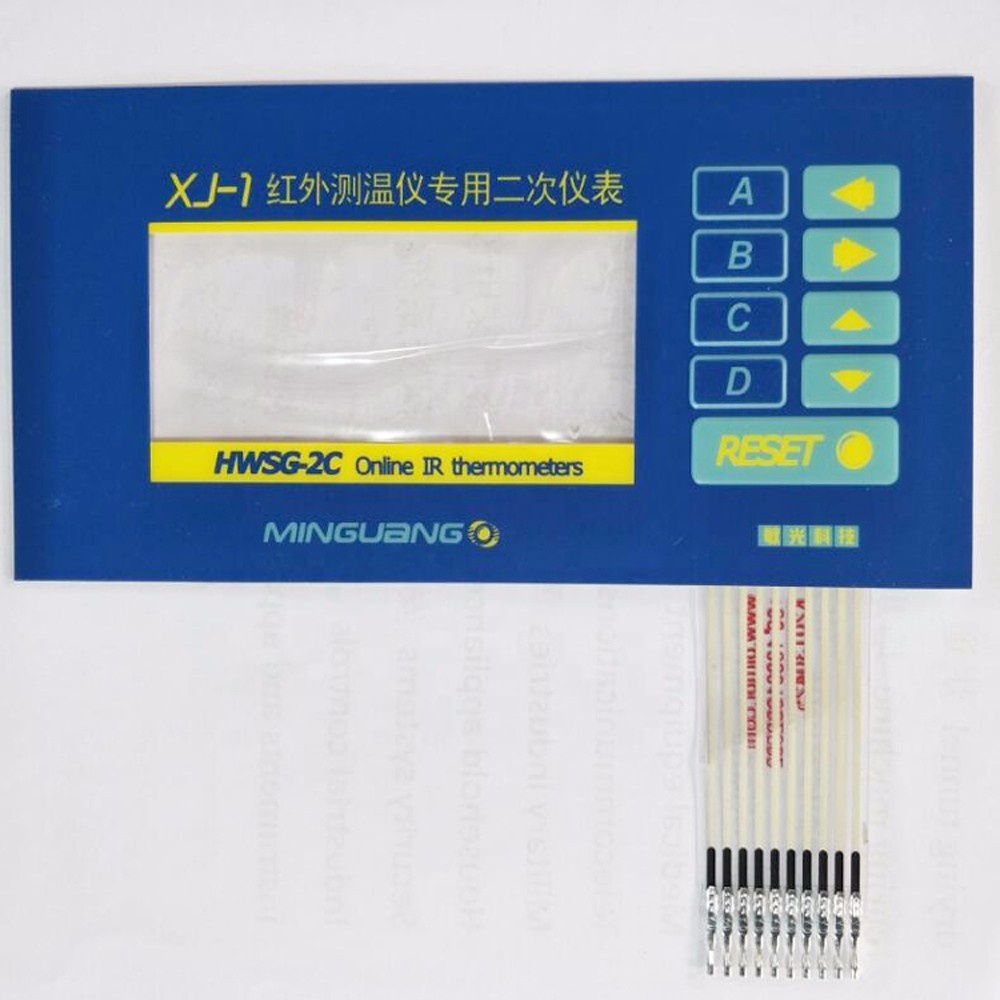
Fast Delivery OEM PBT Keyboard Cap Mechanical Switch Compatible 2.54mm Pitch
- Wear-resistant PBT Keycaps
- Silkscreen / Sublimation Font
Engineered for high-duty cycling, rigorous ingress protection, and vivid illumination across Oceania's demanding environments.
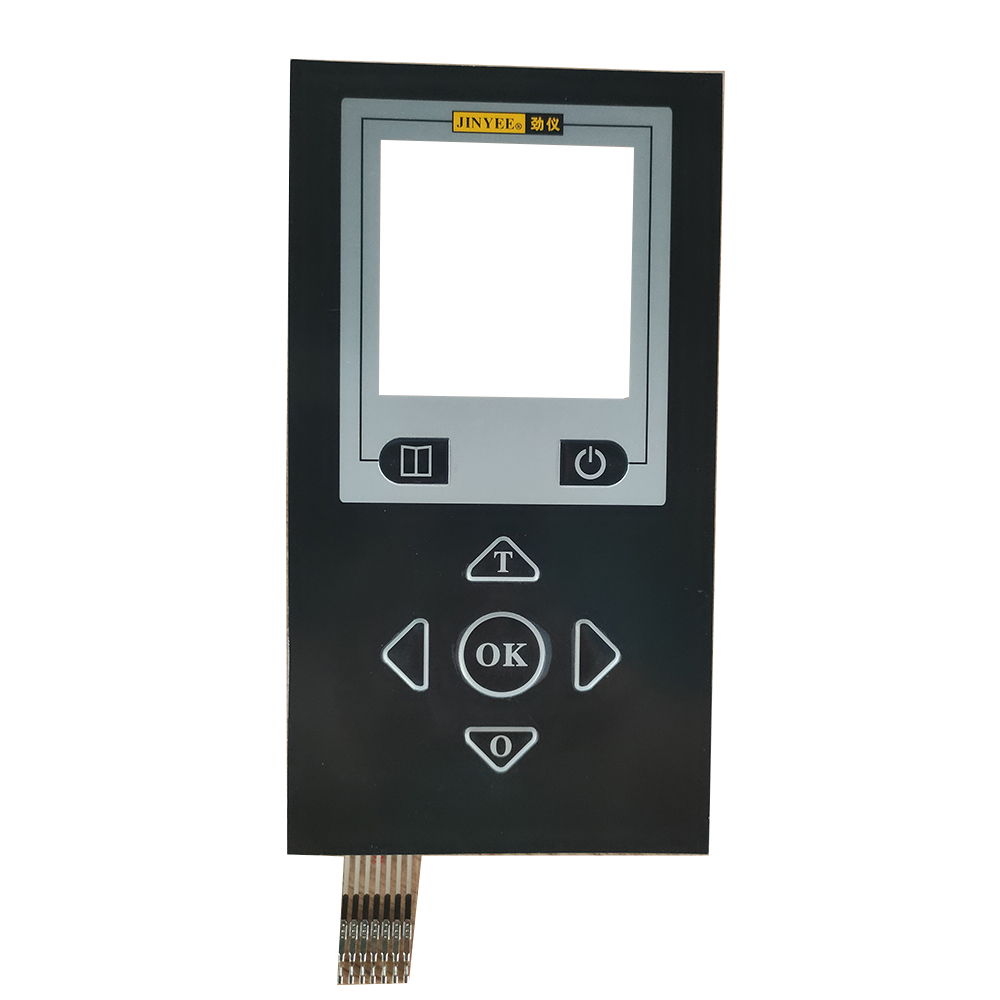
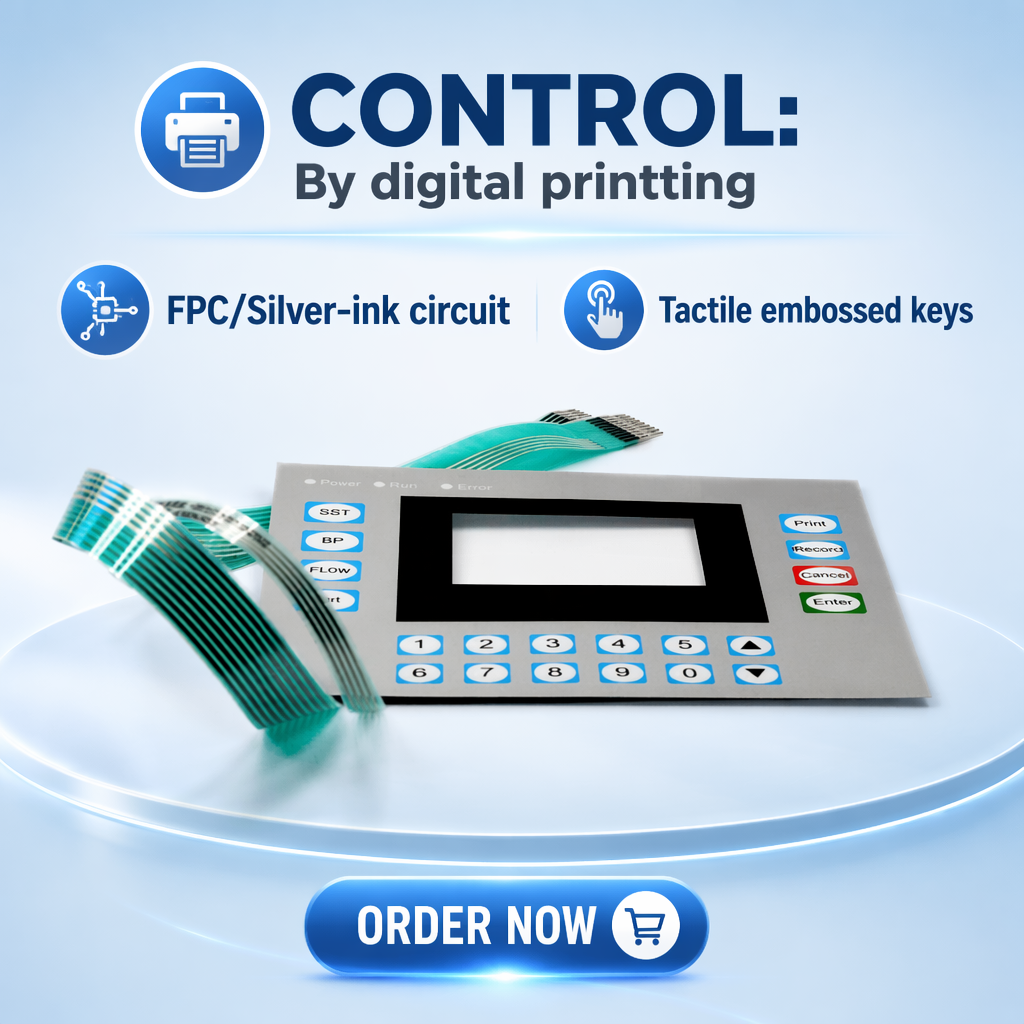
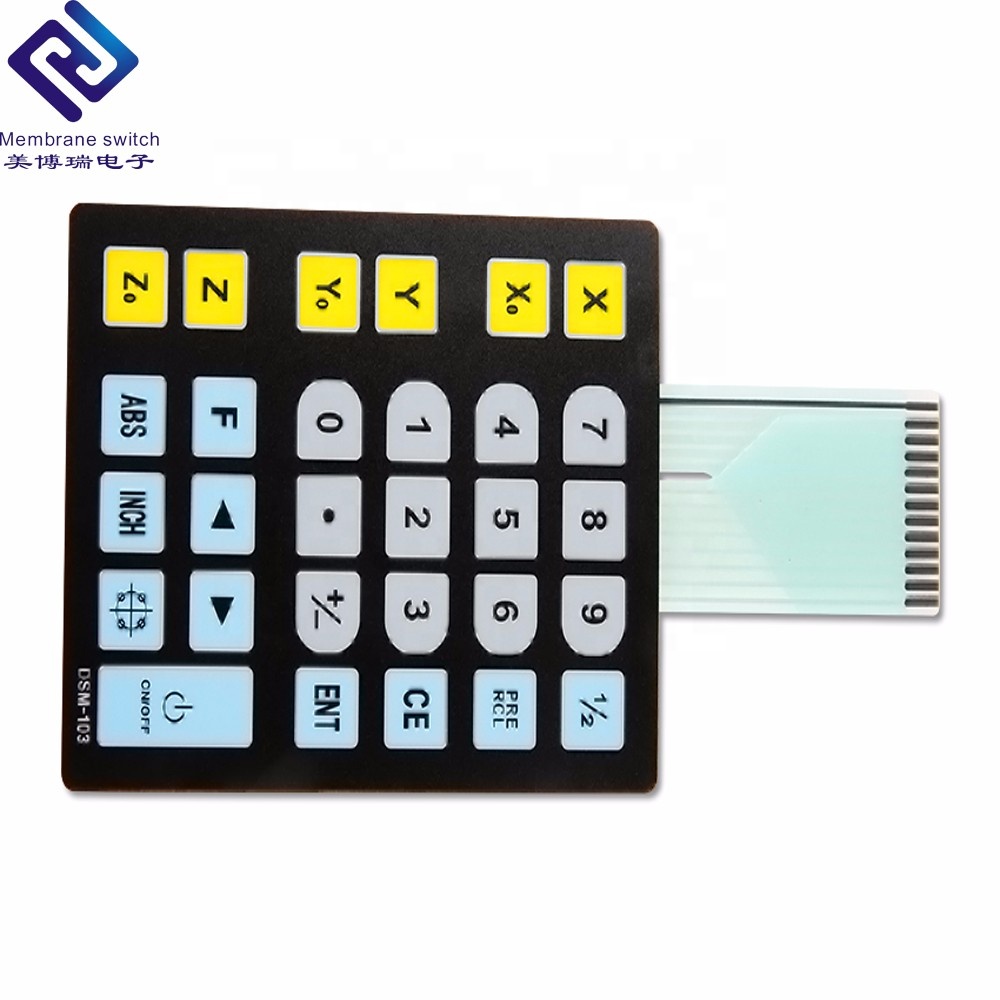
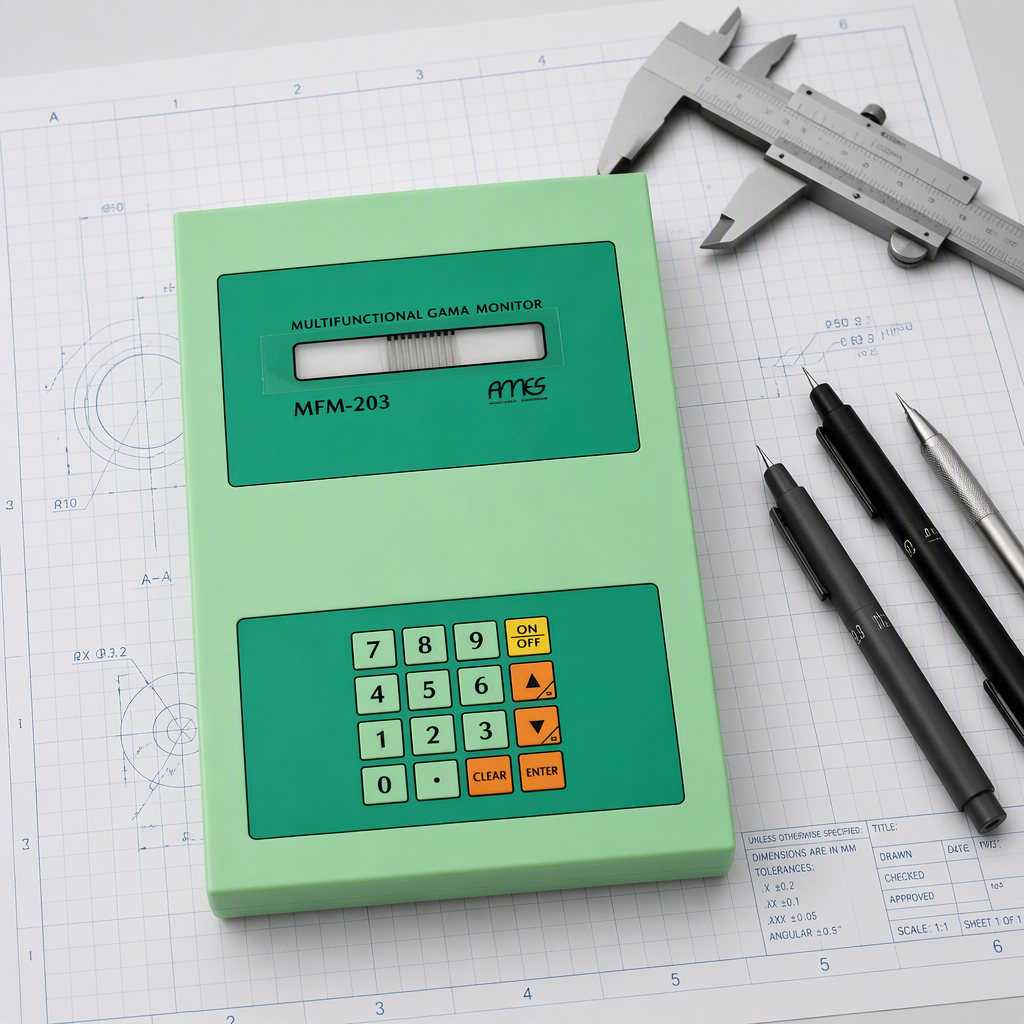
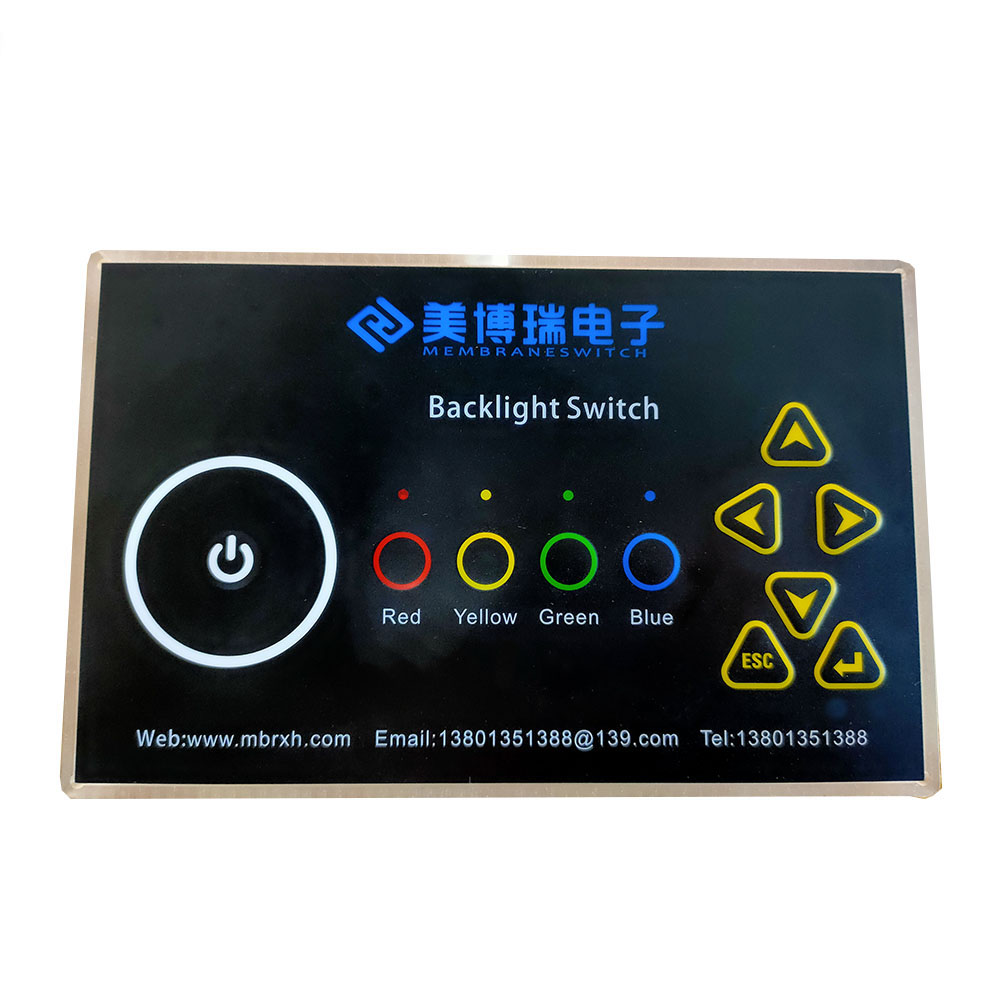
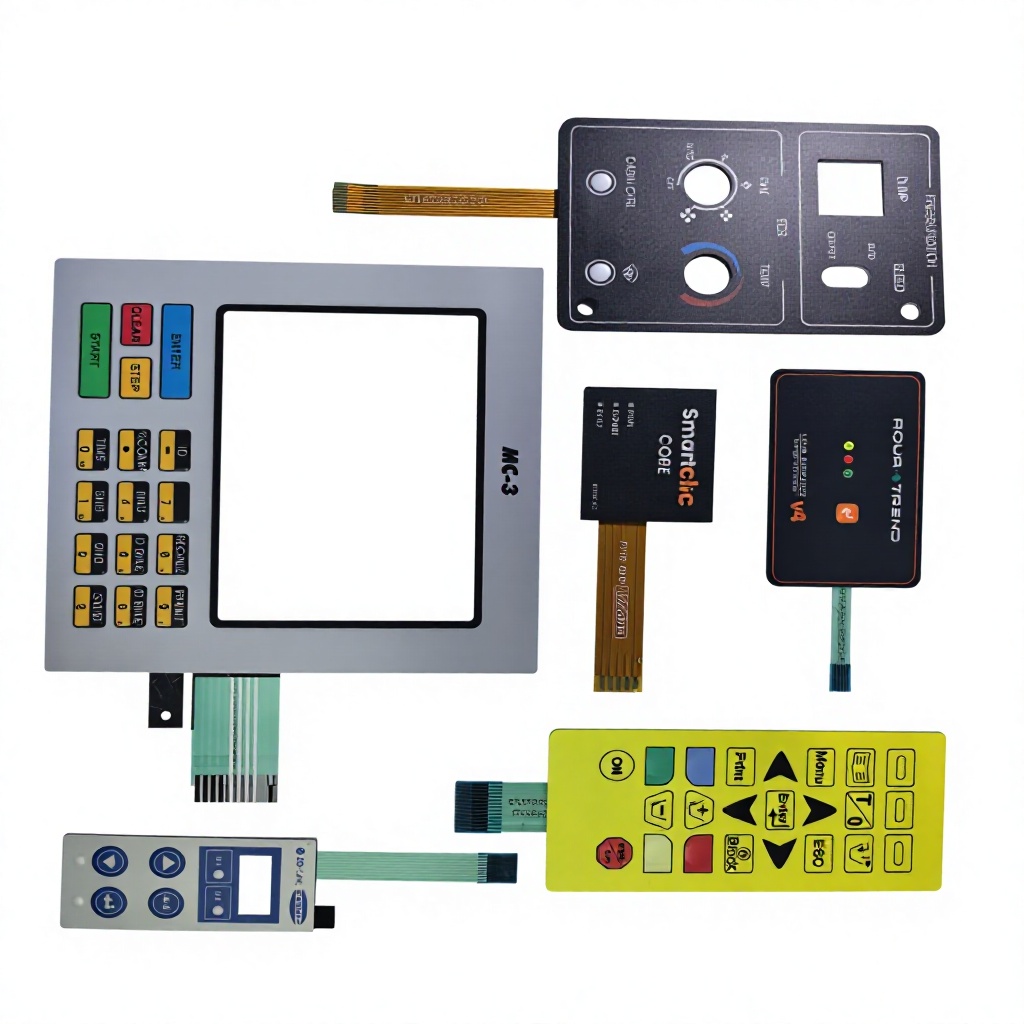
A technical comparison of photon distribution systems tailored for harsh ambient environments, from bright Pacific sunlight to nighttime operation.
Utilizing micro-dot pattern side-emitting refraction via high-optical grade polycarbonate or PMMA film (0.125mm to 0.25mm). Achieves 92% luminance uniformity across 60+ keys using only 4 to 6 low-draw side-firing SMD LEDs. Critical for Auckland battery-powered IoT field units requiring minimal energy dissipation and negligible heat buildup.
Mounting miniature chip LEDs directly onto printed flexible silver circuit tails or polyimide FPC layers. Engineered with specialized dome spacers to eliminate light bleed between discrete functional legends. Enables dynamic dual-color (Red/Green/Amber) status indication for safety interlocks and marine navigational instruments.
Excitation of phosphor crystals encapsulated between conductive indium tin oxide (ITO) layers by AC high-frequency fields. Delivers balanced, ultra-thin (0.1mm) cool illumination. Ideal for night-vision goggle (NVG) compatible avionic systems and low-noise specialized biomedical displays engineered in New Zealand research facilities.
| Parametric Attribute | Silver Conductive Polyester Print | Polyimide Flexible Copper (FPC) | Rigid Backed FR4 Hybrid |
|---|---|---|---|
| Loop Resistance | < 100 Ω (Circuit trace length dependent) | < 2 Ω (Ultra-low dissipation) | < 0.5 Ω (True printed circuit integrity) |
| Operating Temperature | -20°C to +70°C (Industrial Grade) | -40°C to +105°C (Extreme Environment) | -40°C to +125°C (Automotive / Military) |
| Tactile Actuation Force | 180g to 450g (Configurable Stainless Domes) | 220g to 500g (Precision Crisp Snap) | Customized snap tactile force curve |
| Ingress Rating Capability | IP65 (Perimeter Gasket Adhesion) | IP67 / IP68 (Waterproof Perimeter Seal) | IP67 / NEMA 4X (O-Ring Groove Capable) |
| Expected Key Life | > 1,000,000 actuations | > 5,000,000 actuations | > 3,000,000 actuations |
Auckland represents New Zealand's commercial and advanced manufacturing epicenter. Our backlit keypads are purpose-built to solve environmental and operational challenges across key regional hubs.
Auckland’s world-renowned boat building and marine electronics sectors in Westhaven and Albany require keypads immune to salt spray crystallization, high UV indexes, and nighttime visibility demands. We engineer IP68 silicone-sealed backlit switches with xenon-tested UV barriers.
Dairy sheds, automated sorting hubs, and meat processing facilities throughout South Auckland enforce aggressive caustic CIP (Clean-in-Place) washdowns. Our chemically inert Autotex PET overlays withstand sodium hydroxide, nitric acid, and high-pressure hot water sanitization.
Heavy machinery, bottling equipment, and PLC cabinets situated across Auckland's industrial belt operate through continuous mechanical vibrations. We deploy gold-plated metal domes with redundant contact rings to ensure zero contact bounce and continuous uptime.
Precision health equipment manufactured in Auckland’s biomedical corridors requires non-porous, antimicrobial HMI surfaces compatible with alcohol, chlorhexidine, and ethylene oxide sterilization, coupled with soft LGF backlighting for dark operating environments.
Understanding shifting regulatory compliance, environmental durability, and technological convergence across the ANZ market.
Auckland OEMs are increasingly migrating away from purely resistive touchscreens toward hybrid architectures. Capacitive touch slider zones paired with tactile metal dome stop/start switches eliminate false actuations caused by rain droplets in outdoor marine and agricultural settings.
Due to the Southern Hemisphere ozone gap, UV radiation in New Zealand degrades conventional PVC overlays within 12–18 months. Leading hardware teams now mandate outdoor-rated Autotex XE and 3M 200MP series acrylic adhesives tested over 2,000 continuous hours in xenon aging chambers.
New Zealand's agile hardware startup ecosystem requires iterative prototype turnarounds without commercial lock-in. Direct-from-factory digital UV printing allows cost-effective production of 50 to 500 units without custom screen-stencil setup expenses.
Combining over 30 years of human-machine interface engineering with German technical collaboration and certified vertically integrated facilities.
In-house precision steel mold fabrication ensuring tight ±0.05mm perimeter tolerances on custom embossing dies.
Eliminating edge burrs, stress cracks, and expensive knife-tooling charges on complex tail ribbon and window profiles.
From CAD design, screen coating, UV digital printing to FPC bonding and xenon test aging, zero sub-tier outsourcing.
Full traceable lifecycle documentation with computerized continuity test verifications delivered with every shipment.
Clear, direct technical answers covering delivery lead times, logistics clearance into Auckland Ports, and design-for-manufacture requirements.
Express courier air freight (DHL/FedEx/TNT) directly into Auckland International Airport (AKL) delivers in 3 to 5 business days following dispatch. For consolidated volume orders, direct sea freight from Shenzhen or Tianjin Port to Ports of Auckland (POAL) averages 14 to 18 sailing days, accompanied by complete HS code documentation (8537.10) for seamless New Zealand Customs clearance.
We apply continuous perimeter die-cut gaskets utilizing genuine 3M 467MP, 468MP, or 3M 300LSE low-surface-energy adhesive systems. Furthermore, internal air venting channels are engineered to route through the connector tail ribbon into the enclosed interior chassis, preventing pressure differentials while eliminating exterior atmospheric moisture intake.
Our 10-person CAD engineering department converts artwork supplied in Adobe Illustrator (.AI), vector PDF, CorelDRAW (.CDR), AutoCAD (.DXF/.DWG), or Gerber circuit files. If you only possess a physical sample or legacy panel from an existing Auckland production unit, our reverse-engineering team can digitize graphic layers, track traces, and produce complete production approval drawings within 48 hours.
We deploy high-density opaque black light-blocking isolation barriers silk-screened between the graphic overlay and the circuit diffuser layers. For light guide film (LGF) builds, laser micro-cavities reflect light strictly into designated key legends, ensuring zero peripheral bleed onto neighboring buttons or transparent display windows.
Yes. We integrate AL6061/5052 anodized aluminum backer plates, stainless steel sheets, or FR4 PCB rigidizers complete with press-fit PEM studs, clinch nuts, and countersunk mounting holes. This provides Auckland electrical assemblers with a plug-and-play drop-in module that seals instantly into enclosure bezels without secondary fastening steps.
Unlike conventional contract factories demanding thousands of units, our digital UV printing and automated laser profile cutters eliminate high initial tooling costs. We support engineering prototype batches as low as 10 to 50 pieces for pilot validation runs across Auckland research institutions and hardware incubators.
Partner directly with a certified, vertically integrated Chinese manufacturer serving Auckland’s industrial, agritech, and marine technology pioneers. Request an instant engineering review, stack-up recommendation, or factory quote.
Send an Inquiry