High-Reliability Metal Dome Keypads & Membrane Assemblies
Engineered for mission-critical tactile feedback, environmental durability, and rapid prototyping integration. Select a product build below to inspect full electrical, mechanical, and finishing specifications.
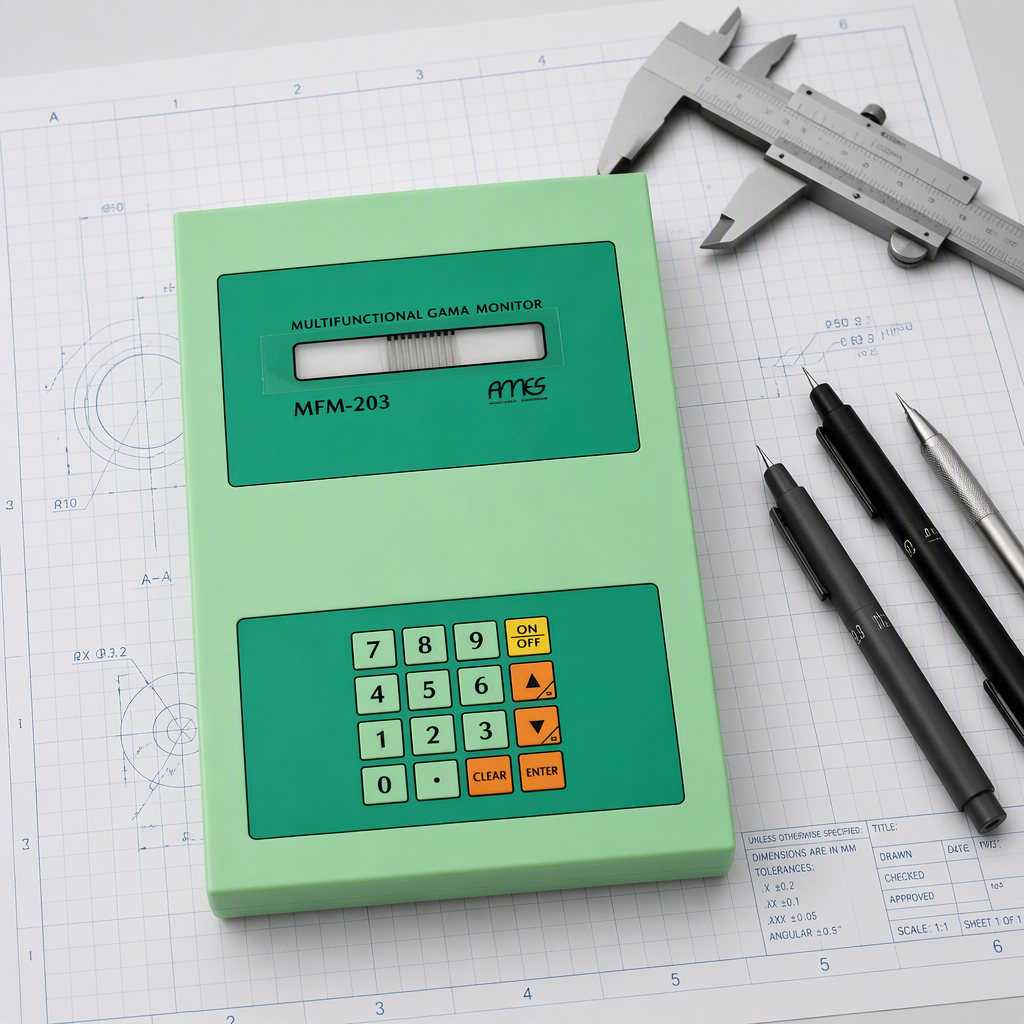
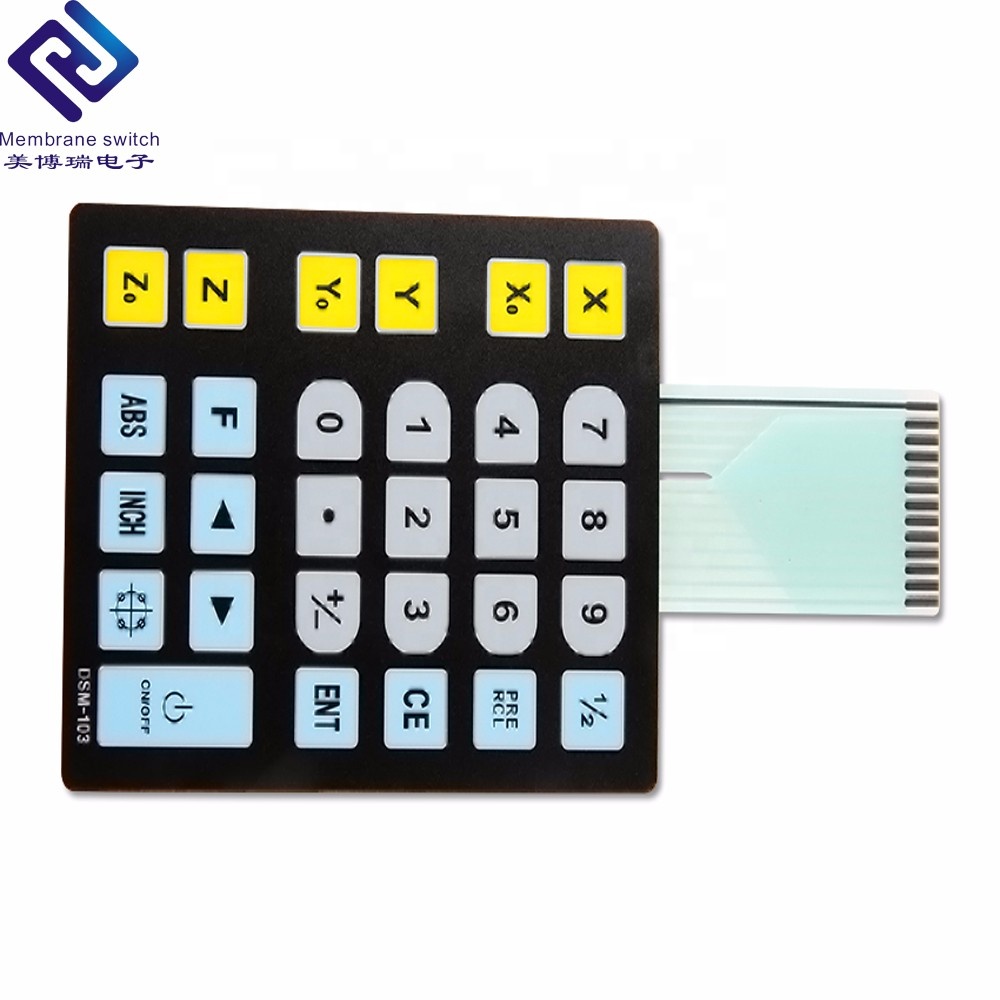
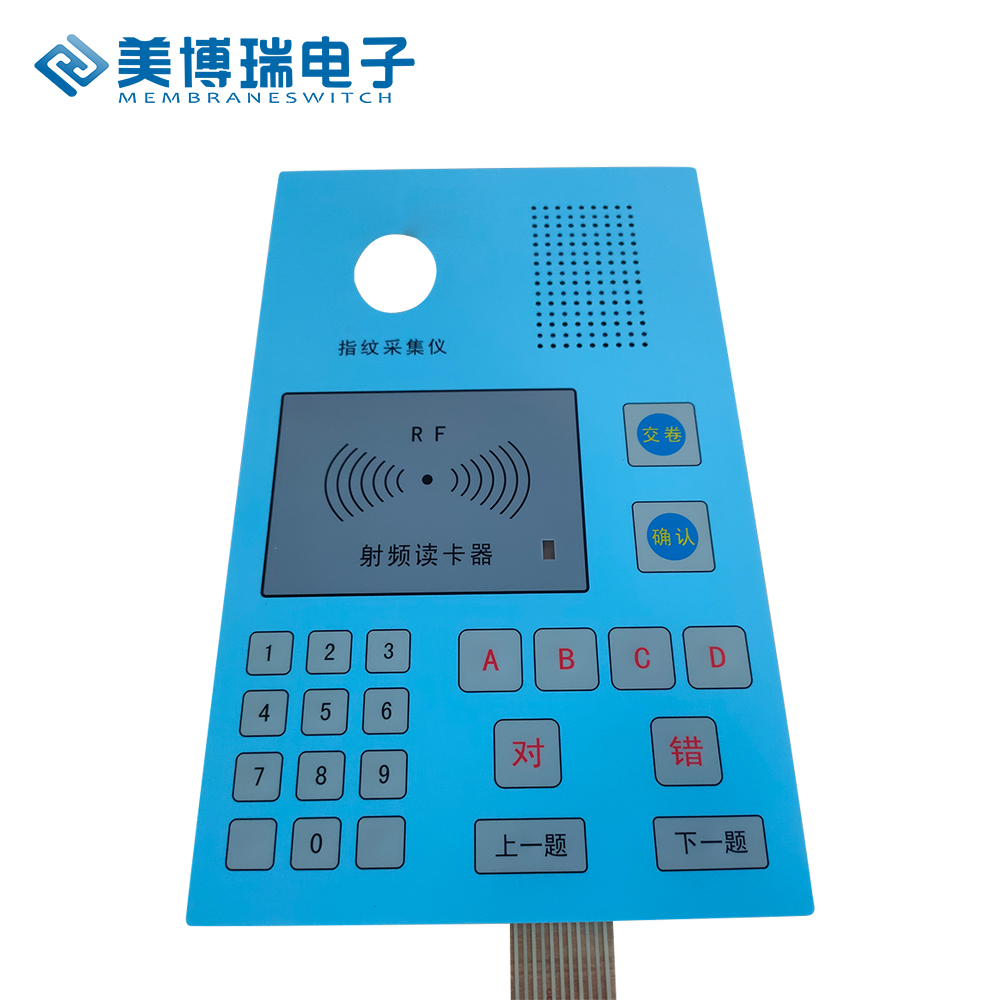
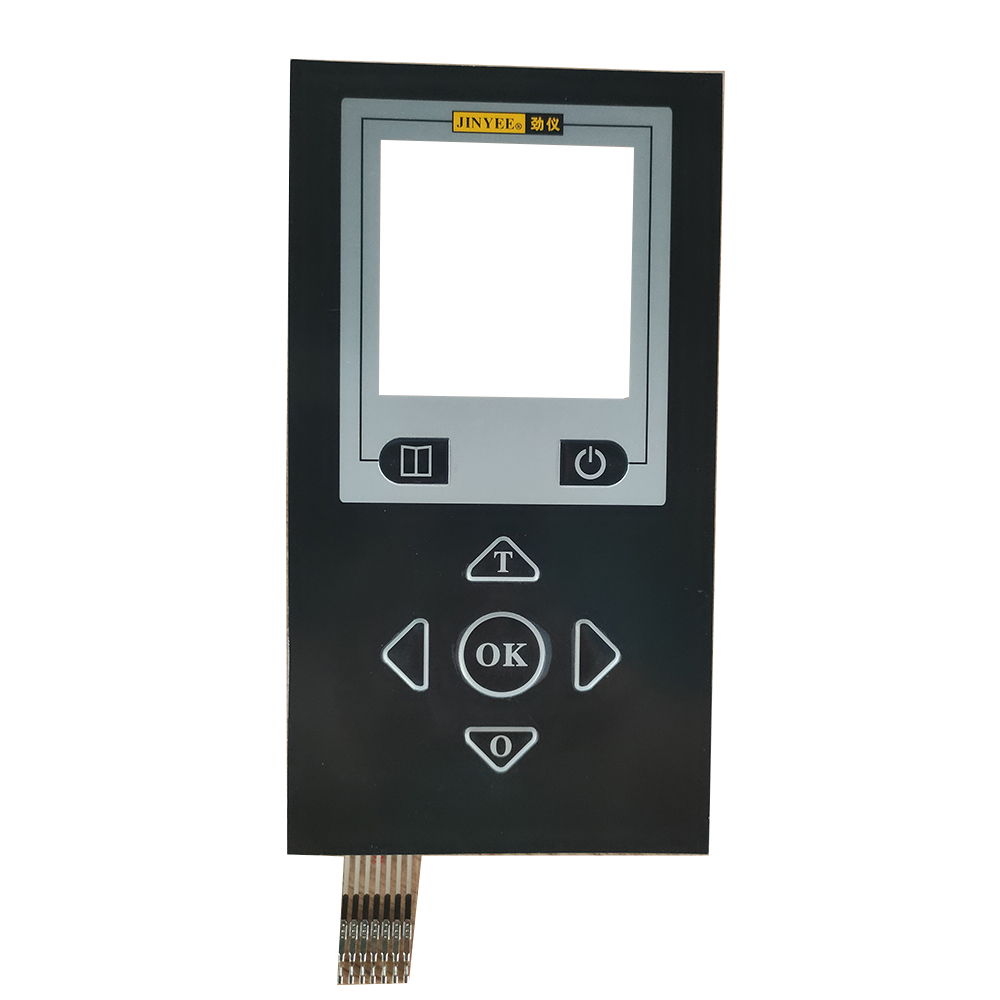
Tactile Physics & Mechanical Snap Dynamics
Within human-machine interface (HMI) engineering, the tactile snap sensation is governed by the snap ratio formula: Snap Ratio = (F1 - F2) / F1, where F1 represents peak actuation force (trip force) and F2 represents return contact force. High-spec industrial metal dome keypads demand snap ratios calibrated between 40% and 60% to guarantee definitive, non-fatiguing feedback to operators wearing heavy safety gloves in demanding Merseyside maritime docks, offshore platforms, or chemical plants.
Our stainless steel metal domes (SUS301 and SUS304 temper grades) are precision-stamped with four-leg, round, or oblong triangle geometries. Available in diameters ranging from 6mm to 20mm, with actuation forces tailored from 200g up to 500g, these components deliver exceptionally stable snap curves. Our dual-contact engineering ensures contact bounce times remain below 5ms, mitigating false triggering in fast-cycling microcontroller (MCU) polling circuits.
To eliminate silver migration and corrosion caused by atmospheric chlorides along the River Mersey, our circuit layers feature optional selective gold or nickel plating at contact pads, backed by laser-cut acrylic spacer channels that equalize pneumatic pressure during dome deflection without compromising hermetic perimeter seals.
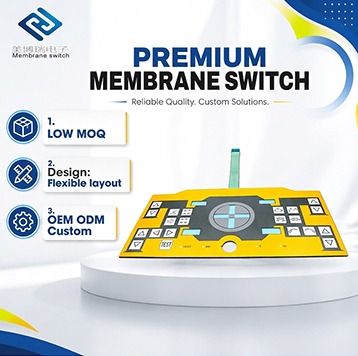
Sub-Millimeter Layer Stack-Up Architecture
A precision-manufactured metal dome keypad functions as a multi-tier laminated mechanical switch. Every micron of layer thickness influences tactile feel, actuation travel, and ingress protection against caustic washdowns or marine salt fog:
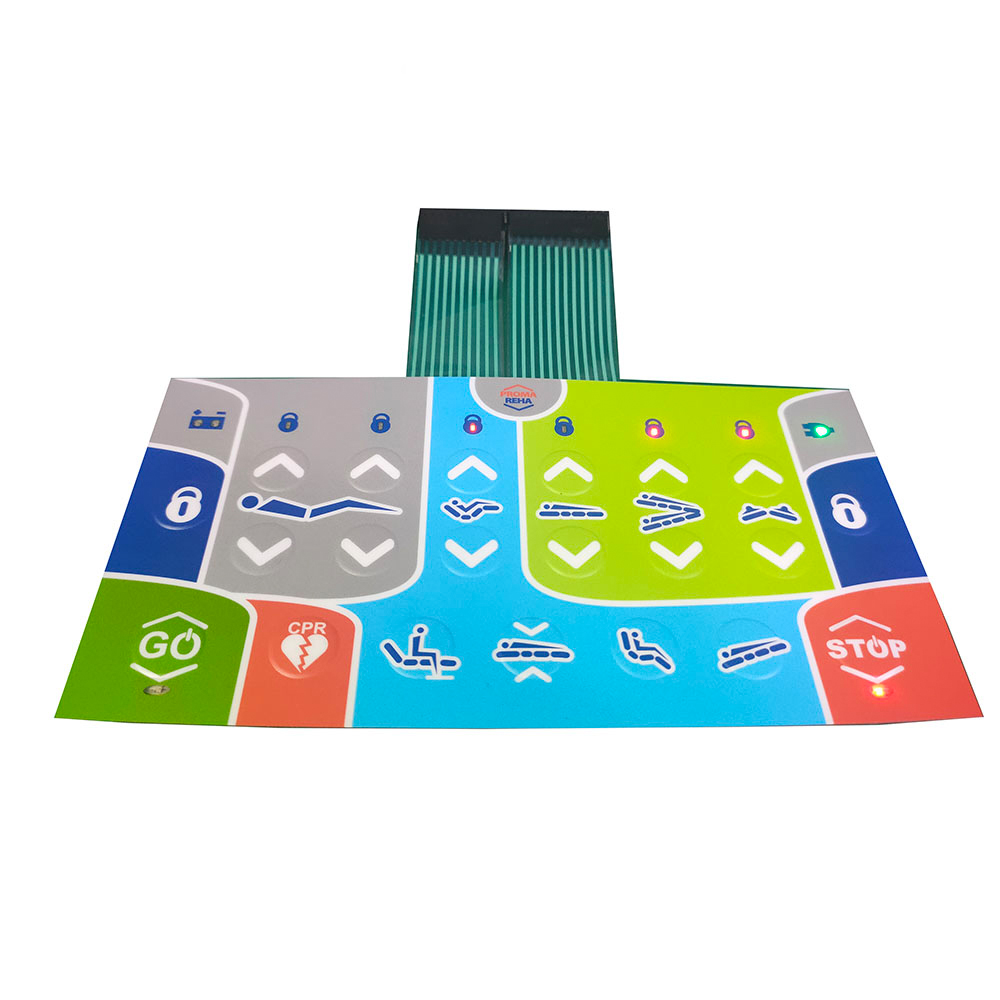
- L1: Graphic Overlay: 0.15mm – 0.20mm Autotex XE or Makrofol polycarbonate, reverse printed via 37 silkscreen or Mimaki digital UV lines with selective micro-embossing (rim, pillow, or dome).
- L2: Overlay Adhesive: High-performance 3M 467MP or 468MP acrylic adhesive transfer tape engineered to resist shear stress under cyclic thermal oscillation.
- L3: Dome Retainer / Spacer Layer: Laser-die-cut polyester sheet containing pneumatic venting channels and precise pocket apertures that lock metal domes securely over target circuits.
- L4: Actuation Domes: Nickel-plated or gold-plated SUS301 stainless steel domes configured for tactile travel from 0.3mm to 0.6mm.
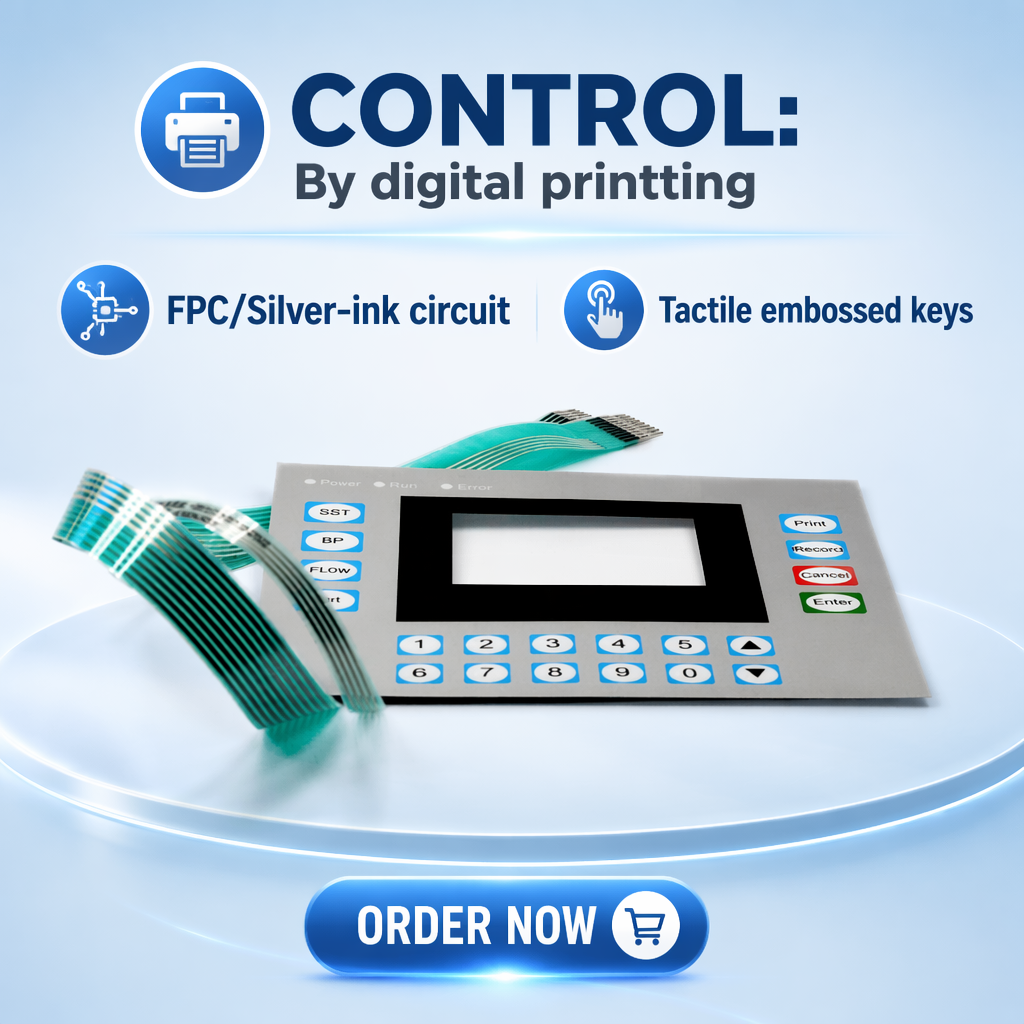
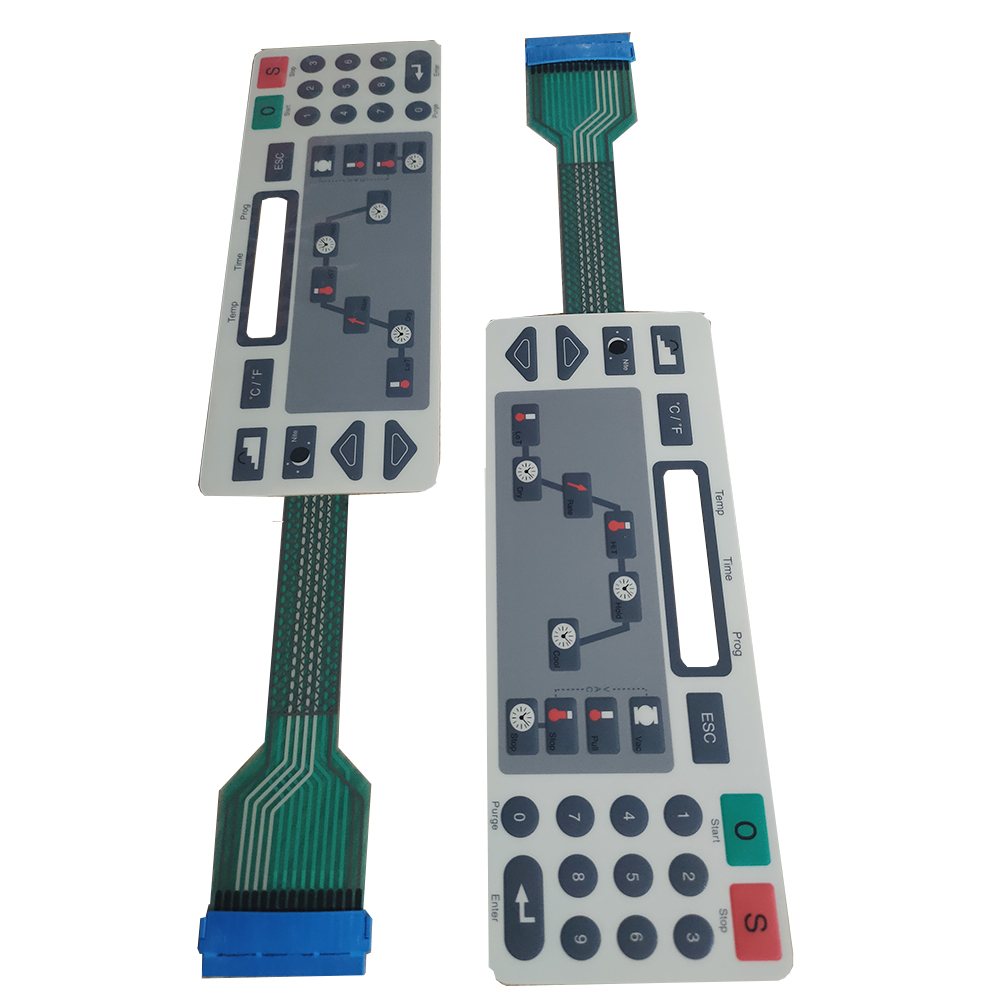
- L5: Conductive Circuit: Screen-printed conductive silver polymer ink with dielectric crossover bridges, or flexible etched copper Polyimide (FPC) for high trace density.
- L6: Base Mounting Adhesive: 3M 200MP or 300LSE adhesive rated for secure adhesion to powder-coated cast aluminium, stainless steel, or low-surface-energy ABS/polypropylene enclosures.
This coordinated stack-up guarantees consistent mechanical performance across more than 1,000,000 operational cycles while maintaining compliance with RoHS, REACH, and UKCA industrial directives.
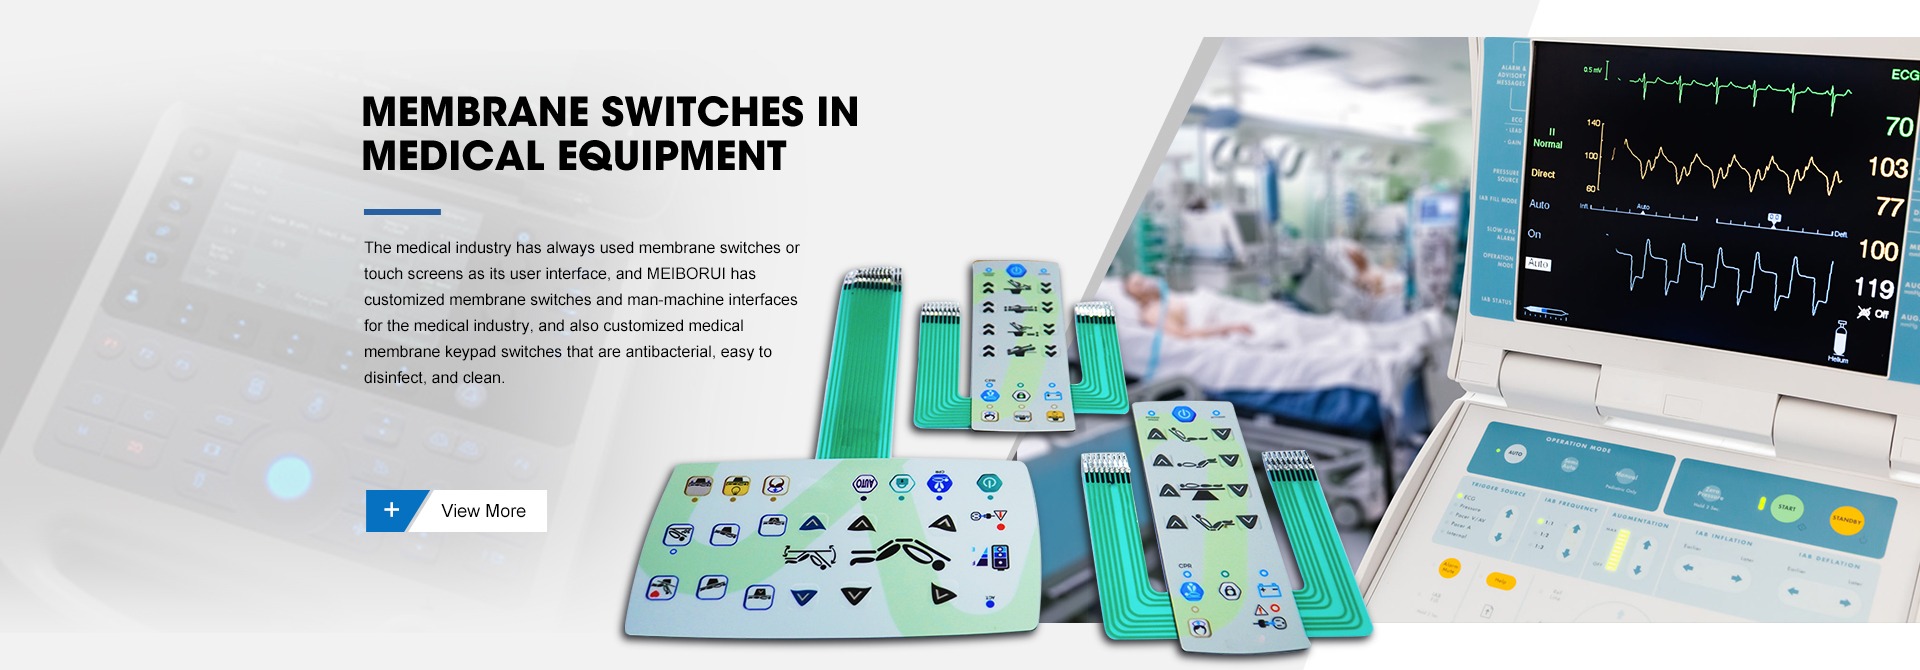
Mission-Critical Deployments Across Liverpool Industrial Corridors
From the Port of Liverpool and the Mersey Estuary to advanced manufacturing clusters in Knowsley, Speke, and Runcorn, our metal dome switch assemblies deliver dependable human-machine interface performance in harsh environments.
Maritime Navigation & Port Automation
Liverpool’s extensive maritime logistics infrastructure at Seaforth Docks and along the Irish Sea relies on crane consoles, winch controls, radar consoles, and container tracking terminals exposed to continuous marine brine.
- IP67/IP68 perimeter gas-tight gaskets preventing salt spray ingress.
- SUS304 gold-plated dome options resistant to electrolytic oxidation.
- Autotex XE UV-resistant overlays preventing yellowing and micro-cracking under direct marine exposure.
Chemical & Petrochemical Processing
Merseyside and Cheshire chemical hubs (Runcorn, Widnes, Ellesmere Port) handle aggressive reagents, solvents, and frequent high-pressure washdowns requiring chemically inert front panels.
- Textured polyester films resistant to ketones, alcohols, and caustic cleaning fluids.
- Seamless, flat graphic overlays preventing biological or particulate accumulation.
- Conductive carbon-coated contact pads for hazardous environment reliability.
Pharmaceutical & Speke Life Sciences
The biomedical and vaccine manufacturing corridor in Speke requires hygienic, sterilizable interfaces that endure repeated IPA (isopropyl alcohol) wipes, hydrogen peroxide vapor, and UV sterilization.
- Antimicrobial film coatings inhibiting bacterial proliferation.
- Optical-grade clear display windows bonded with clear OCA adhesives for zero parallax.
- Tactile crisp metal dome actuation eliminating operator double-stroke errors during formula entry.
Advanced Automotive & Robotic Tooling
Halewood automotive facilities and adjacent Tier-1 manufacturing suppliers demand rugged handheld teach pendants, automated guided vehicle (AGV) panels, and programmable logic controller (PLC) keyboards.
- High actuation trip forces (350g to 500g) preventing accidental triggering.
- Integrated surface-mount bi-color LEDs and embedded light guide film (LGF).
- Aluminium backing plates (1.5mm to 3.0mm) with PEM studs for rigid enclosure mounting.
Offshore Wind & Renewable Energy Hardware
Operations managing Burbo Bank and Irish Sea offshore wind assets demand power conversion and subsea monitoring interfaces capable of flawless operation under extreme thermal variations.
- Operational temperature range rating: -40°C to +85°C.
- EMI/RFI aluminum shielding foil layers exceeding 60 dB attenuation.
- Hermetically encapsulated dome chambers preventing internal condensation during thermal cycling.
UK North West HMI Sourcing Trends: Direct OEM Engineering Partnerships
Electronics and mechanical engineering procurement teams across Liverpool and Greater Manchester are increasingly transitioning away from multi-tier brokerage distributors in favor of direct manufacturer-to-OEM collaboration. With strict supply chain auditing requirements and tight production release windows, hardware innovators require direct access to manufacturing tooling engineers who can provide DFM (Design for Manufacturability) analysis within 24 hours.
Key drivers transforming the Liverpool procurement landscape include:
- Compression of NPI Timelines: New Product Introduction (NPI) cycles for Merseyside automation startups and medical device developers now demand prototype sample delivery within 7 to 10 days, eliminating the traditional 6-week tooling delays.
- Direct Engineering Collaboration: Direct communication between UK CAD designers and factory CAM/screen-tooling specialists eliminates translation discrepancies on critical tolerances (e.g., dome alignment within ±0.1mm, connector tail pitch at 1.0mm/2.54mm).
- Tariff & Compliance Transparency: Sourcing managers require full documentation packages including certificates of conformity (CoC), RoHS, REACH declarations, and UKCA compliance data to support domestic and European market distribution.
By leveraging our dual-production infrastructure, Liverpool clients secure direct tier-1 factory pricing alongside rapid air-freight logistics directly into Manchester or Liverpool John Lennon Airports.
Comprehensive HMI Substrate & Dome Material Matrix
Selecting appropriate materials is critical to ensure mechanical longevity, chemical immunity, and electrical integrity under rigorous operational environments.
| Component Layer | Material Options | Key Technical Properties | Operating Temp Range | Recommended Industrial Application |
|---|---|---|---|---|
| Graphic Overlay Substrate | Autotex XE Polyester (PET) / Makrofol Polycarbonate (PC) | Abrasion resistance, flexural fatigue life >5M actuations, optical clarity, chemical inertness | -40°C to +85°C (PET) -30°C to +105°C (PC) |
Outdoor maritime consoles, chemical washdown interfaces, industrial automation |
| Tactile Metal Domes | SUS301 / SUS304 Stainless Steel (Nickel or Gold Plated) | Snap ratio 40%–60%, trip force 200g–500g, contact resistance <50 mΩ, bounce <5ms | -40°C to +125°C | Medical instruments, teach pendants, marine navigation keyboards |
| Circuit Conductor | Screen-Printed Conductive Silver / Etched Polyimide FPC | Sheet resistance <15 mΩ/sq/mil (Silver) or ultra-low resistance copper traces (FPC) | -20°C to +70°C (Silver) -40°C to +105°C (FPC) |
Silver for standard cost-effective HMI; FPC for dense SMT LEDs and vibration-heavy machinery |
| Adhesive Lamination | 3M 467MP / 3M 468MP / 3M 300LSE | Shear strength up to 100 psi, resistant to humidity, solvent splashes, and plasticizer migration | -40°C to +150°C | Enclosure sealing against smooth aluminium, painted sheet metal, or low-energy plastics |
| Rigid Backer Plate | AL5052 Anodized Aluminium / FR4 Glass Epoxy PCB | Structural rigidity, integrated PEM studs, ground plane shielding, direct component soldering | -50°C to +130°C | Heavy plant equipment, vehicle telematics, outdoor kiosk panel integration |
Why Liverpool & International OEMs Rely on Our Factories
Combining heritage engineering dating back to 1990 with modern cleanroom production and comprehensive testing infrastructure.
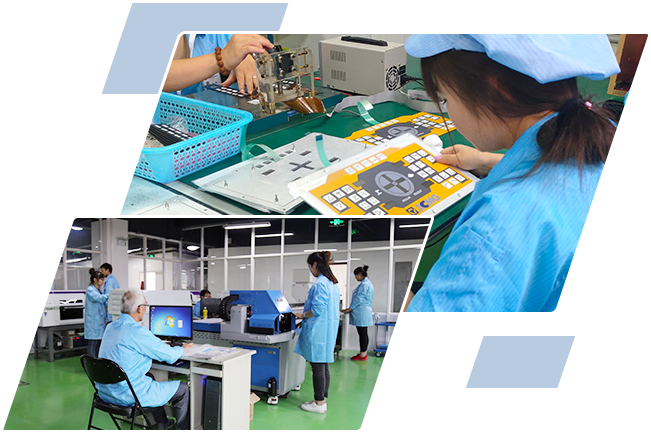
Dual-Facility Scale & Fully Integrated In-House Production
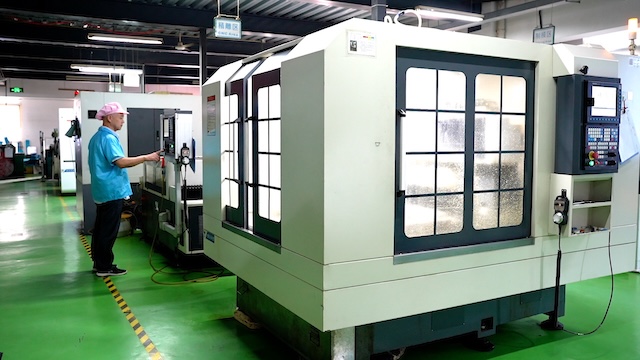
We eliminate quality bottlenecks by housing every production step under a unified quality assurance regime. Rather than outsourcing screen printing, die cutting, or metal backing assembly to third parties, our operations encompass 100% in-house manufacturing across two modern facilities:
- Xianghe Robot Industry Port Base (Langfang): Centralized precision prototyping, CAD/CAM layout design, cleanroom screen printing, and reliability testing.
- Huizhou Base (Guangdong): High-volume automated stamping, SMT pick-and-place component integration, and automated optical inspection (AOI).
- Machinery Fleet: Equipped with 60 CNC mold-making centres, 37 precision silkscreen printers, 4 high-resolution Mimaki digital UV printers, 18 precision laser cutting tables, and 7 high-speed digital engraving units.
This operational architecture guarantees that capacity constraints never compromise customer delivery milestones.
Rigorous On-Site Environmental & Reliability Testing Lab
A keypad installed on a maritime container crane in Seaforth or an ambulance defibrillator in Cheshire cannot fail. Our factory maintains an ISO 9001 certified and Intertek-assessed inspection laboratory to validate every production batch:
- Automated Salt Fog Test Chambers: Continuous ASTM B117 salt spray exposure testing validating IP67 seals and dome anti-corrosion plating for marine use.
- Button Life-Cycle Dynamometers: Pneumatic multi-actuator cycling machines executing 1,000,000+ continuous strikes while logging trip force decay curves.
- Programmable Climate Chambers: Thermal shock and humidity stress profiling cycling rapidly between -40°C and +85°C at 95% relative humidity.
- Computerized Circuit Continuity Testers: Automated pin-to-pin open/short/resistance verification validating conductive traces to sub-milliohm accuracy.
Frequently Asked Questions: Sourcing Keypads in Liverpool
Direct technical answers addressing the critical mechanical, electrical, and supply chain considerations of Merseyside procurement professionals.
How do you safeguard metal dome keypads against corrosion in Liverpool's maritime and dockside environments?
What CAD and graphic files are required to initiate a custom dome keypad project?
- Mechanical Outline Drawing: DXF, DWG, or STEP files depicting external contours, key centers, embossing rims, display cutouts, and tail exit coordinates.
- Graphic Artwork: Vector files in Adobe Illustrator (.AI), CorelDraw (.CDR), or PDF with Pantone Matching System (PMS) color codes clearly designated.
- Schematic / Circuit Diagram: Pin-out schedule, tail pitch (e.g., 2.54mm or 1.0mm ZIF), matrix or common bus configuration, and embedded LED anode/cathode maps.
Can you support low-volume prototype builds for North West tech startups and NPI trials?
How is tactile feedback preserved when operating equipment with thick safety gloves?
What are the lead times and delivery terms for shipments arriving into Liverpool?
Can metal dome keypads integrate backlighting for low-light or night operations?
- Light Guide Film (LGF): Micro-etched optical film that channels light horizontally from side-firing surface-mount LEDs uniformly across key icons and borders while maintaining an ultra-thin sub-1.5mm keypad profile.
- Selective LED Integration: Miniature surface-mounted chip LEDs (0603 or 0805 packages) integrated directly into the circuit layer for clear key status indication.
- Electroluminescent (EL) Lamps: Ideal for balanced, low-power green/blue ambient illumination across maritime bridge displays.
How do you guarantee quality traceability across high-volume production orders?
Accelerate Your Custom HMI Project in Liverpool
Collaborate directly with our senior application engineers to optimize stack-up thickness, snap dynamics, environmental ingress sealing, and production tooling budgets. Request a comprehensive catalog or send your CAD layout for rapid DFM evaluation.
Custom Engineering Support
Direct communication with our technical team. NDA confidentiality guaranteed for all preliminary design schematics.