IP67 Waterproof
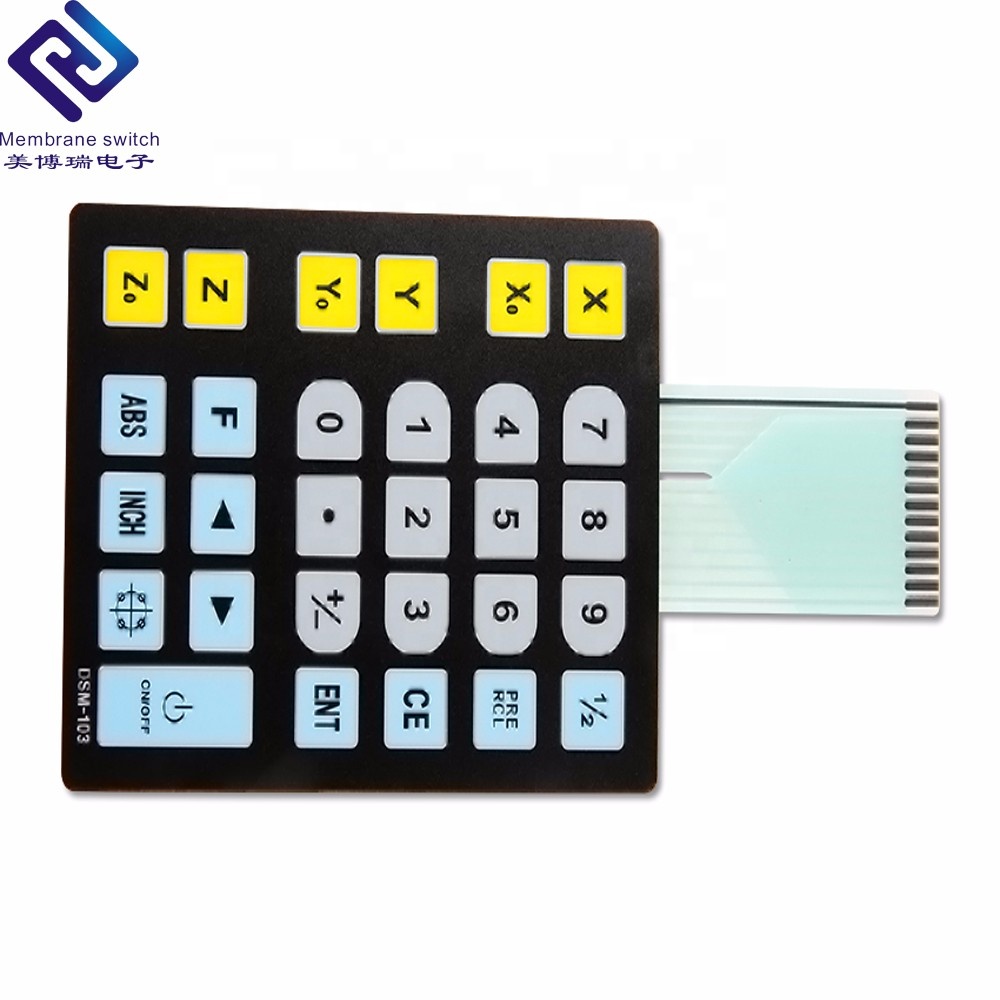
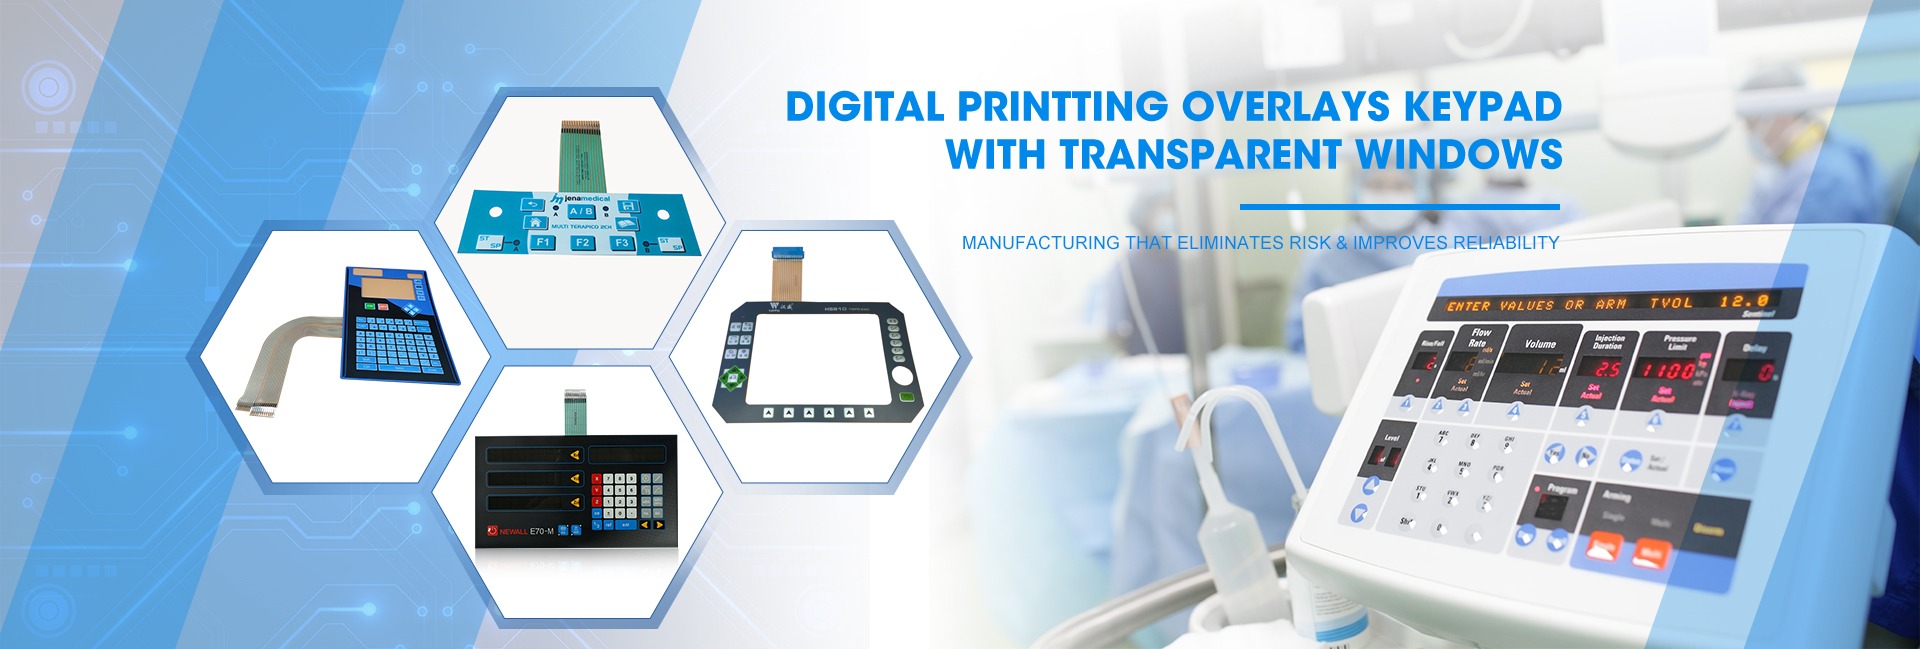
MBR High Quality IP67 Waterproof 3M Adhesive Flexible Cable Membrane Keypad
3M Adhesives
Metal Domes
Sealed PET
Precision-screened circuits, flexible printed interconnects, and uniform illumination options built in compliance with ISO 9001 and verified by Intertek test protocols.
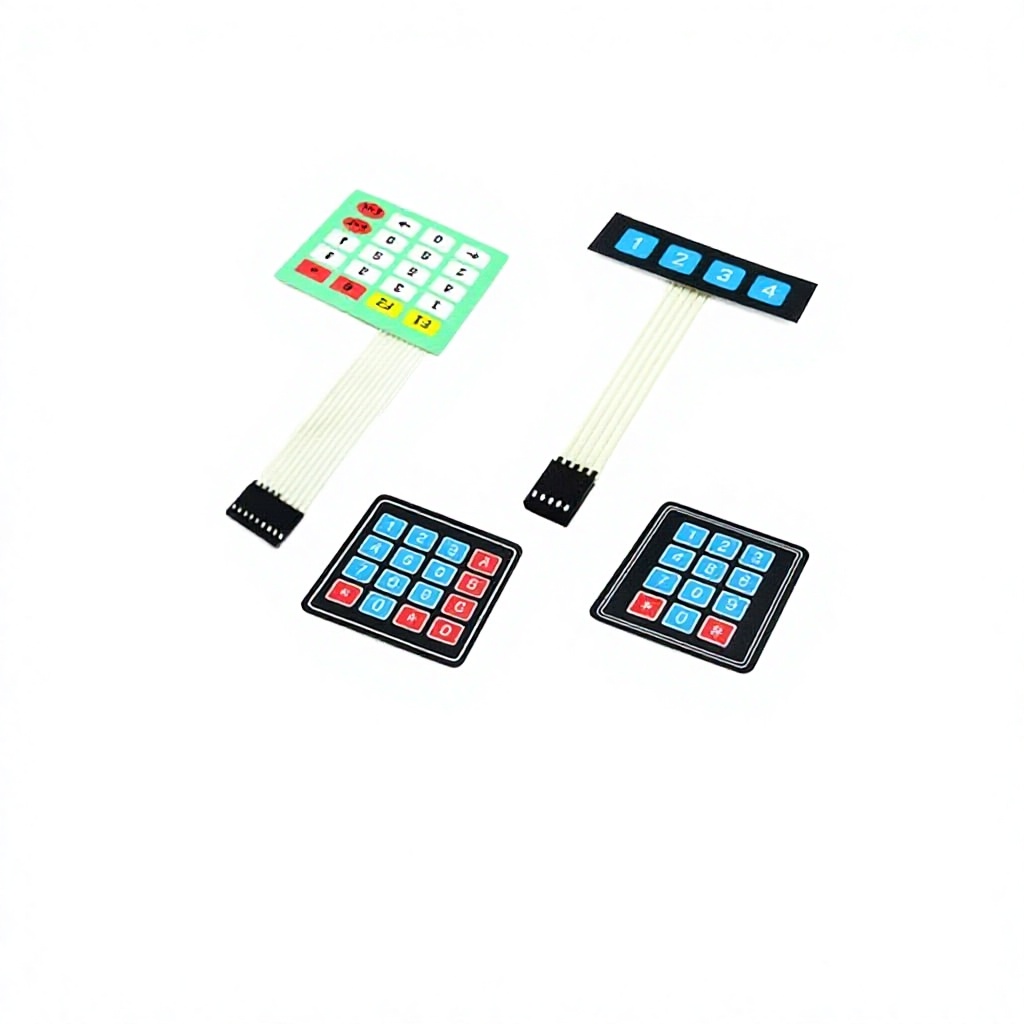
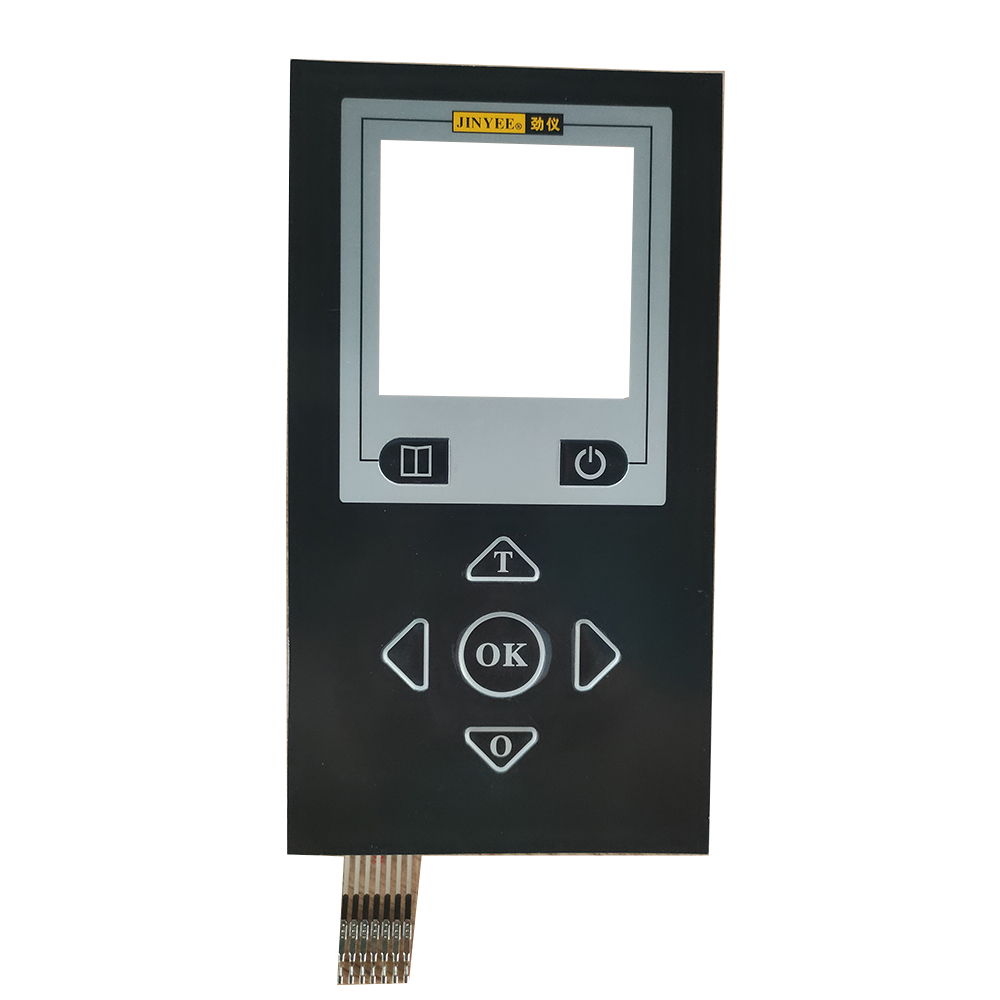
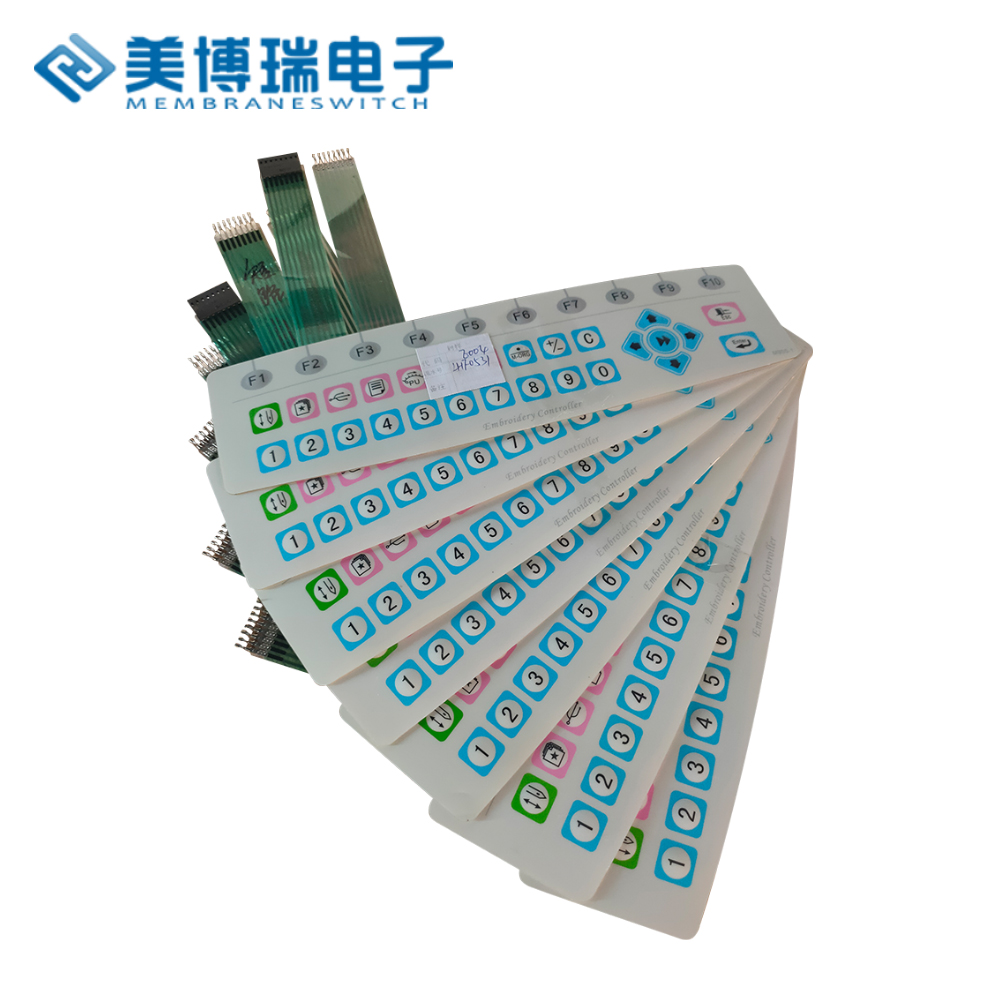
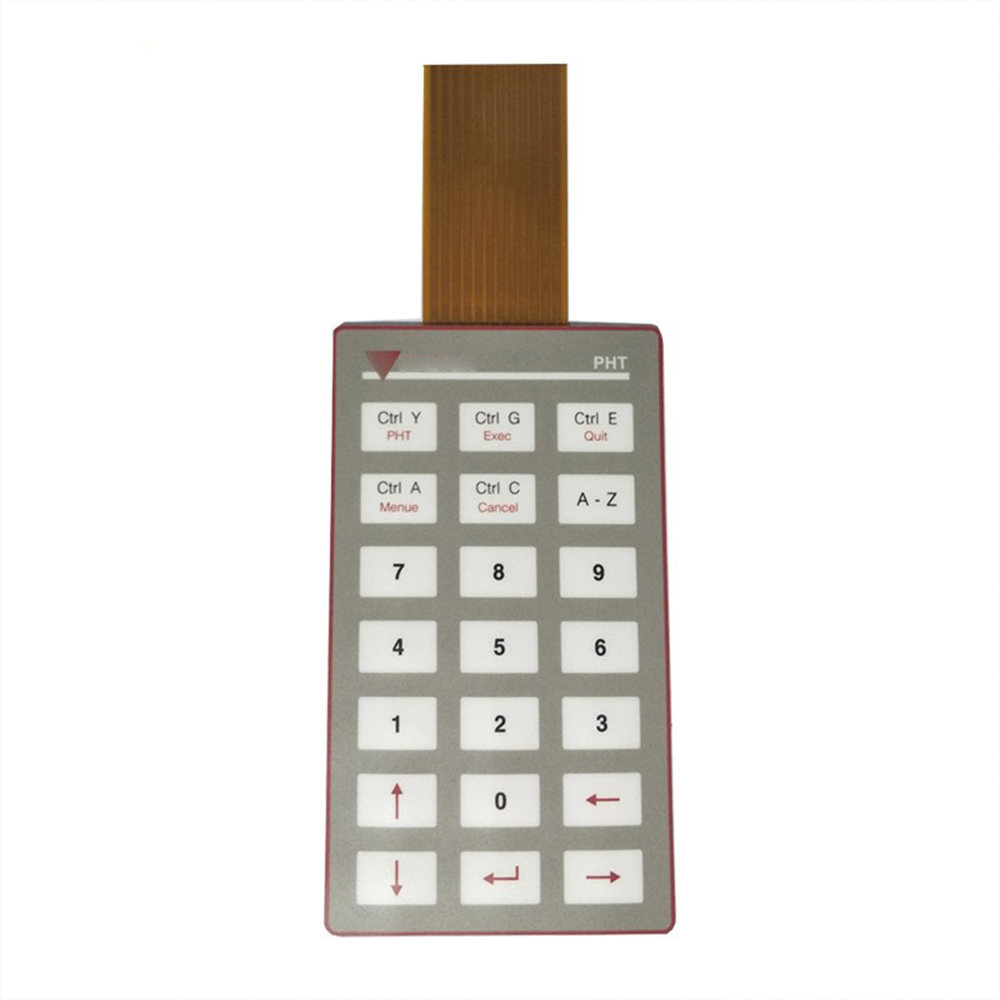
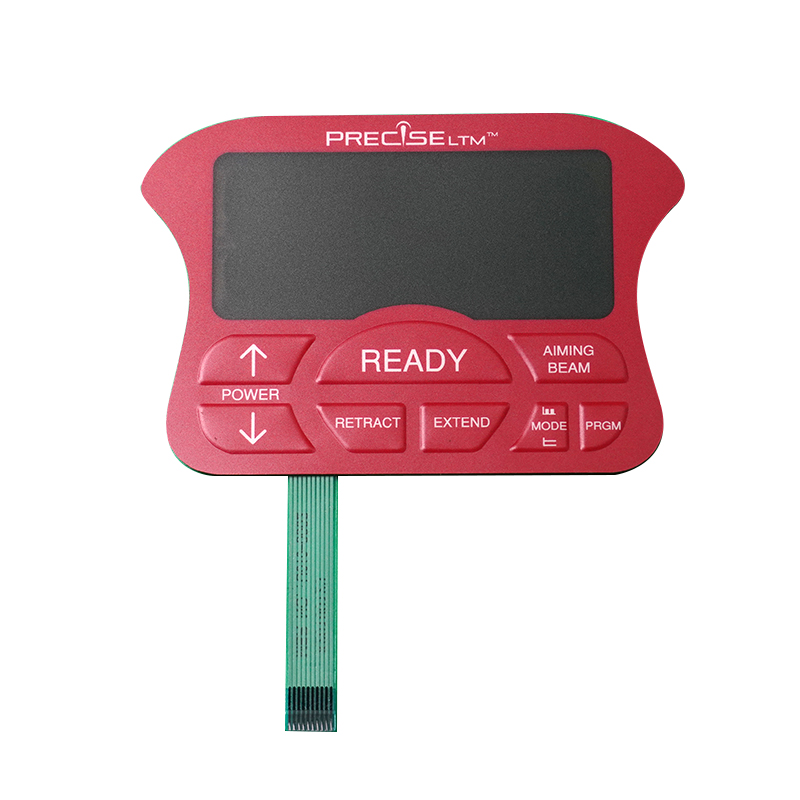
Procuring human-machine interfaces for specialized environments requires balancing ultra-quiet operation, non-invasive aesthetics, electromagnetic compatibility, and decade-long optical stability.
Libraries, scriptoriums, and subterranean vaults safeguarding ancient parchment and priceless artworks require microclimatic precision. Our membrane panels incorporate sealed IP67 perimeter gaskets and continuous backlighting to prevent humidity ingress while enabling discreet monitoring in ambient light-restricted zones.
Tested across -20°C to +70°C, these panels provide steady contact resistance (<100Ω) even in high-humidity subterranean gallery conditions.
Institutional entrances, Swiss Guard tactical command desks, and confidential diplomatic rooms demand silent, tamper-resistant access pads. We deploy stainless steel snap-domes rated for over 1,000,000 actuations integrated with diffused Light Guide Film (LGF) networks.
The uniform LED backlighting eliminates hotspots and glare, providing crisp numeric clarity without leaking conspicuous ambient light during evening ceremonies or security patrols.
Acoustic performance inside historic basilicas is paramount. Traditional mechanical switches produce click echoes that disturb sacred services. TAVO engineers customized low-force tactile domes combined with acoustic-dampening overlay foams.
Coupled with reverse-printed polycarbonate graphic overlays resistant to aggressive alcohol disinfectants, these panels blend seamlessly into bronze, stone, or mahogany architectural mounts.
How rigorous electromagnetic standards, longevity demands, and modern illumination methods shape local industrial sourcing.
Historically, membrane switches relied on embedded surface-mount LEDs mounted directly beneath translucent key windows. This legacy technique frequently created visual hot-spots, uneven coloration, and noticeable thermal build-up inside compact wall enclosures.
In high-profile architectural conservation settings, the demand has pivoted to Light Guide Film (LGF) and side-firing micro-LED architectures. LGF redistributes light across microscopic optical micro-dots, yielding razor-sharp, whisper-thin (0.125mm) illumination across intricate multi-lingual lettering, latin glyphs, or status icons with zero bleeding.
Furthermore, stringent electromagnetic immunity demands (CE, RoHS, and low radio emissions) have prompted procurement officers to specify Full-coverage Aluminum or Copper EMI Shielding layers. These grounded conductive grids safeguard telecommunications terminals from external RF interference generated by emergency radio transmissions or high-voltage power networks.
Decades of membrane technology heritage fused with German technical cooperation and dual-factory redundancy.
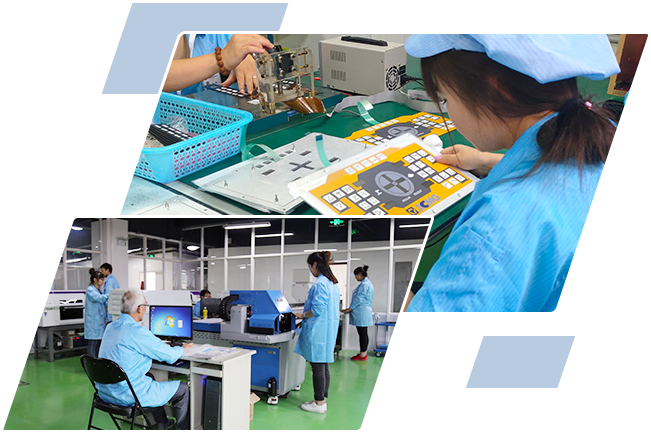
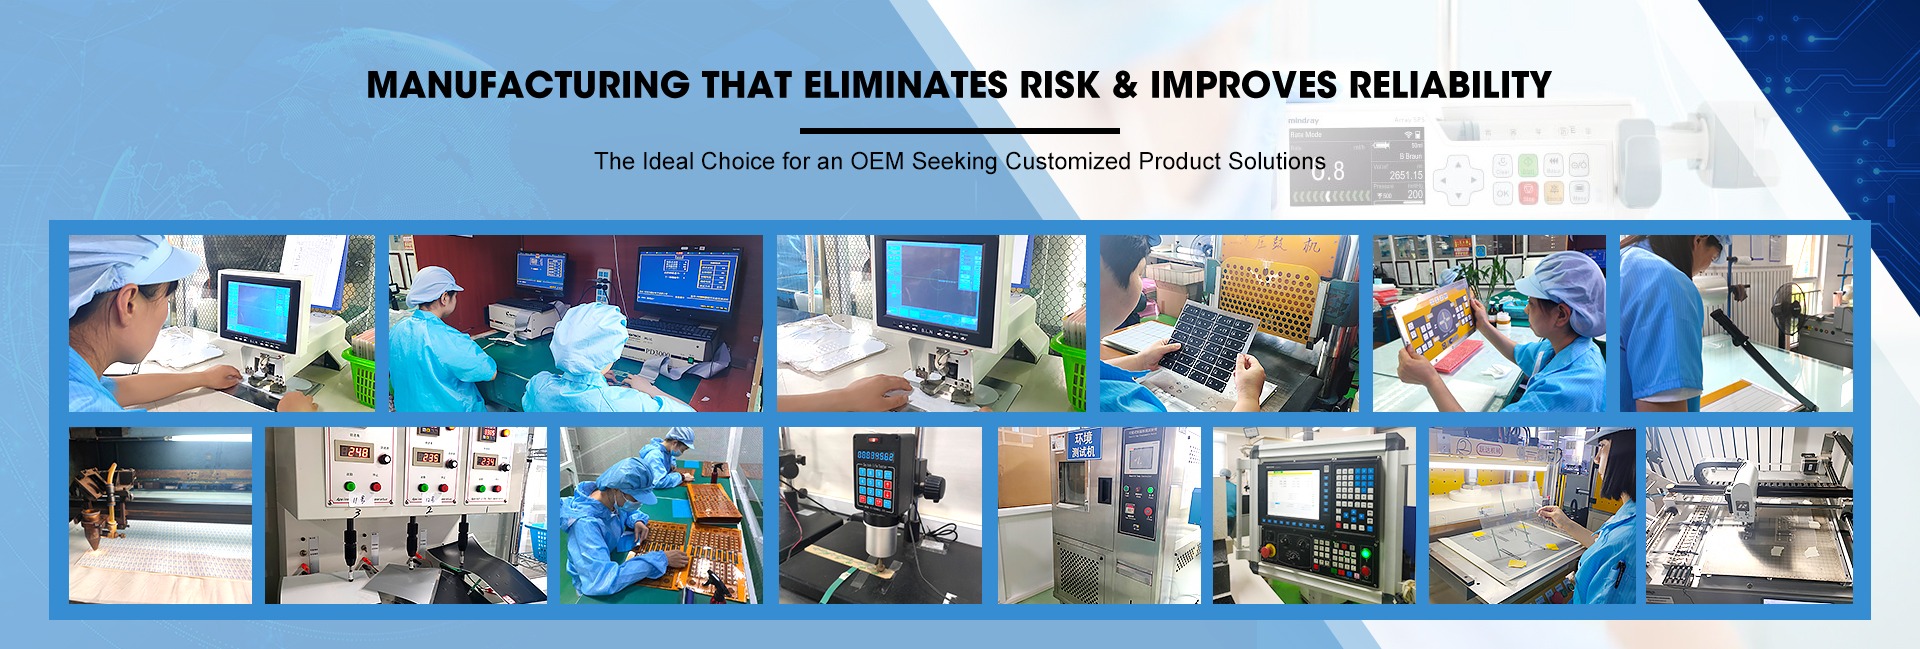
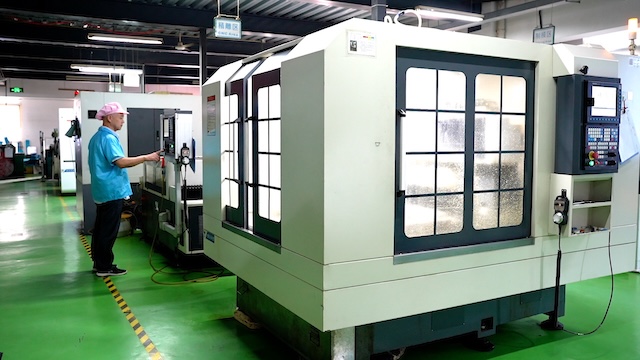
TAVO Electronic Information Technology Co., Ltd. eliminates subcontractor variance. Every production phase—structural design, film patterning, screen printing, embossing, laser profile contouring, cleanroom dome placement, and environmental testing—occurs under direct proprietary supervision across our Langfang (Hebei) and Huizhou (Guangdong) plants.
Through our long-term technical cooperation with a renowned German membrane switch factory, our engineers follow rigorous DIN-aligned mechanical tolerances, guaranteeing dome tactile feedback uniformity within ±15 grams and strict color adherence matching Pantone and RAL specifications.
Clear, direct answers regarding custom tooling, longevity validations, material compliance, and international shipping.
We deploy high-refractive index Light Guide Films (LGF) or custom fiber-optic diffusion grids combined with calibrated side-firing SMD LEDs. By mathematically optimizing the micro-dot scattering patterns across the overlay surface, we maintain a uniform luminance gradient across all tactile keys without localized hotspots or optical edge bleed.
Yes. For sanitary, medical, or high-touch institutional applications, we utilize textured Autotex® polyester or hard-coated polycarbonate graphic overlays. These films demonstrate superior chemical inertness against concentrated alcohol, quaternary ammonium disinfectants, and harsh industrial surface cleaners without clouding or surface degradation.
Thanks to our in-house Mimaki digital UV printing systems and 18 optical laser profile cutters, we can deliver functional, non-tooled membrane switch prototypes in 5 to 7 working days. Hard-tooled, steel-rule production runs and custom embossed tactile production samples are conventionally finalized in 12 to 15 working days upon drawing sign-off.
Absolutely. While standard switches utilize flexible 3M high-performance adhesive layers (such as 3M 467MP or 3M 300LSE), we frequently laminate membrane switches directly to CNC-machined aluminum plates, stainless steel chassis brackets, or rigid FR4 copper PCBs complete with pre-soldered active components, studs, and connectors.
Every shipment is covered by our ISO 9001 inspection dossier, including automated 100% circuit continuity test logs, actuation force curves, dielectric breakdown certificates, and dimensional compliance reports. Full RoHS and REACH declarations of conformity are provided for all integrated plastics, silver paste inks, and adhesive systems.
We provide full EXW, FOB, CFR, and DDP shipping capabilities utilizing premier air express carriers (DHL, FedEx, UPS) and regulated customs couriers. Our trade documentation team ensures seamless customs clearance directly to procurement destinations throughout central Italy and Vatican administrative offices without logistical delay.