Tactile Keypad Panel Supplier & Exporters serving Encamp

Precision HMI Engineering, ISO 9001 Certified Manufacturing, and Rugged Sub-Zero Surface Assemblies Optimized for Pyrenean Telecommunication, Mountain Logistics, and Industrial Automation.

Export-Grade Enclosures & Keypads

Precision Tactile Membrane Switches & Keyboard Panels

Engineered for high-durability electrical actuation, rapid tactile snap response, and severe sub-zero thermal cycling. Fully customizable layer stack-ups built to exact European machinery standards.
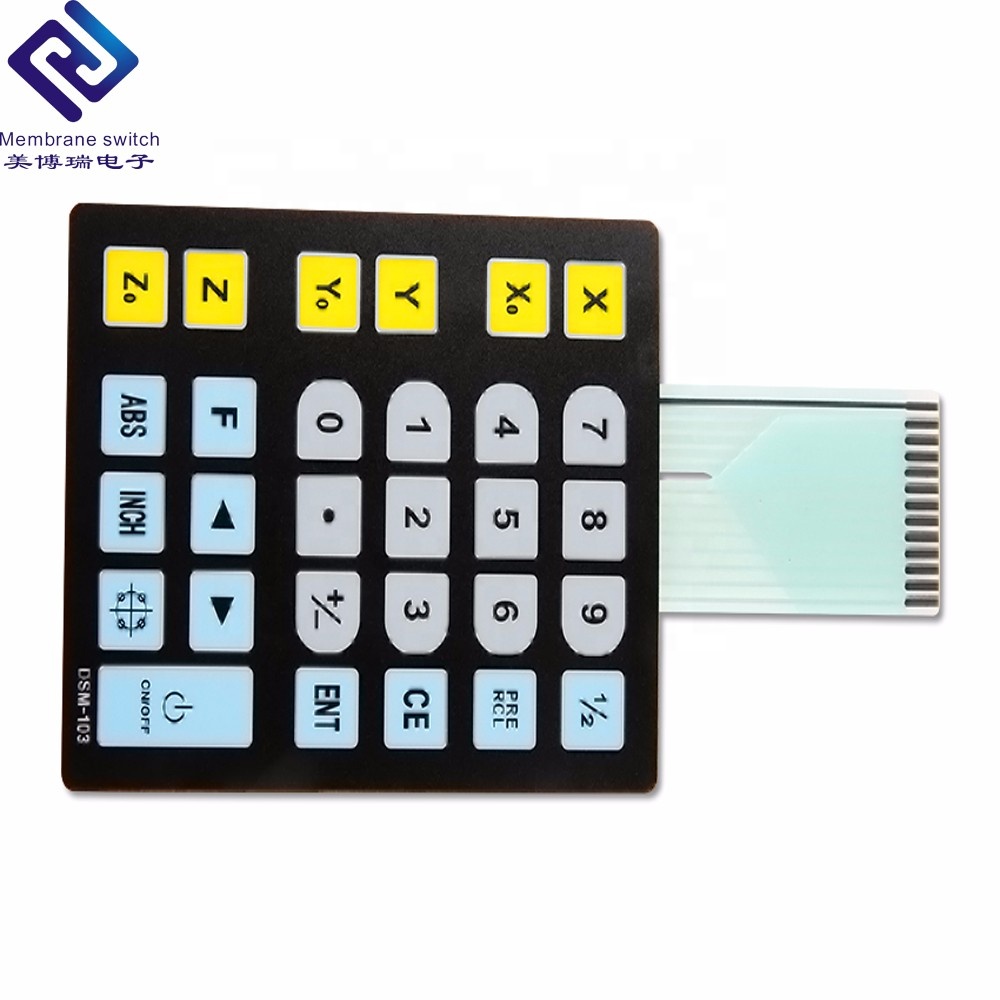
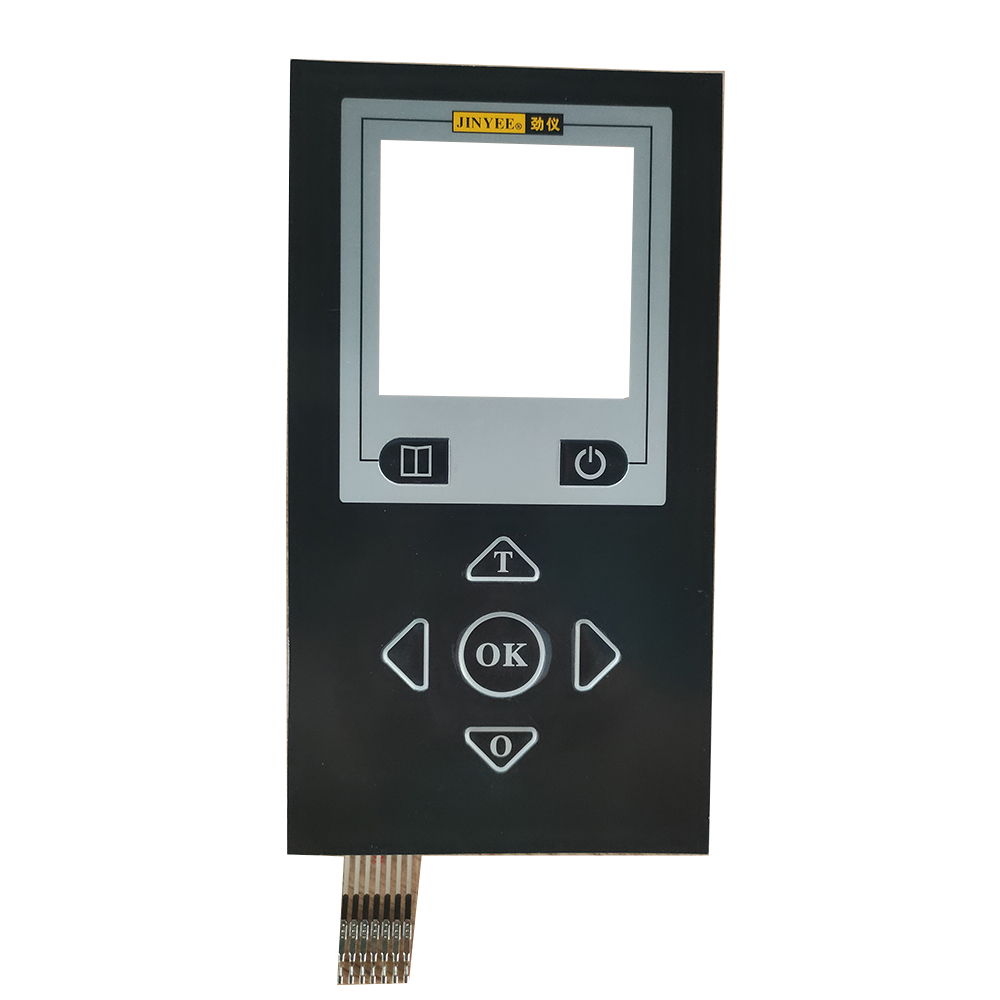
Standard Matrix 3x4 3*4 12 Key PET Matrix Array Membrane Button Switch Keyboard Keypad Waterproof Eco-friendly for Home Appliance

3x4 12-Key Industrial PET Matrix Array Switch

High Tactile 12-Pin Array Eco PET
Explore Specifications
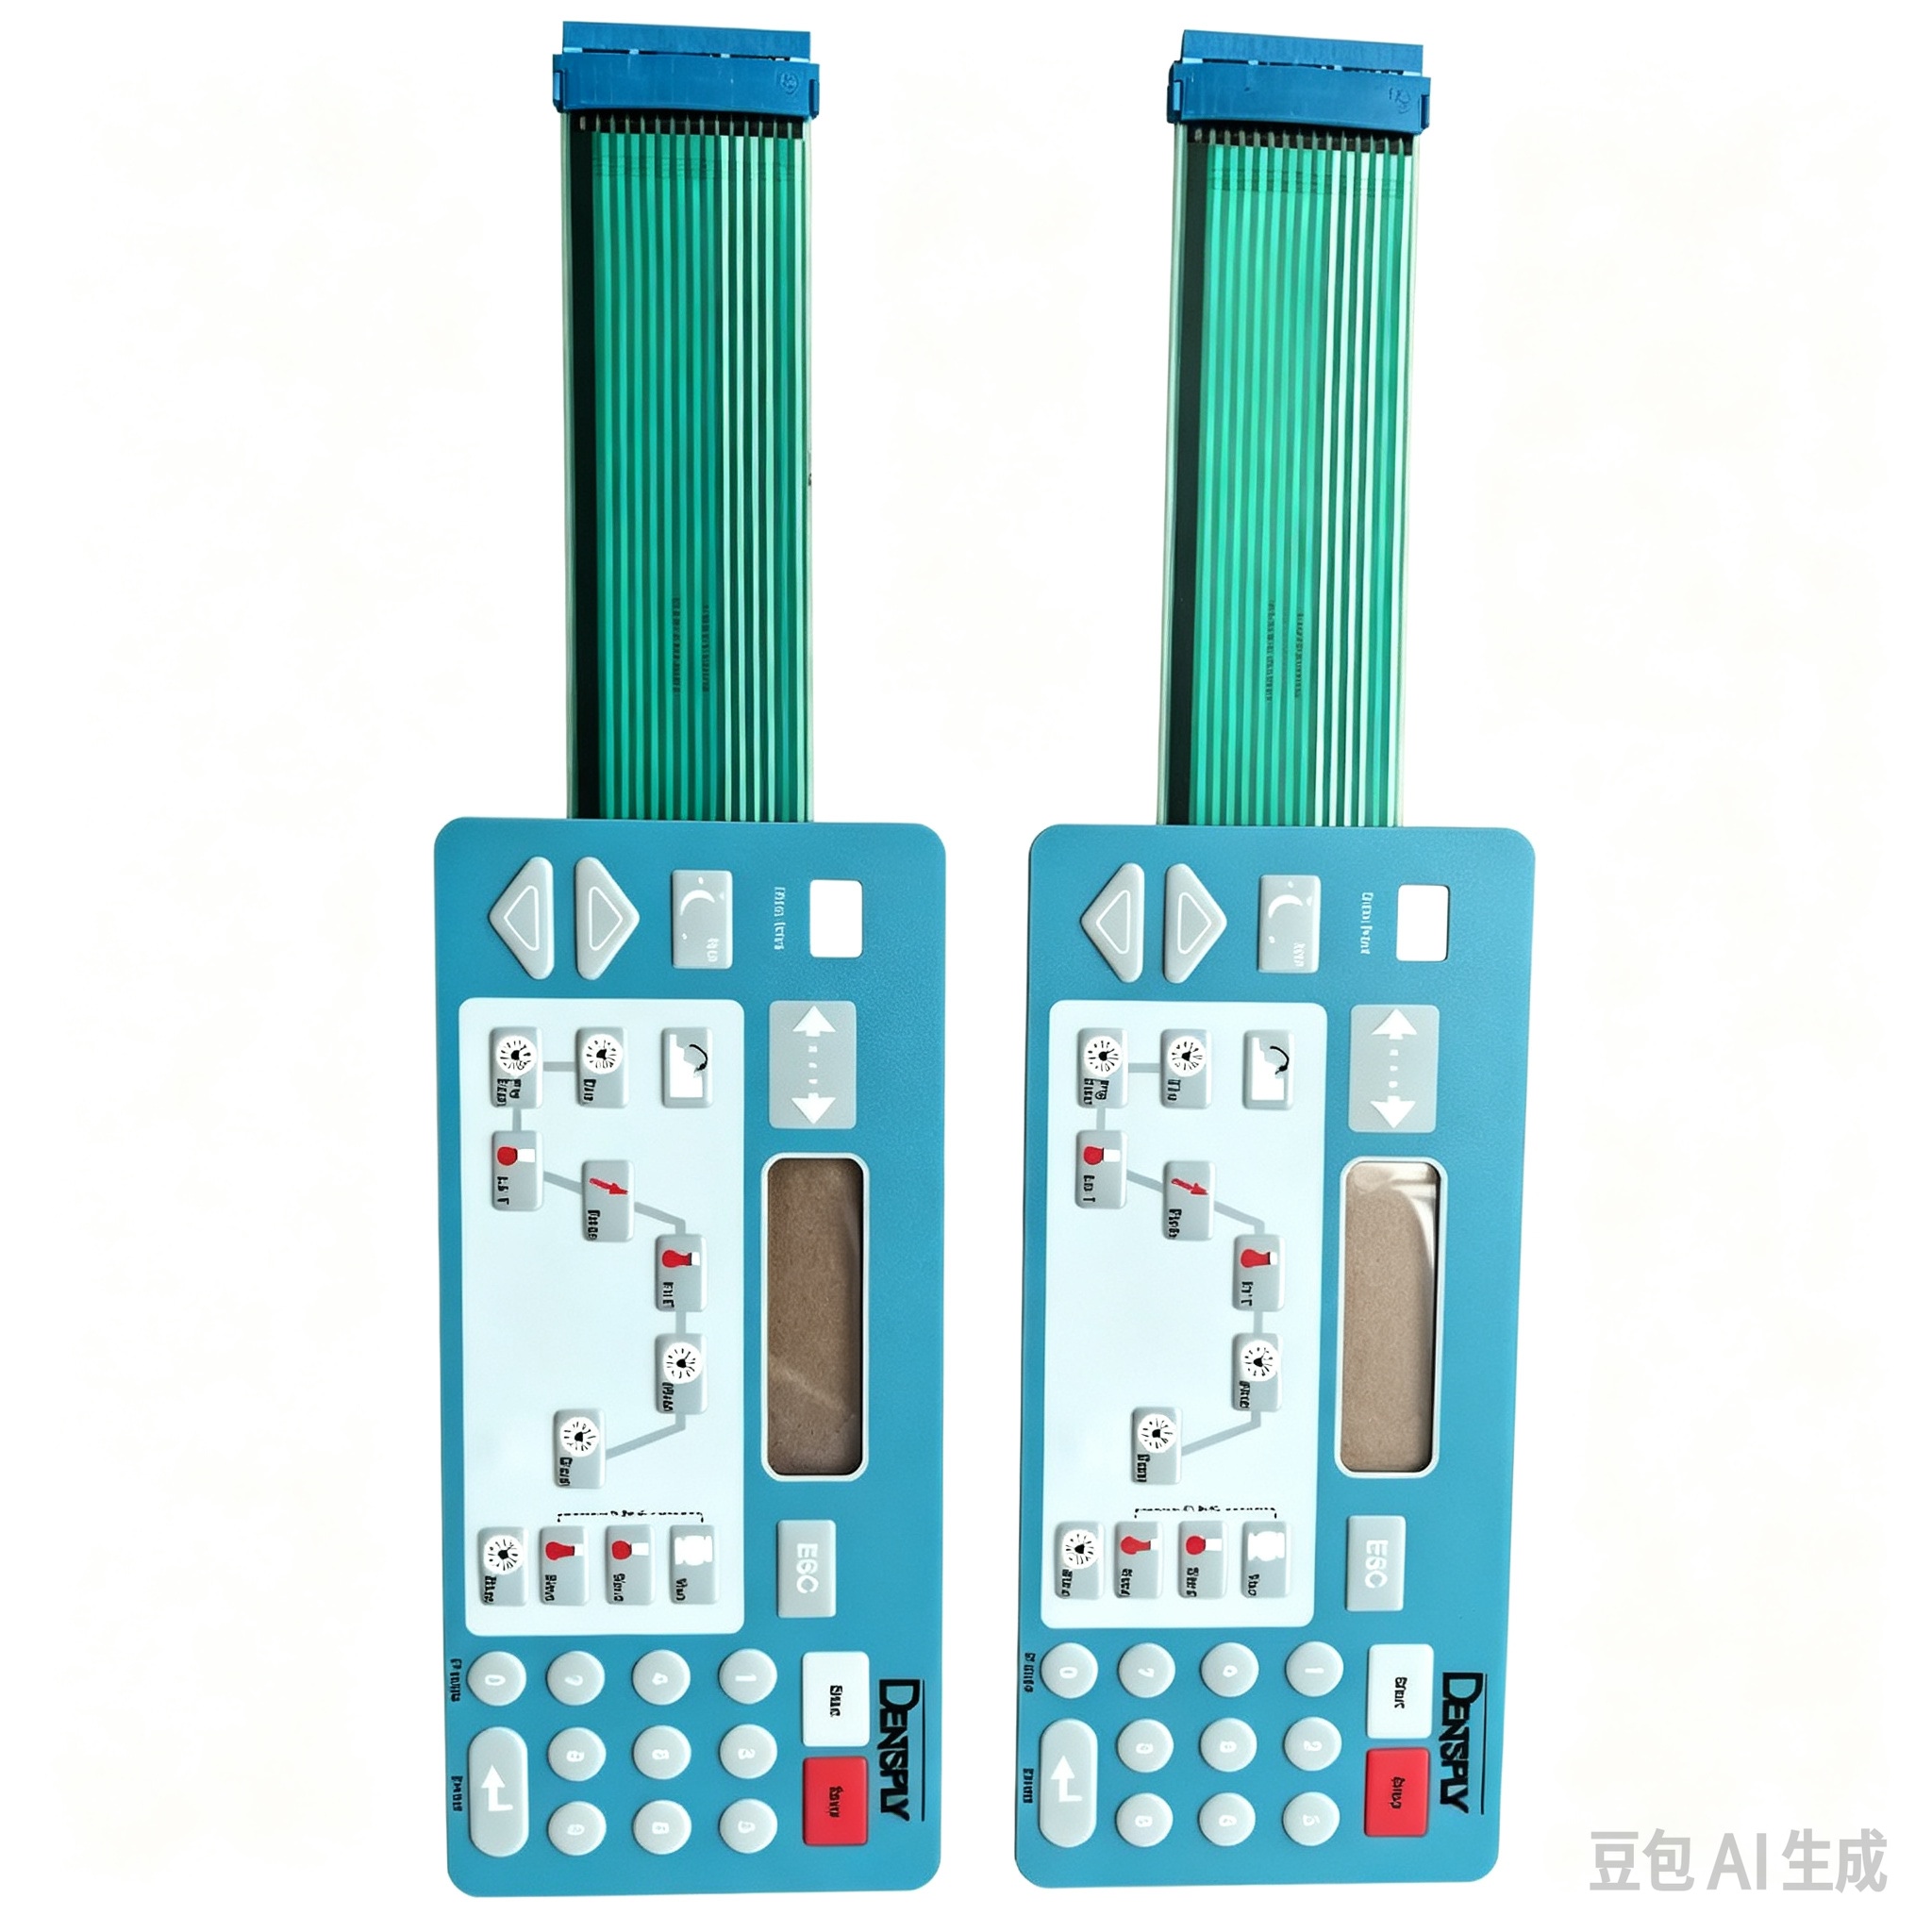
Mechanical Hybrid Fast Delivery OEM Waterproof Membrane Keyboard PBT Keyboard Cap Mechanical Switch Compatible Factory Direct Supply Free Sample

PBT Cap Mechanical-Compatible Membrane System

PBT Keycaps Tactile Core Fast Turnaround
Explore Specifications
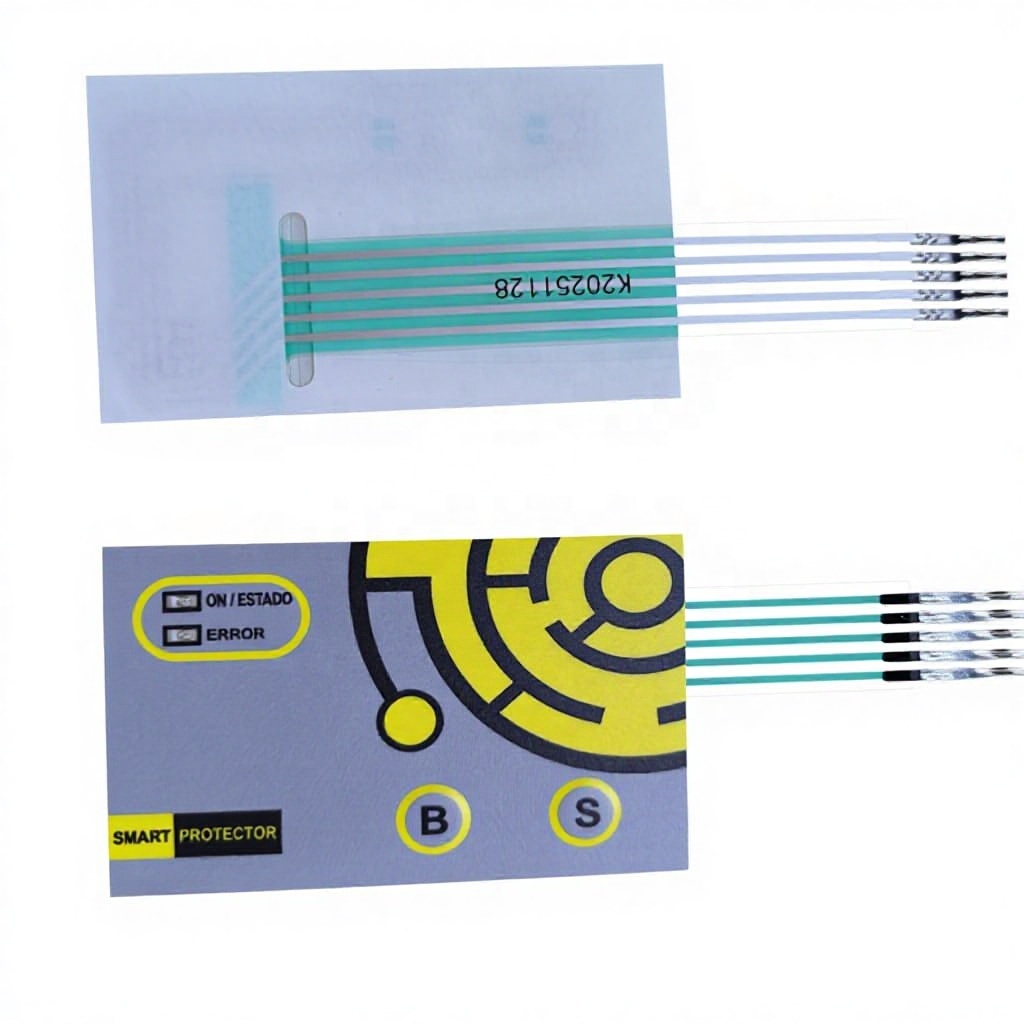
Cleanroom Built Factory Custom Waterproof Polyester Membrane Switch On Off Button Panel

Custom Polyester Membrane On/Off Control Panel

Autotype PET Embossed Dome 1M+ Clicks
Explore Specifications
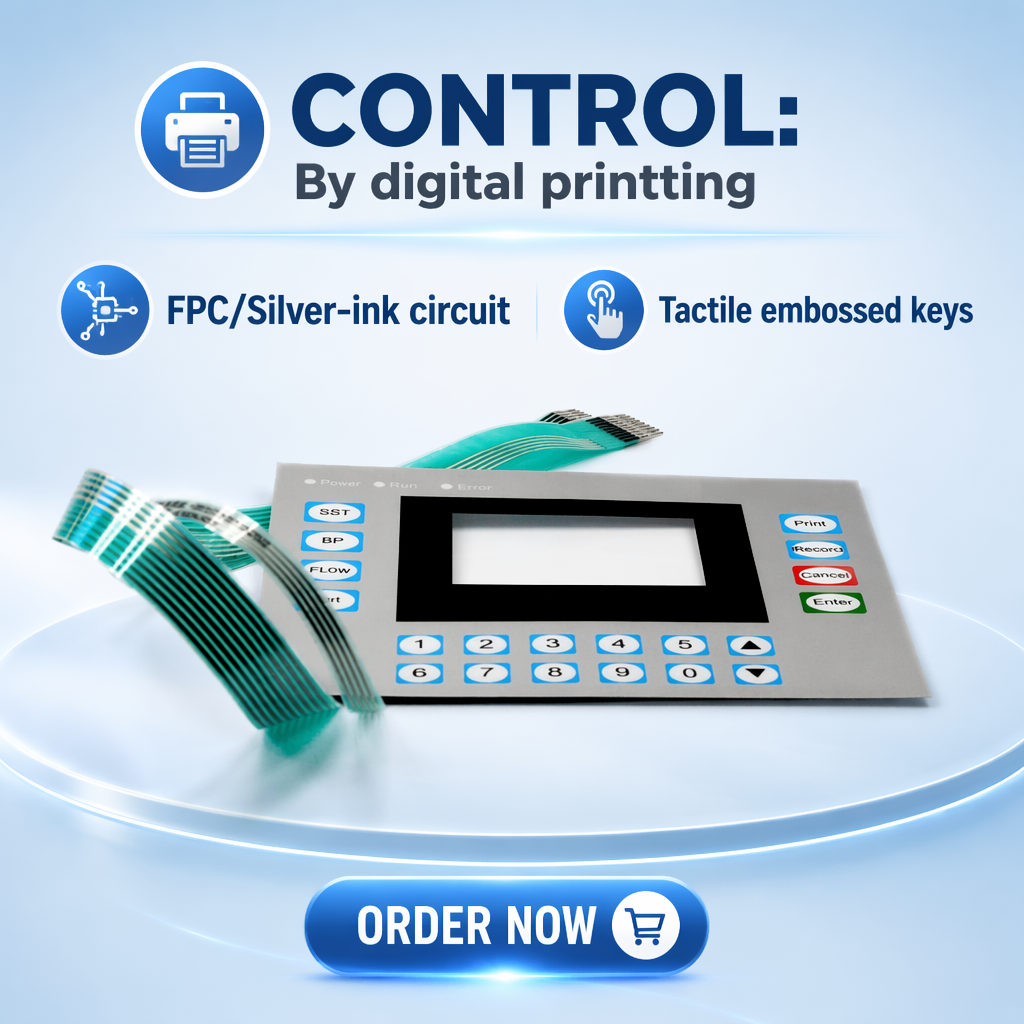
Extreme Grade MBR IP67 Waterproof Industrial Membrane Keyboard PET Overlay for Telecommunication Equipment (OEM/ODM Model)

Industrial Sealed Telecommunication Keyboard Panel

IP67 Enclosure Wide Operating T° Zero-Bounce
Explore Specifications
Send an Inquiry
1990
Pioneering Heritage Since
111+
Verified Technical Specialists
2,219 ㎡
Cleanroom Manufacturing Floor
1M+ Pcs
Exported to Europe & Global Hubs
Alpine Applications

High-Altitude Engineering: Serving Encamp's Industrial & Infrastructure Matrix

Encamp sits at an average altitude exceeding 1,250 meters in the heart of the Pyrenean corridor. Equipment deployed here experiences severe atmospheric pressure shifts, dense snowpack condensation, freeze-thaw cycles, and elevated UV exposure.

Ski Lift & Cable Transit Controls (Funicamp)

Encamp hosts one of the world's most critical aerial tramways connecting the town to Grandvalira. Our stainless steel dome assemblies deliver crisp, unambiguous tactile snap even through heavy synthetic ski gloves, guaranteed over 1,000,000 continuous operations at -30°C.

Alpine Telecommunications & Microwave Relays

Ridge-top transmitter units and base stations throughout the Parish require IP67 and IP68 hermetically sealed interface overlays with EMI/RFI conductive grid shielding to prevent interference, water ingress from blowing ice, and long-term polyester embrittlement.

Hydroelectric & Civil Water Monitoring

FEDA's historic and modernized hydroelectric installations along the Valira d'Orient river require industrial control consoles resistant to continuous humidity, sulfur exposure, and pressurized washdowns without surface fogging or micro-switch debonding.

Engineering Whitepaper: Overcoming Pyrenean Environmental Stresses in HMI Design

Designing human-machine interface (HMI) keypads for the mountainous parishes of Andorra requires fundamentally rethinking material physics. At elevations between 1,200m and 2,500m around Encamp, standard commercial keypads quickly experience catastrophic failures: membrane venting paths clog with frozen condensation, plastic overlays suffer brittle fracture under sub-zero actuation, and internal silver trace oxidation accelerates due to diurnal temperature swings ranging over 25°C within hours.

1. Sub-Zero Elastomeric & Polyester Science

To resist structural degradation, TAVO specifies high-grade biaxially oriented polyethylene terephthalate (Autotype MacDermid Autotex PET) rather than conventional polycarbonate (PC). Polycarbonate becomes glass-brittle around -10°C, leading to edge cracking and tactile fatigue. Our heat-stabilized PET films maintain flexural modulus down to -40°C, resisting dynamic flexing under repetitive glove-hammering by ski facility operators and municipal road maintenance crews.

2. Atmospheric Venting Architecture vs. Condensation Sealing

A classic challenge in alpine keypad design is dome venting. If a keypad is entirely airtight, altitude pressure differential causes the air pocket behind the metal snap dome to balloon outwards or collapse, ruining tactile feedback. TAVO engineers utilize customized labyrinth vent channels baffled with hydro-phobic, oleo-phobic ePTFE filtration membranes. This equalizes atmospheric pressure instantly during mountain transit without admitting vapor, meeting true IP67 submersion criteria.

3. Trace Metallurgy: Screened Silver vs. Flexible Copper (FPC)

While screen-printed silver ink tracks on polyester provide an economical solution for stable indoor environments, high-altitude installations subject to thermal vibration and current spikes perform significantly better with Flexible Printed Circuits (FPC). Our rolled annealed copper polyimide circuits eliminate micro-fissuring and electromigration. SMT components, including bi-color status LEDs, decoupling capacitors, and zero-insertion-force (ZIF) headers, are mechanically anchored via thermo-compression epoxy bonding to survive aggressive operational conditions.

4. Next-Gen Trends in Andorran Industrial Sourcing (2025–2030)

  • Transition to LGF (Light Guide Film) Uniform Backlighting: Operators working night snow groomers and mountain rescue relays need uniform, low-glare keypad visibility without heat concentration. Our 0.125mm LGF layers distribute side-fired LED light across critical keys while pulling minimal current.
  • Integrated Rigid Aluminum & FR4 Backers: Rather than forcing technicians in Encamp to adhere thin membranes onto uneven metal chassis in freezing conditions, TAVO delivers factory-laminated, stud-mounted aluminum backer plates with pre-applied precision die-cut gaskets.
  • Capacitive Hybrid Interfaces with Tactile Safeguards: Incorporating both projected capacitive touch surfaces and mechanical perimeter tactile cancel buttons to ensure immediate emergency shut-off even when gloves are soaked with snow slurry.
Send an Inquiry
Enterprise Reliability

Why Sourcing Managers in Southern Europe Partner with TAVO

With roots reaching back to 1990, TAVO combines thirty years of proprietary manufacturing heritage with European technological exchange to serve leading global enterprises including Siemens, ABB, and Haier.

100% In-House Vertical Processing

From CAD layout, film plotting, and precision screen printing to Mimaki UV digital color replication, embossing, laser cutting, cleanroom lamination, and 100% automated continuity verification—no steps are subcontracted, eliminating third-party latency and quality degradation.

German Technical Partnership

Our long-term operational and technical collaboration with a premier German membrane switch plant directly governs our tooling standards, adhesive layer validation (3M 467MP, 468MP, and VHB series), and dimensional tolerance controls (±0.05mm).

Dual-Facility Supply Chain Guarantee

Operating high-capacity manufacturing centers in Xianghe (Robot Industry Port) and Huizhou (Southern Industrial Hub) with 111+ full-time specialists, 60 CNC mold suites, and 37 automated silkscreen printers ensuring uninterrupted production pipelines.

Comprehensive In-House Test Laboratory

Every custom production run is validated through programmable temperature/humidity chambers (-50°C to +150°C), xenon lamp UV accelerated weatherometers, automated salt fog corrosion chambers, and pneumatic key life-cycle testers exceeding 1,000,000 actuations.

Full Prototype & Low-MOQ Flexibility

We actively accommodate European engineering departments developing high-mix, low-volume specialist gear. Rapid prototyping delivers functional, laser-cut samples within 5–7 working days for pilot testing prior to mass tooling investment.

Seamless Global Logistics to Andorra

Experienced with Andorran customs clearance pathways via Toulouse (Blagnac) and Barcelona (El Prat). Full export compliance with CE, RoHS, REACH, and ISO 9001 certifications accompanied by comprehensive DDP/DAP/FOB documentation.

Procurement Clarity

Frequently Asked Questions for Sourcing in Encamp

Essential technical and logistical answers for project managers, hardware engineers, and supply chain directors.

What CAD and artwork files are required to initiate tooling and prototyping?
To generate preliminary production blueprints, our 10-person CAD team requires an outline mechanical drawing (DXF, DWG, or vector PDF) specifying external contours, window cutouts, and connector egress coordinates. Graphic overlay files should be supplied in vector format (Adobe Illustrator .AI or CorelDraw .CDR) with exact Pantone Solid Coated (PMS) or RAL color references. Circuit routing can be shared as a schematic schematic netlist or pinout pin-to-key matrix map.
How do you guarantee keypad adhesion on equipment stored outdoors in cold alpine winter conditions?
Adhesion failure under freeze-thaw cycles is the most frequent issue in high-altitude environments. We specify genuine 3M 467MP, 468MP, or 3M VHB structural acrylic adhesives matched precisely to your substrate (cast aluminum, powder-coated steel, ABS, or polycarbonate). Furthermore, we design moisture-diverting internal perimeter seals and recommend surface degreasing protocols with isopropyl alcohol prior to application at temperatures above 15°C to achieve full cross-linking bonding before cold-temperature exposure.
Can you provide tactile metal domes that provide reliable actuation through heavy ski or work gloves?
Yes. Standard human finger actuation requires approximately 200g to 280g of actuation force. For alpine, industrial, and transportation hardware used by gloved operators in Encamp, we integrate heavy-snap stainless steel domes rated at 350g, 420g, or up to 500g force with key travel distances between 0.6mm and 0.9mm. This delivers a pronounced mechanical "click" feedback audible and palpable through insulated gloves.
How are import shipments delivered to Encamp and Andorra without customs hold-ups?
While Andorra is not part of the EU Single Market, it maintains customs agreements via Spain and France. Our export department routinely coordinates express DDP (Delivered Duty Paid) shipments via DHL, FedEx, and specialized European freight carriers routed through customs control stations in Sant Julià de Lòria (Spain border) or Pas de la Casa (France border). All commercial invoices, HS commodity codes (8537.10 / 8471.60), and Certificates of Origin are meticulously prepared to prevent local transit delays.
Do you support batch sizes under 500 units for specialized Andorran municipal or resort runs?
Yes. We intentionally avoid excessive Minimum Order Quantities (MOQs). By utilizing high-resolution Mimaki digital UV printing systems alongside digital CNC knife plotting and laser cutting, we produce pilot runs from 50 to 250 units without requiring expensive steel die-cut or screen setup fees. Once your field trials in Encamp confirm operational success, we scale smoothly into multi-thousand unit automated mass production.
What is the typical turnaround lead time from approval of technical drawings?
Standard engineering design review and 2D/3D blueprint approval take 24 to 48 hours. Rapid functional prototypes generally dispatch within 7 to 10 business days. Full production orders typically ship within 15 to 20 working days, with air courier delivery to Andorra taking an additional 4 to 6 business days.

Transform Your Machine Interface Today

Whether you require sub-zero resistant keypad membranes for alpine infrastructure, high-density FPC arrays, or EMI-shielded telecom controls, our specialized engineering team is ready to analyze your technical specifications.

Send an Inquiry