Catalog & Prototypes
High-Reliability Embedded LED Keypads & HMI Assemblies
Engineered to survive corrosive media, washdown cycles, and millions of actuations in industrial machinery, intelligent instruments, and mission-critical controls.
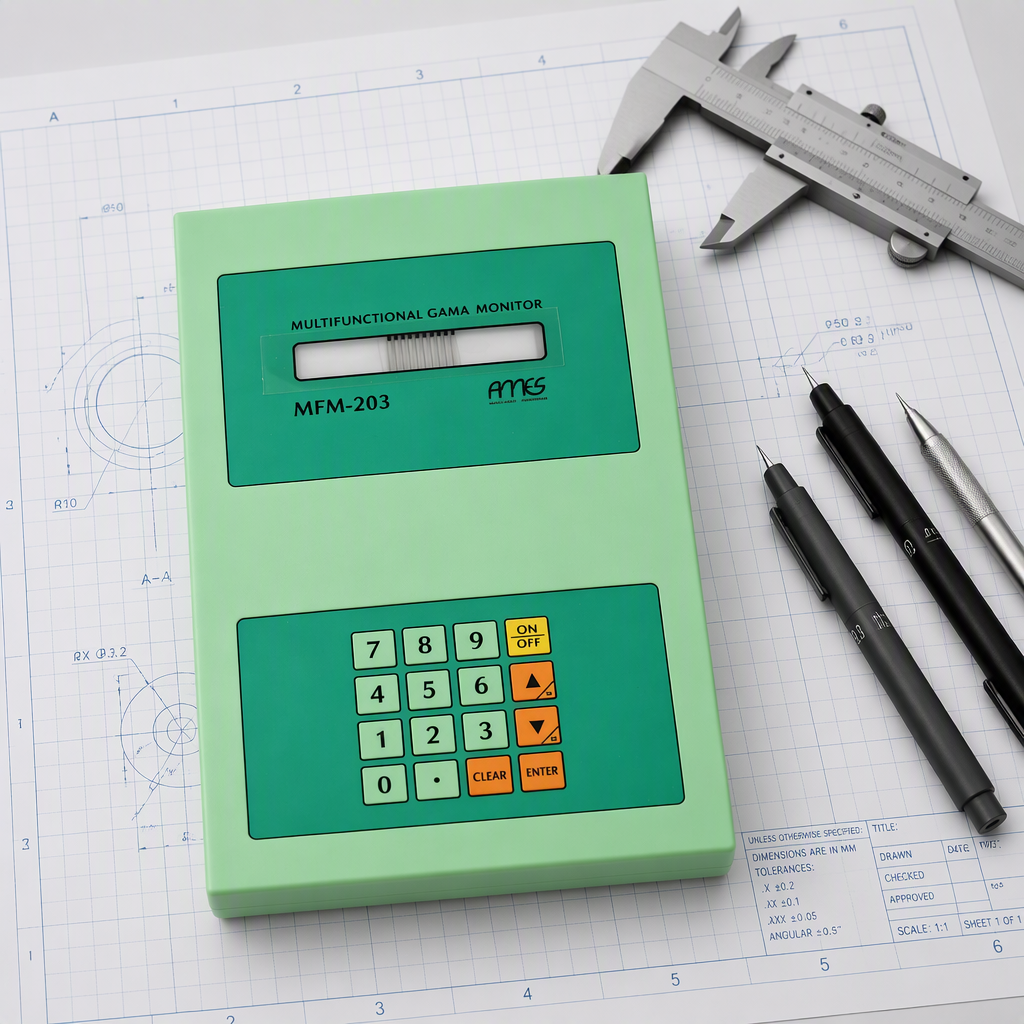
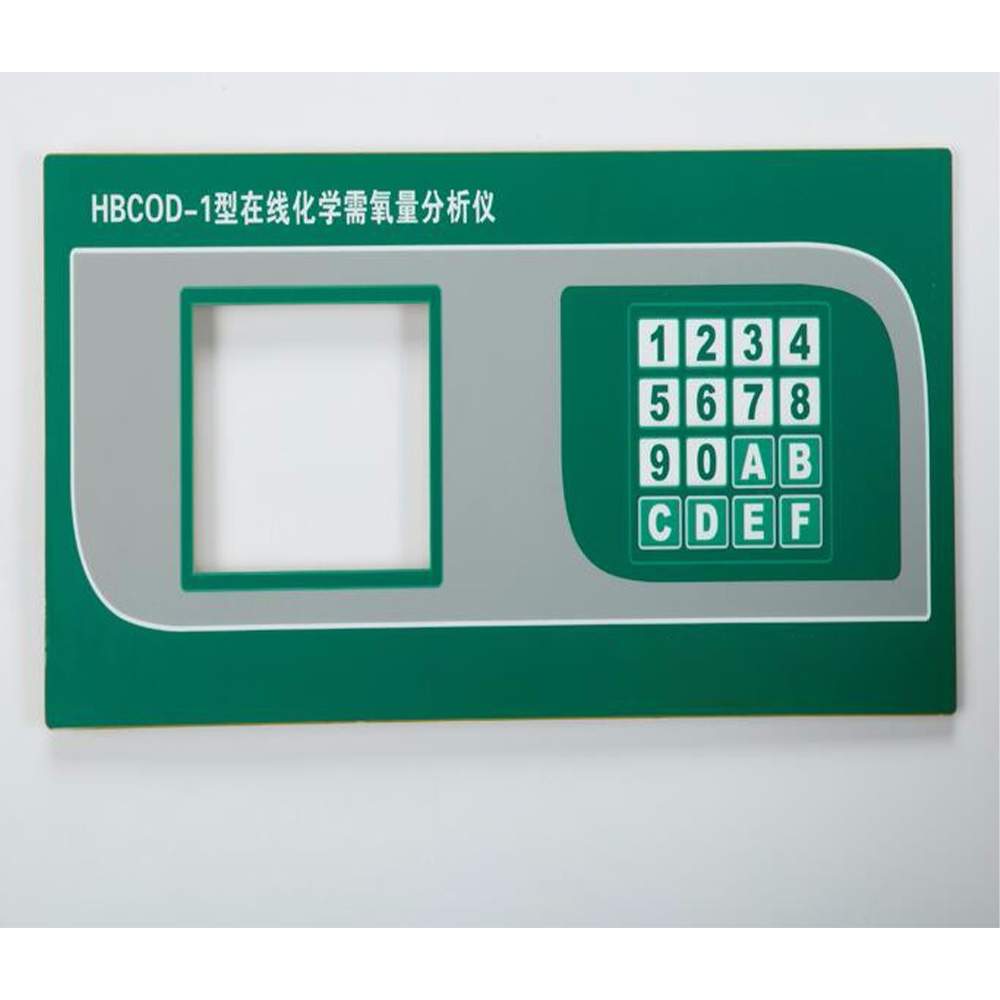
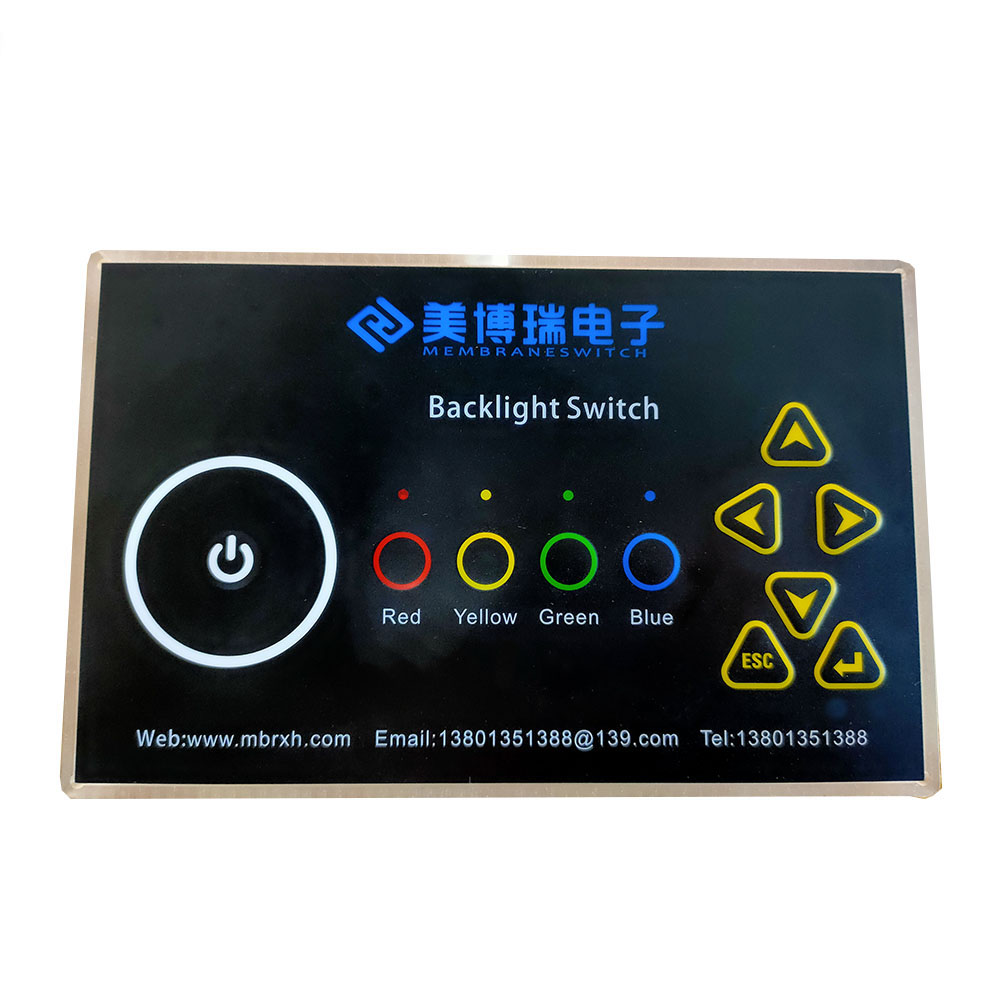
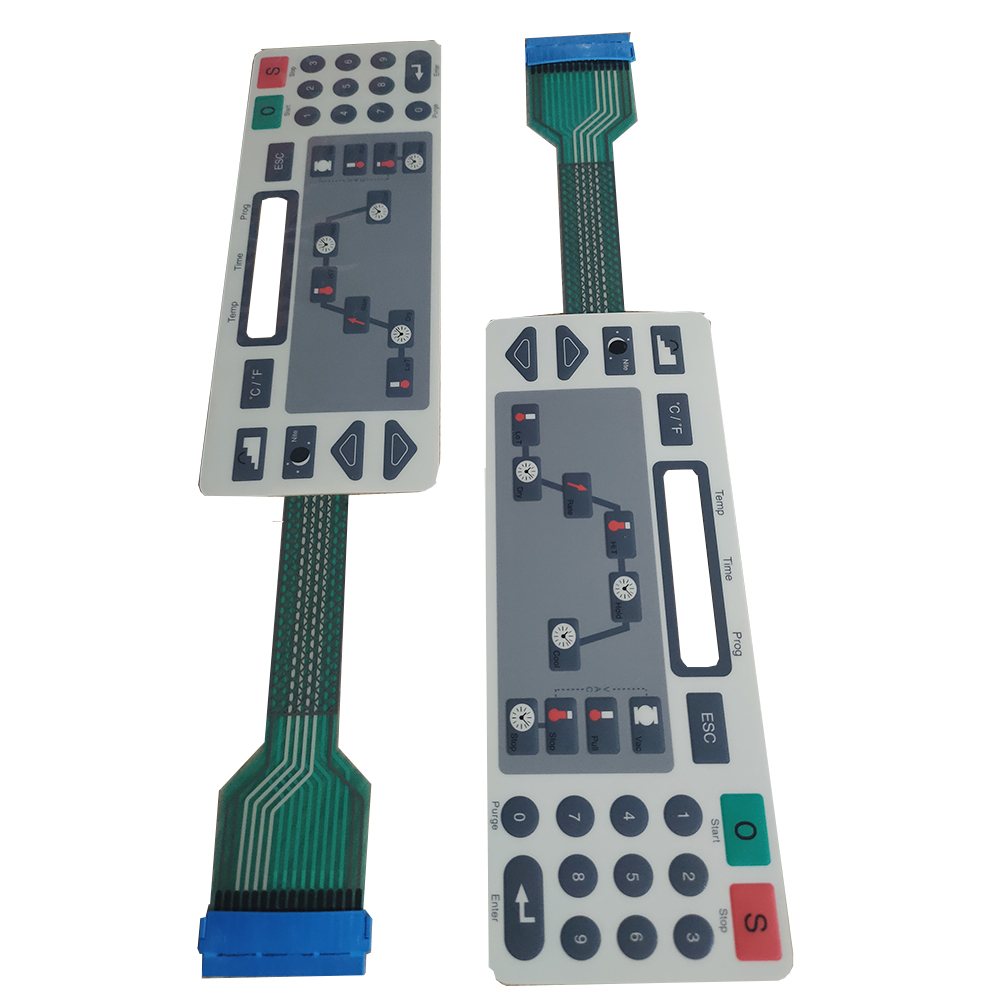
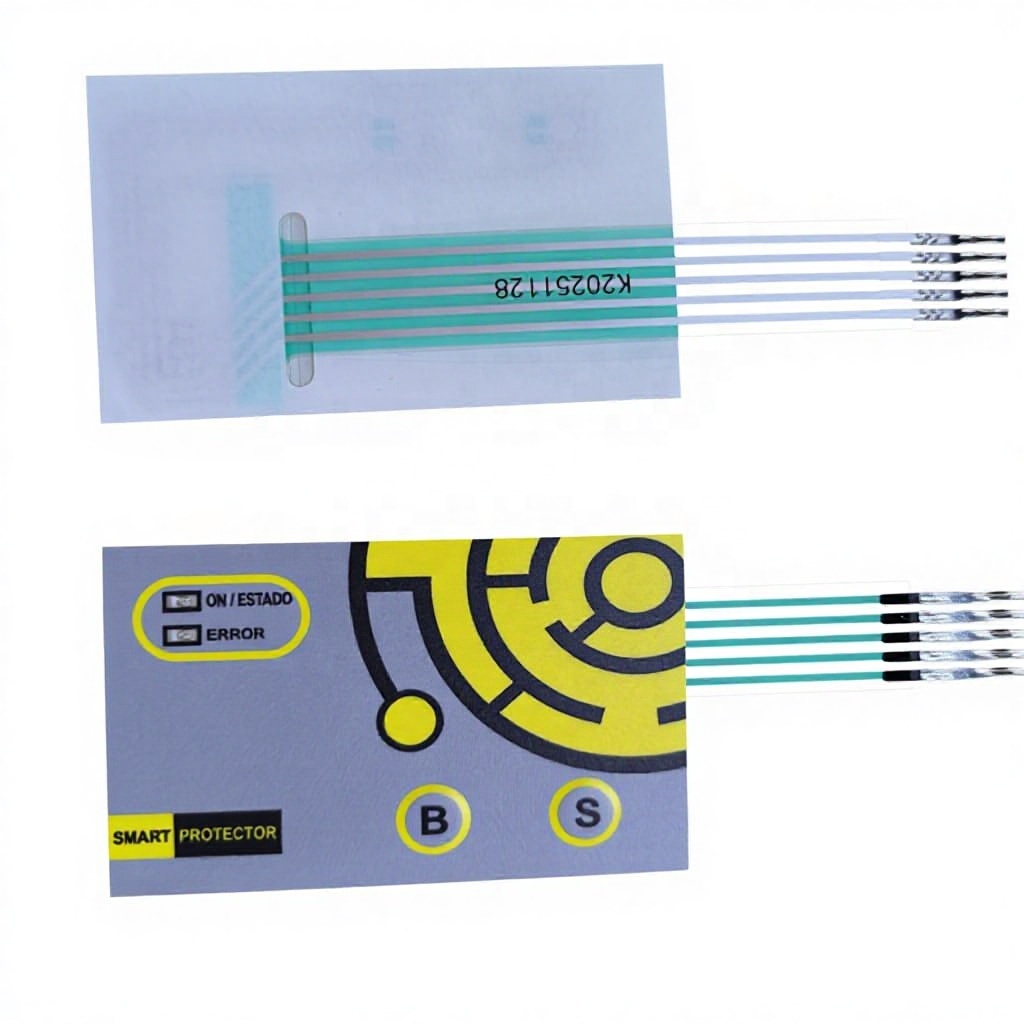
Engineering Analysis: Sourcing Embedded LED Keypad Modules for the Serravalle Market
The industrial ecosystem surrounding Serravalle—spanning northern Italy's Piedmont-Liguria precision automation corridors and San Marino’s specialized electromechanical equipment manufacturing clusters—demands human-machine interface (HMI) hardware with exceptional resilience. For European procurement managers, systems architects, and industrial equipment builders, securing an OEM manufacturing partner that bridges technical micro-engineering with lean production flexibility is essential for sustaining international competitiveness.
Embedded LED keypad modules represent a fundamental evolution over legacy passive membrane panels. By directly integrating Surface-Mount Device (SMD) light-emitting diodes, Light Guide Film (LGF) networks, and capacitive tactile feedback assemblies directly onto Flexible Printed Circuits (FPC) or precision silver-screened substrates, modern control panels achieve ultra-thin footprints without sacrificing tactile or optical clarity. Operating inside harsh factory environments subject to hydraulic oil spray, chemical washdowns, and high ambient vibration makes sub-component structural engineering paramount.
Comparative Architecture: Silver Flex Circuit vs. Copper Polyimide (FPC) Keypads
A frequent dilemma encountered during design-for-manufacturability (DFM) reviews for Serravalle-bound equipment is selecting between screen-printed conductive silver ink tracks on polyester (PET) and photolithographically etched copper traces on flexible polyimide (PI) films. While conductive silver ink remains a cost-effective standard for standard commercial consumer electronics, high-vibration industrial automation hardware requires the ductile endurance and low trace resistance of FPC technology.
| Performance Parameter | PET Screen-Printed Silver Traces | Polyimide (PI) Etched Copper (FPC) | Rigid FR4 Backed LED Membrane |
|---|---|---|---|
| Trace Resistance | < 1.0 Ω/cm (Varies with trace width) | < 0.05 Ω/cm (Negligible voltage drop) | < 0.01 Ω/cm (Ideal for dense LED arrays) |
| LED SMT Mounting Method | Conductive epoxy bonding (Silver glue) | Lead-free reflow soldering (SAC305) | Standard SMT reflow & wave soldering |
| Vibration Fatigue Limit | Moderate (Micro-fissuring risk > 5G) | High (Ductile rolled-annealed copper) | Exceptional (Solid structural substrate) |
| Actuation Life Expectancy | 1,000,000 to 3,000,000 cycles | > 5,000,000 cycles (with stainless domes) | > 5,000,000 cycles |
| Ingress Protection Rating | IP65 (Perimeter 3M 467MP gasket) | IP67 / IP68 (Ultrasonic perimeter weld) | IP67 / NEMA 4X (With O-ring bevels) |
Market Trends & Localized Industrial Applications across Serravalle and European Hubs
As modern packaging machinery, food-processing equipment, and multi-axis CNC machine tools across northern Italy and the wider European basin evolve toward Industry 4.0 standards, HMI modules are no longer simple contact closures. In Serravalle's industrial sub-sectors, three specific application frontiers dictate current keypad specifications:
CNC Metalworking & Milling
Keypads applied directly to machine tool consoles encounter continuous splashes of water-soluble coolants and synthetic lubricants. Overlays manufactured from biaxially oriented textured polyester (Autotex XE) combined with hermetically sealed embossed stainless-steel snap domes prevent chemical embrittlement and phantom keystrokes.
Medical & Diagnostic Diagnostics
Diagnostic laboratory equipment requires perfectly smooth front panels featuring antimicrobial surface coatings that withstand frequent disinfection using isopropyl alcohol, bleach, and quaternary ammonium solutions. Embedded status LEDs provide unambiguous visual confirmations of sterilization and operational states.
Smart Industrial Infrastructure
Outdoor access terminals, energy metering panels, and automated gate systems across regional logistic facilities must endure extreme solar exposure and thermal cycling (-30°C to +75°C). Optical-grade anti-UV polycarbonate graphic windows and high-brightness side-lit LEDs ensure daytime readability.
Inside TAVO: End-to-End Manufacturing Prowess & Quality Architecture
Founded in 1990, TAVO Electronic Information Technology Co., Ltd. has established itself as an authoritative leader in engineered human-machine interface technologies. Rather than acting as a broker or trading intermediary, TAVO maintains a fully enclosed, vertically integrated industrial framework across two advanced production facilities in Xianghe Robot Industry Port (Hebei) and Huizhou (Guangdong). This strategic dual-plant synergy ensures robust business continuity, agile tooling turnaround, and the capacity to manufacture over 1,000,000 precision units annually for discerning clients in Germany, Italy, Switzerland, and the United States.
ISO 9001 Certified & Intertek Assessed Operations
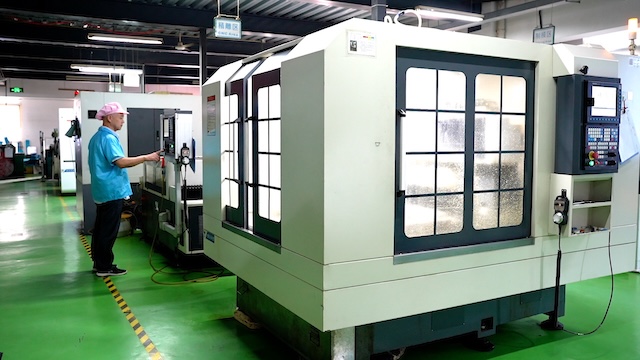
Our 2,219-square-meter facility houses cleanroom production suites maintaining strict temperature and particle-count stabilization. Every key processing step—from precision vector silkscreen rendering and high-speed digital UV printing to surface-mount pick-and-place component soldering, pneumatic key embossing, laser die-cutting, and multi-pin electrical continuity analysis—is kept 100% in-house under uncompromised process auditing.
60 CNC Mold Centers
37 Screen Printers
18 Laser Cutters
4 Mimaki UV Units
Intertek Inspected
Stringent Reliability Verification in In-House Laboratories
To uphold long-standing design endorsements from global industrial leaders such as Siemens, ABB, and Haier, TAVO subjects each membrane keypad run to a rigorous testing gauntlet prior to delivery packaging:
1. Automated Button Life-Cycle Testing: Pneumatic finger actuators depress tactile switches at 3 to 5 Hz cycles, ensuring uninterrupted actuation through over 1,000,000 to 5,000,000 operations without dome micro-cracking or contact resistance escalation.
2. Programmable Thermal & Humidity Chambers: Thermal shock and damp-heat aging cycles verify that adhesive lamination boundaries (featuring genuine 3M 467MP, 468MP, or VHB systems) experience zero delamination or silver migration.
3. Salt Fog & Xenon Aging: Overlays undergo ASTM B117 salt fog corrosion testing and intense xenon arc weathering chambers to assure graphic colorfastness and complete sealing of embedded LED driver circuits against atmospheric moisture.
Top 10 Criteria for Qualifying an Embedded LED Keypad Factory for Serravalle
When selecting a manufacturing partner for embedded illuminated switch panels, engineering teams should evaluate prospective suppliers against these critical industrial benchmarks:
1. In-House Cleanroom SMT Placement
Avoid vendors who subcontract LED soldering to third-party workshops. Dedicated cleanroom surface mounting ensures high alignment accuracy for ultra-compact 0603 or 0805 reverse-mount LEDs, eliminating short circuits and cold solder joints.
2. LGF Backlighting Uniformity
Direct point LEDs can generate distracting hot spots. Leading factories specialize in Light Guide Film (LGF) molding, utilizing micro-dot matrices that refract illumination evenly across key legends while drawing minimal drive currents.
3. Complete Traceability of Adhesives
Harsh ambient operational envelopes necessitate verifiable industrial adhesive systems (such as genuine 3M 200MP acrylic series). Inferior generic laminates inevitably fail through adhesive creep, bubble formation, or fluid leakage.
4. Comprehensive Continuity Verification
Verify that the manufacturer implements 100% automated electrical pin-out testing for loop resistance, open/short circuits, insulation resistance, and LED forward voltage verification prior to export palletization.
5. Solid Structural Backer Integration
For high-load industrial controllers, top-tier factories machine aluminum, stainless-steel, or FR4 backing plates with integrated PEM studs, creating plug-and-play drop-in console sub-assemblies.
6. Flexible Prototyping Policies
Advanced R&D requires rapid prototype iterations. Seek suppliers capable of delivering precision laser-cut and digital UV-printed functional prototypes in low batches to accelerate product field trials.
Buyer Sourcing Insights
Serravalle Procurement: Frequently Asked Questions
Essential guidance covering technical requirements, order logistics, trade compliance, and mechanical specifications.
What design files and specifications are required to initiate an embedded LED keypad quote?
To generate an accurate DFM review and quotation, our engineering team requires:
1. Vector Mechanical Outline: DXF, DWG, or vector PDF detailing overall dimensions, cutouts, embossing profiles, and tail egress dimensions.
2. Graphic Artwork: Adobe Illustrator (.AI) or CDR files with designated Pantone matching system (PMS) or RAL color codes.
3. Electrical Schematic: Circuit pin-out diagram, connector type (e.g., 2.54mm pitch female housing, zero-insertion-force ZIF contacts), and LED forward voltage/current ratings.
4. Operating Environment: Ambient temperature ranges, chemical contact expectations, and required ingress ratings (e.g., IP65 or IP67).
2. Graphic Artwork: Adobe Illustrator (.AI) or CDR files with designated Pantone matching system (PMS) or RAL color codes.
3. Electrical Schematic: Circuit pin-out diagram, connector type (e.g., 2.54mm pitch female housing, zero-insertion-force ZIF contacts), and LED forward voltage/current ratings.
4. Operating Environment: Ambient temperature ranges, chemical contact expectations, and required ingress ratings (e.g., IP65 or IP67).
How are LEDs embedded into thin membrane switch profiles without causing surface bulges?
TAVO utilizes precision spacer routing and embossed relief pockets tailored to the exact package dimensions of surface-mount LEDs (typically miniature 0603, 0805, or side-firing LEDs). Furthermore, we integrate Light Guide Film (LGF) layers measuring as thin as 0.125mm to 0.25mm, which diffuse light laterally across the key legend from side-mounted light sources, allowing the finished keypad assembly to maintain a sleek, planar profile under 1.5mm total thickness.
Can TAVO supply complete plug-and-play assemblies with aluminum backers and stud mounts?
Yes. We regularly produce integrated assemblies featuring CNC-machined, anodized aluminum or brushed stainless-steel backing plates. These are fitted with press-fit threaded PEM standoffs, integrated LCD display bezel frames, EMI/RFI shielding foils, and pre-mounted rigid PCB interface boards, eliminating multiple sub-assembly steps for your local assembly technicians.
What international delivery terms and quality assurances are provided for shipments to Europe?
We support standard Incoterms including FOB, CFR, CIF, and DDP via express air courier or container ocean freight directly to Italian and regional logistics hubs. Quality is certified under ISO 9001:2015, with full batch certificates of conformance (CoC), material compliance records (RoHS, REACH), and inspection reports provided alongside every dispatch.
What is the typical turnaround time for custom prototypes versus production runs?
Utilizing our digital UV Mimaki printers and high-precision laser profiling equipment, prototype units are typically completed and dispatched within 5 to 8 business days following engineering drawing sign-off. Full production orders requiring precision die-tooling, metal stamping, and cleanroom silkscreen runs typically ship within 14 to 20 business days.