Precision HMI & Membrane Switch Portfolio
Field-proven switch architectures engineered for continuous mechanical duty, high-humidity isolation, and uniform tactile feedback under adverse production conditions.
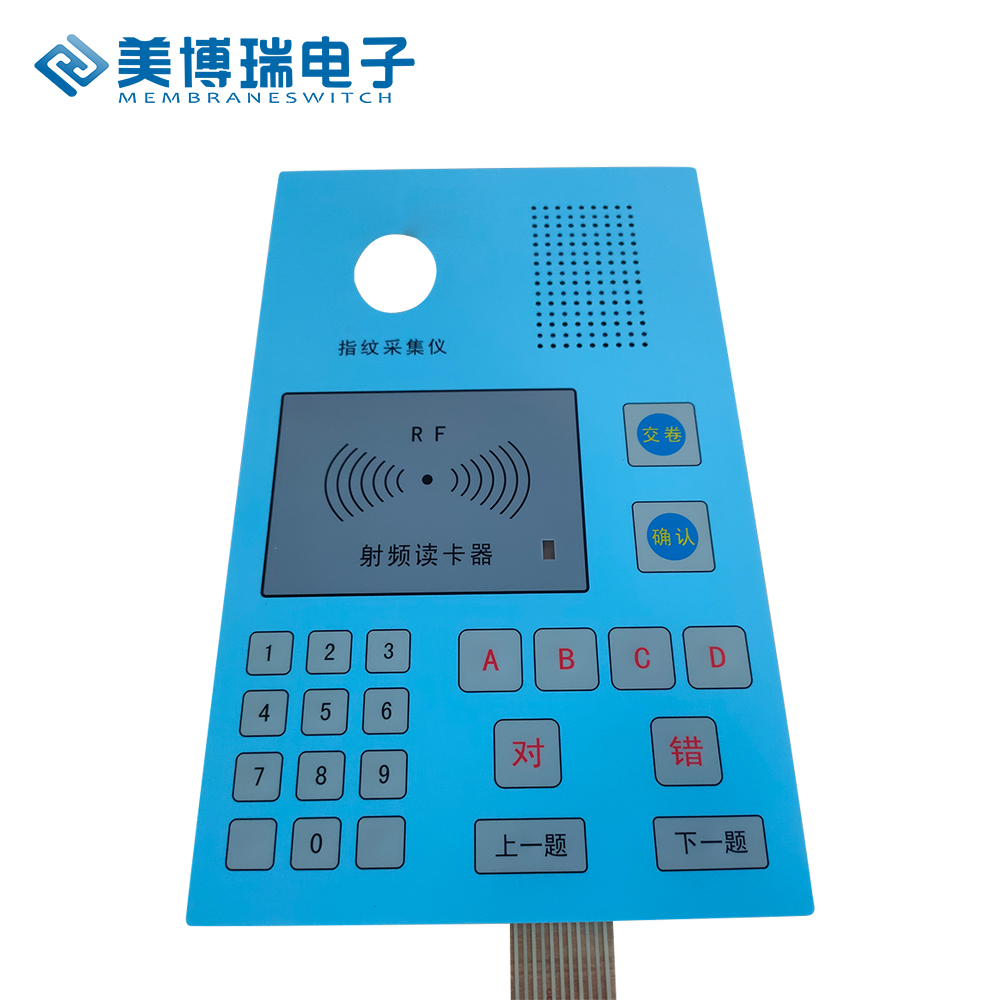
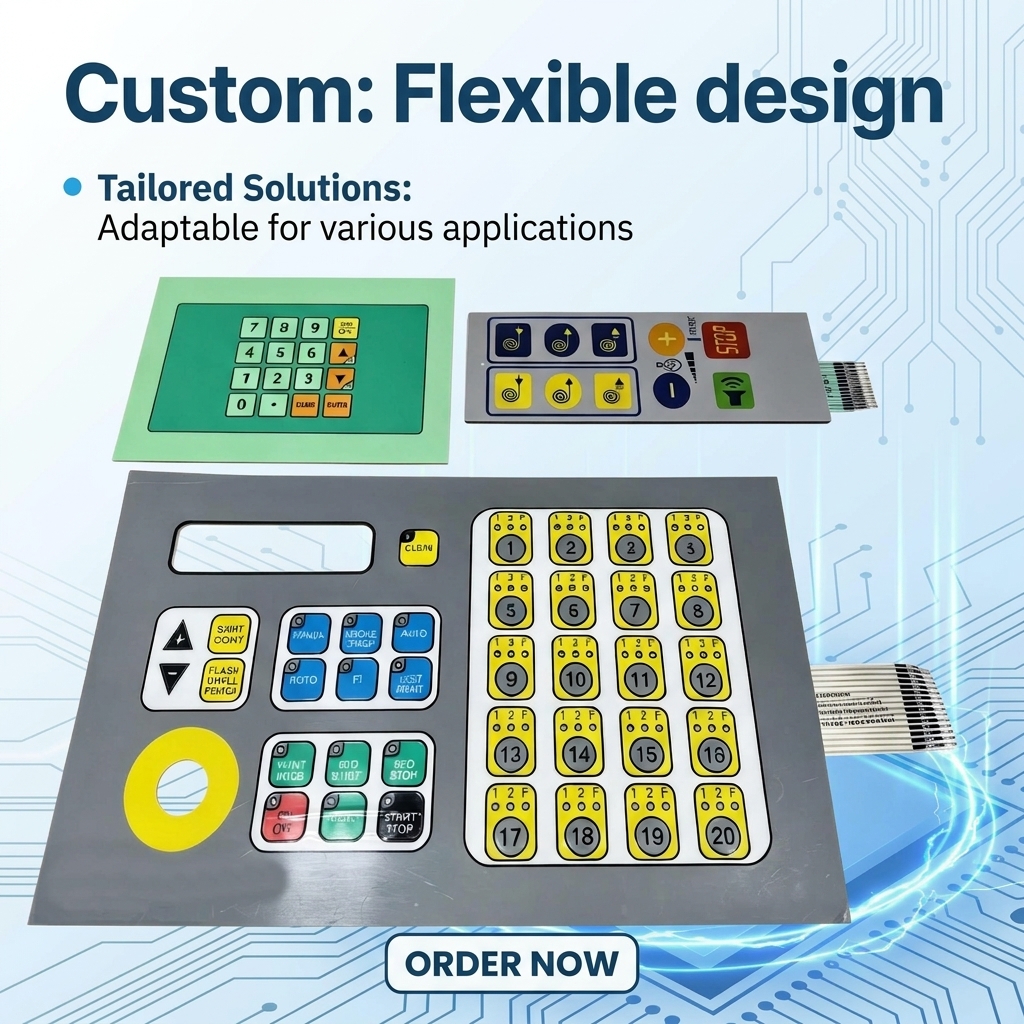
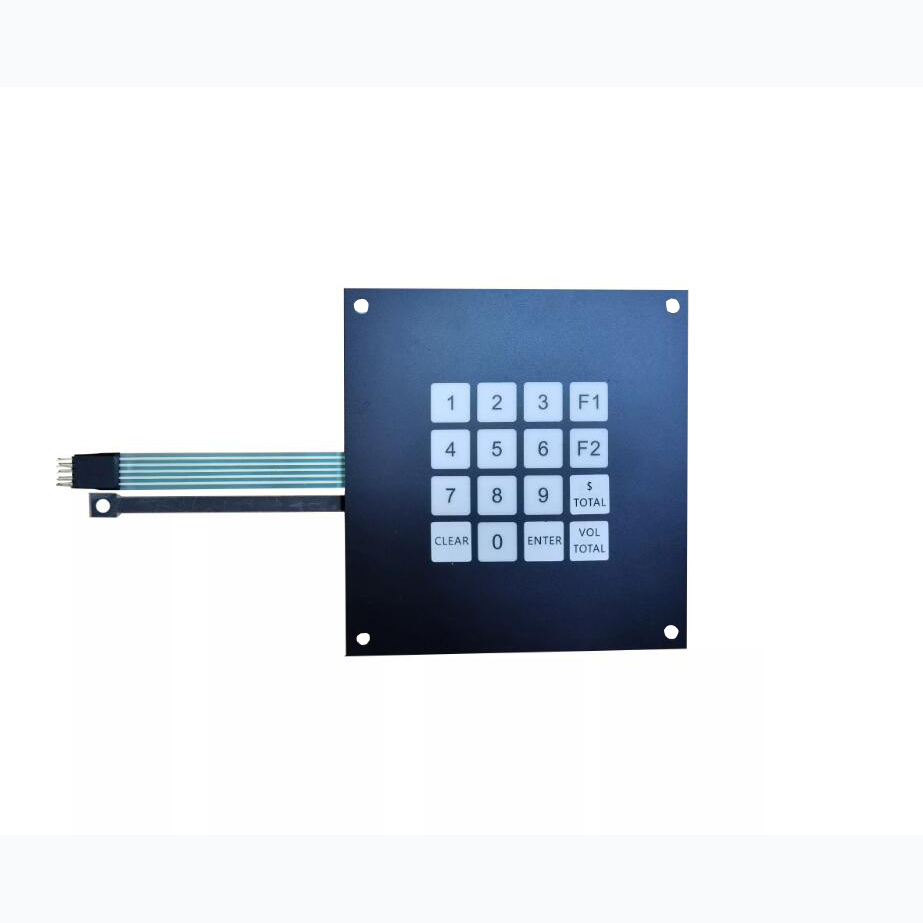
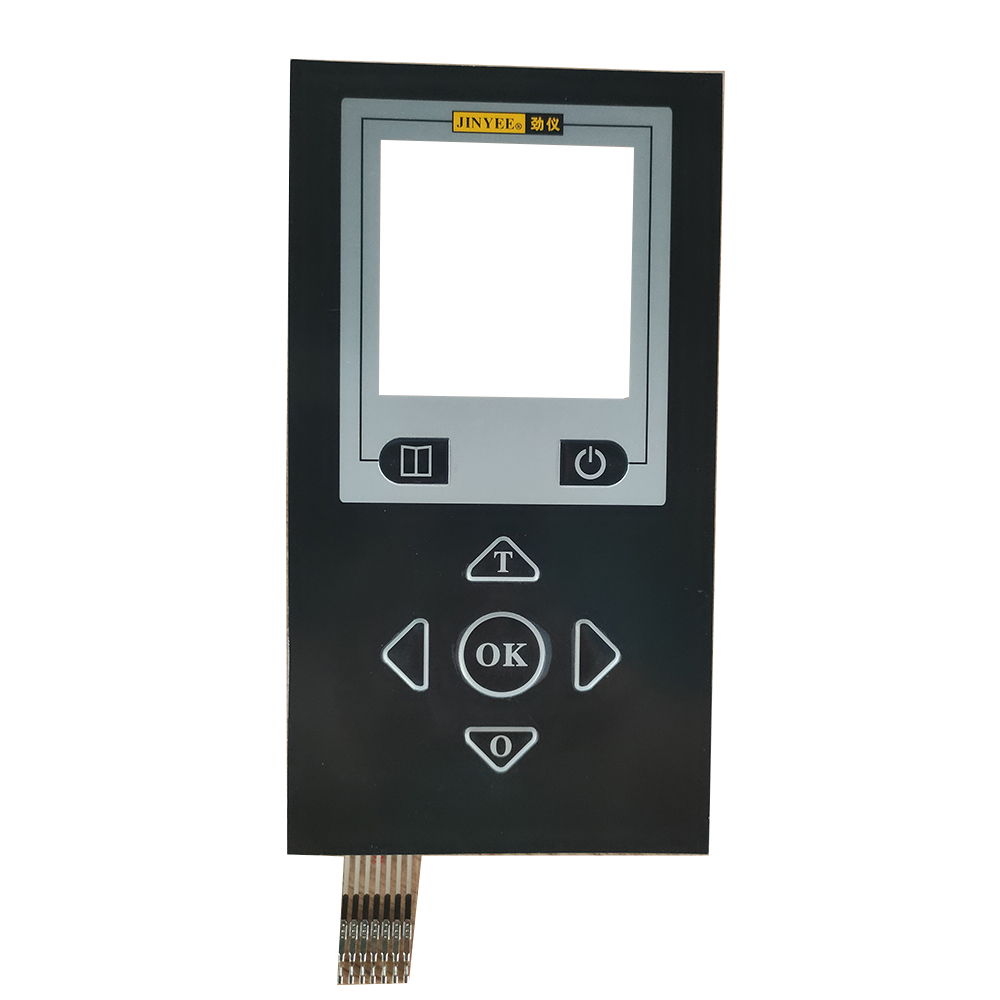
Physics & Mechanics of Light Guide Film (LGF) Interfaces
Why modern industrial systems in harsh operating climates have moved beyond legacy Electroluminescent (EL) foils and clustered point-source LEDs.
Micro-Dot Optical Diffusion
LGF technology utilizes precision optical-grade polycarbonate (PC) or PMMA film micro-embossed with computerized dot patterns. Light introduced via side-firing SMD LEDs travels via total internal reflection (TIR) and exits exclusively at dot coordinates, eliminating localized hot spots and delivering a luminescence variance across keys of under ±8%.
Ultra-Thin Cross Section
Traditional discrete backlighting requires 2.5mm to 4.5mm of spacer depth to diffuse point-source illumination. LGF layers measure between 0.125mm and 0.25mm, enabling full tactile metal dome integration within an ultra-slim total stack-up below 1.2mm without compromising mechanical switch travel or acoustic feedback.
Low Power & Thermal Balance
By relying on edge-coupled high-efficiency diodes (0603 or 0805 packages), an entire 24-key industrial keypad requires only 4 to 6 low-current LEDs. This reduces system thermal accumulation by over 70% compared to back-mounted LED grids—a critical design advantage inside unventilated IP66/IP67 control enclosures.
Standard Engineering Stack-up of an Industrial LGF Membrane Switch
Every custom interface manufactured by TAVO for critical export environments adheres to a multi-tier hermetically laminated structure, combining mechanical deflection integrity with continuous optical continuity:
Tailored Industrial Applications in Orange Walk Town, Belize
Serving northern Belize’s industrial heartland—where agro-industrial processing, severe tropical humidity, and continuous cane operations demand robust HMI engineering.
Sugar Cane Refining & Milling Controls
Orange Walk Town, known throughout Central America as Belize’s "Sugar City," centers around continuous-duty sugar extraction, boiling pans, centrifuges, and bagasse handling at facilities like Tower Hill. Our LGF membrane switches withstand acidic cane juice splashes, airborne molasses vapor, and fine fiber particulate. Impermeable polyester front overlays rated IP67 prevent ingress that destroys conventional push-button contact blocks.
Distillery & Rum Production Automation
Molasses fermentation and high-proof distillation environments require HMIs capable of operating in atmospheres with volatile organic compounds and frequent high-pressure steam washdowns. TAVO’s sealed graphic overlays, combined with intrinsically safe low-power LGF backlighting and spark-free gold-plated metal dome switches, provide operators with tactile control without ignition risk.
Heavy Agricultural Machinery & Haulers
Cane harvesters, tractor implements, and logistics trailers operating through the New River basin endure non-stop mechanical shock, vibration, and mud exposure during harvest season. Our FPC-backed LGF keypads feature copper circuitry that eliminates trace fracturing caused by diesel engine harmonic resonance, providing night-shift operators with clear, uniformly backlit controls.
Fuel Distribution & Commercial Oiling Stations
Orange Walk serves as a major trade artery on the Northern Highway connecting Belize City to Chetumal, Mexico. Our customized fuel dispenser keypads (Product #7) feature UV-stabilized Lexan polycarbonate with anti-fuel solvent barriers. The LGF backlight system guarantees clear legibility for 24-hour freight refueling depots even under bright tropical sunlight and pitch-black nocturnal shifts.
Water Pumping, Municipal & Solar Stations
Irrigation infrastructure along the Rio Hondo and Northern Lagoon relies heavily on remote solar-powered pump stations and telemetry units. The minimal current draw of TAVO’s LGF membrane keypads (often consuming less than 40mA total) ensures that automated supervisory control and data acquisition (SCADA) terminals can maintain continuous illuminated operation without draining backup battery banks.
Engineering Environmental Resilience Against Belizean Climate Stressors
A breakdown of failure modes typical of tropical environments and the exact material specifications TAVO implements to guarantee continuous field survivability.
| Environmental Stressor | Standard Commercial Issue | TAVO LGF Engineered Countermeasure | Lab Verification Standard |
|---|---|---|---|
| Tropical High Humidity (85%–98% RH) | Silver trace migration, delamination, internal moisture condensation. | Carbon overcoat printed on silver traces, FPC copper trace option, peripheral water-trap gaskets with 3M 300LSE adhesive. | Programmable damp heat chamber test: 60°C, 95% RH for 500 hours without resistance shift. |
| Intense UV Radiation & Sunlight | Embrittlement, micro-cracking of overlay, yellowing, graphic fading. | UV-stabilized Autotex XE exterior-grade polyester film with sub-surface UV digital inks and light-blocking silver blocking masks. | Xenon lamp accelerated weathering test chamber exceeding ASTM G155 standards for 1,000+ hours. |
| Airborne Bagasse Dust & Cane Ash | Dust infiltration under buttons causing open circuits or permanent contact sticking. | Full perimeter sealing with dead-front micro-embossed keys; hermetic cavity isolation separating tactile domes from atmospheric dust. | IP65 and IP67 particulate ingress testing compliant with IEC 60529. |
| Sulfur & Corrosive Salt Fog | Corrosion of dome contact pads and copper tails from coastal Caribbean trade winds. | Gold-plated metal domes (0.5μm Au) combined with nickel-plated contact interfaces and sealed ZIF FPC tail connectors. | Automated salt spray (fog) chamber test: 5% NaCl solution at 35°C for 96 continuous hours. |
| Repetitive Operator Actuation | Dome fatigue, collapse, loss of tactile crispness during 24/7 harvest shifts. | High-grade stainless steel tactile domes sourced from top-tier metallurgists rated for 1,000,000 to 3,000,000 actuations. | Automated pneumatic button life-cycle test rigs operating at 3Hz with calibrated load cell loggers. |
Emerging HMI Procurement & Technology Trends in Orange Walk Town
Strategic modernization across northern Belize is transforming requirements for industrial machine builders, electrical contractors, and plant operators.
Shift from Push-Buttons to Integrated Flat Panels
Processing facilities across Orange Walk are actively retrofitting legacy 22mm electrical push-buttons with fully sealed membrane keypads. Flat, non-porous front panels remove mechanical crevices where cane juice, bacteria, and dust accumulate, drastically cutting washdown times and preventing electrical shorts caused by moisture buildup during factory sanitation cycles.
Combined Capacitive & Tactile Hybrid Designs
Newer control cabinets installed in Belizean facilities increasingly specify hybrid interfaces: sleek capacitive touch sliders for adjusting conveyor speeds or pump rates paired with distinct tactile metal-dome buttons for emergency stops and prime triggers, ensuring operators can navigate controls while wearing heavy protective work gloves.
Direct OEM Sourcing & Replacement Agility
With equipment originating from European, American, and Asian builders, maintenance teams in Orange Walk often face excessive lead times and inflated costs when ordering replacement keypads through intermediaries. Sourcing directly from verified custom manufacturers like TAVO allows Belizean engineers to replicate legacy panels from original schematics or sample overlays in small-batch runs.
World-Class Manufacturing Prowess Backed by 30+ Years of Heritage
Combining German technical cooperation with complete in-house manufacturing integration to deliver uncompromised reliability for global export markets.
Full In-House Process Ownership
Every step of your membrane switch production—graphic layout engineering, digital film drafting, precision silkscreen and digital UV printing, key embossing, laser die-cutting, cleanroom assembly, and circuit testing—is executed internally. With 37 silkscreen printing machines, 4 Mimaki UV flatbeds, and 18 high-precision laser cutters, we eliminate outsourcing risks and maintain complete traceability.
Dual-Facility Capacity & Scalability
Operating our primary production facility in the Robot Industry Port of Xianghe Economic Development Zone, Hebei, complemented by a secondary specialized manufacturing base in Huizhou, Guangdong, TAVO balances order scheduling across both plants. This structure ensures that low-volume prototype builds for machinery retrofits receive the exact same engineering care as high-volume OEM production contracts.
Audited Quality Systems & Global Trust
TAVO is ISO 9001:2015 certified and onsite assessed by Intertek. Our membrane components are integrated into critical systems engineered by Siemens, ABB, and Haier, as well as high-speed railway locomotives and the Three Gorges hydro project. A long-standing technical collaboration with a German membrane switch manufacturer ensures European assembly tolerances across every shipment sent to Belize.
End-to-End Export & Customization Workflow for Orange Walk Buyers
A dependable, transparent path from your preliminary drawing or failed field sample to delivered production batches in northern Belize.
1. Engineering Review & DFM
Submit your CAD drawings (DXF, DWG, Step), graphic vector artwork (AI, CorelDraw, PDF), or physical sample. Our 10-person design team evaluates pin-out assignments, tactile travel, and ingress seal perimeters to issue a detailed DFM report within 24 hours.
2. Prototyping & Color Match
Rapid digital UV proofing matched precisely to Pantone or RAL swatches. Laser-cut tooling facilitates functional prototypes within 5 to 7 working days, allowing your Belizean maintenance team to verify mechanical fit and tactile responsiveness directly on the control console.
3. 100% Circuit & QC Testing
Every switch batch undergoes 100% automated continuity, loop resistance, insulation breakdown, and LED forward voltage verification on computerized test rigs. Button stroke life and seal integrity are validated prior to cleanroom vacuum packing.
4. Express Logistics to Belize
Shipments are hermetically vacuum-sealed with silica desiccant packs to avoid maritime moisture exposure during transit. Dispatched via DHL, FedEx, or air cargo directly into Philip Goldson International Airport (BZE) with full commercial invoicing and export documentation for rapid clearance into Orange Walk Town.
Frequently Asked Questions by Orange Walk Sourcing Managers
Direct technical answers addressing environmental tolerances, tooling economics, circuit modifications, and cross-border delivery schedules.
Can LGF membrane switches withstand direct washdowns and cleaning chemicals in sugar refining and rum processing facilities?
How does Light Guide Film (LGF) compare to Electroluminescent (EL) backlighting under hot, humid tropical conditions?
Can you reverse-engineer a damaged membrane keypad from an imported agricultural machine if we lack CAD files?
What is the minimum order quantity (MOQ) for custom membrane keypads, and do you support small replacement runs?
Should we select screen-printed silver ink or Flexible Printed Circuits (FPC) for high-vibration equipment?
What are the typical lead times for delivery into Orange Walk Town, Belize?
How do you protect exported membrane switches against condensation and moisture during international shipment?
What international trade terms and payment methods are supported?
Ready to Engineer Your Custom Membrane Interface?
Consult directly with TAVO’s human-machine interface engineering team. Send your technical drawings, environmental specifications, or machinery replacement requirements for a rapid design review, DFM analysis, and firm quotation.