High-Reliability PCB & Membrane Interface Assemblies
Direct factory manufacturing featuring FR-4 rigid substrates, gold-flashed contact pads, custom PBT tooling, and laser-guided overlay printing tested beyond 1,000,000 actuations.
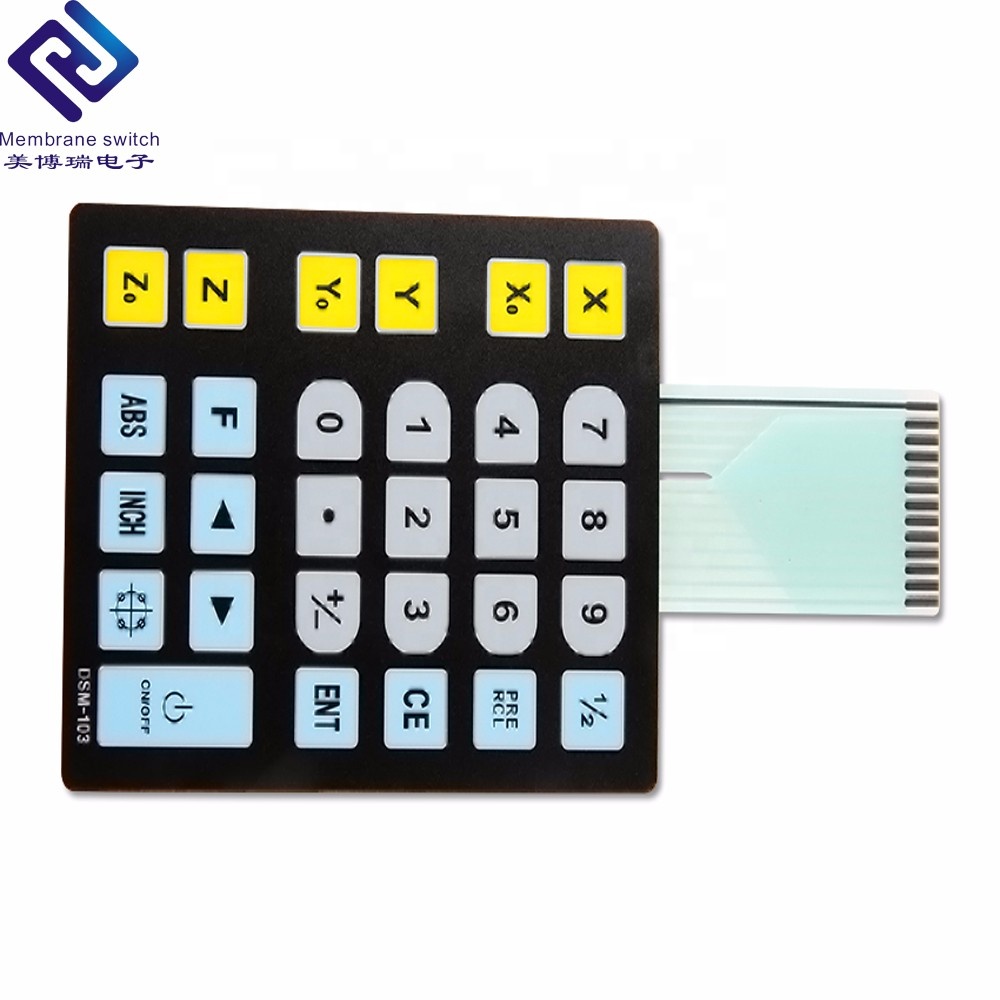
Factory Membrane Switch Keypad with Rubber Buttons 4*4/1*4/3*4/4*5 Layout MCU Expansion
Fast Delivery OEM PBT Keyboard Cap Mechanical Switch Compatible Silkscreen Printed 2.54mm Pitch
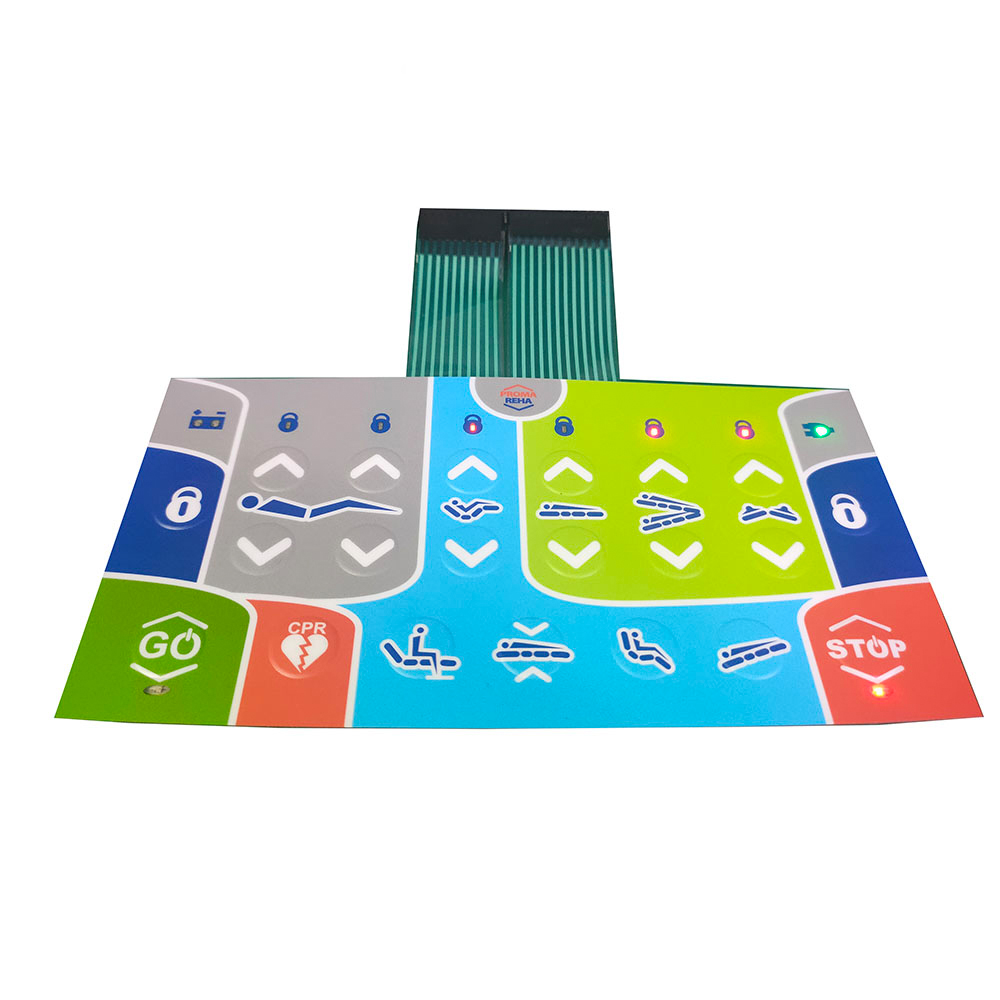
High Quality PBT Keyboard Cap Customized Color & Size Silkscreen Printing Fast Delivery Meiborui
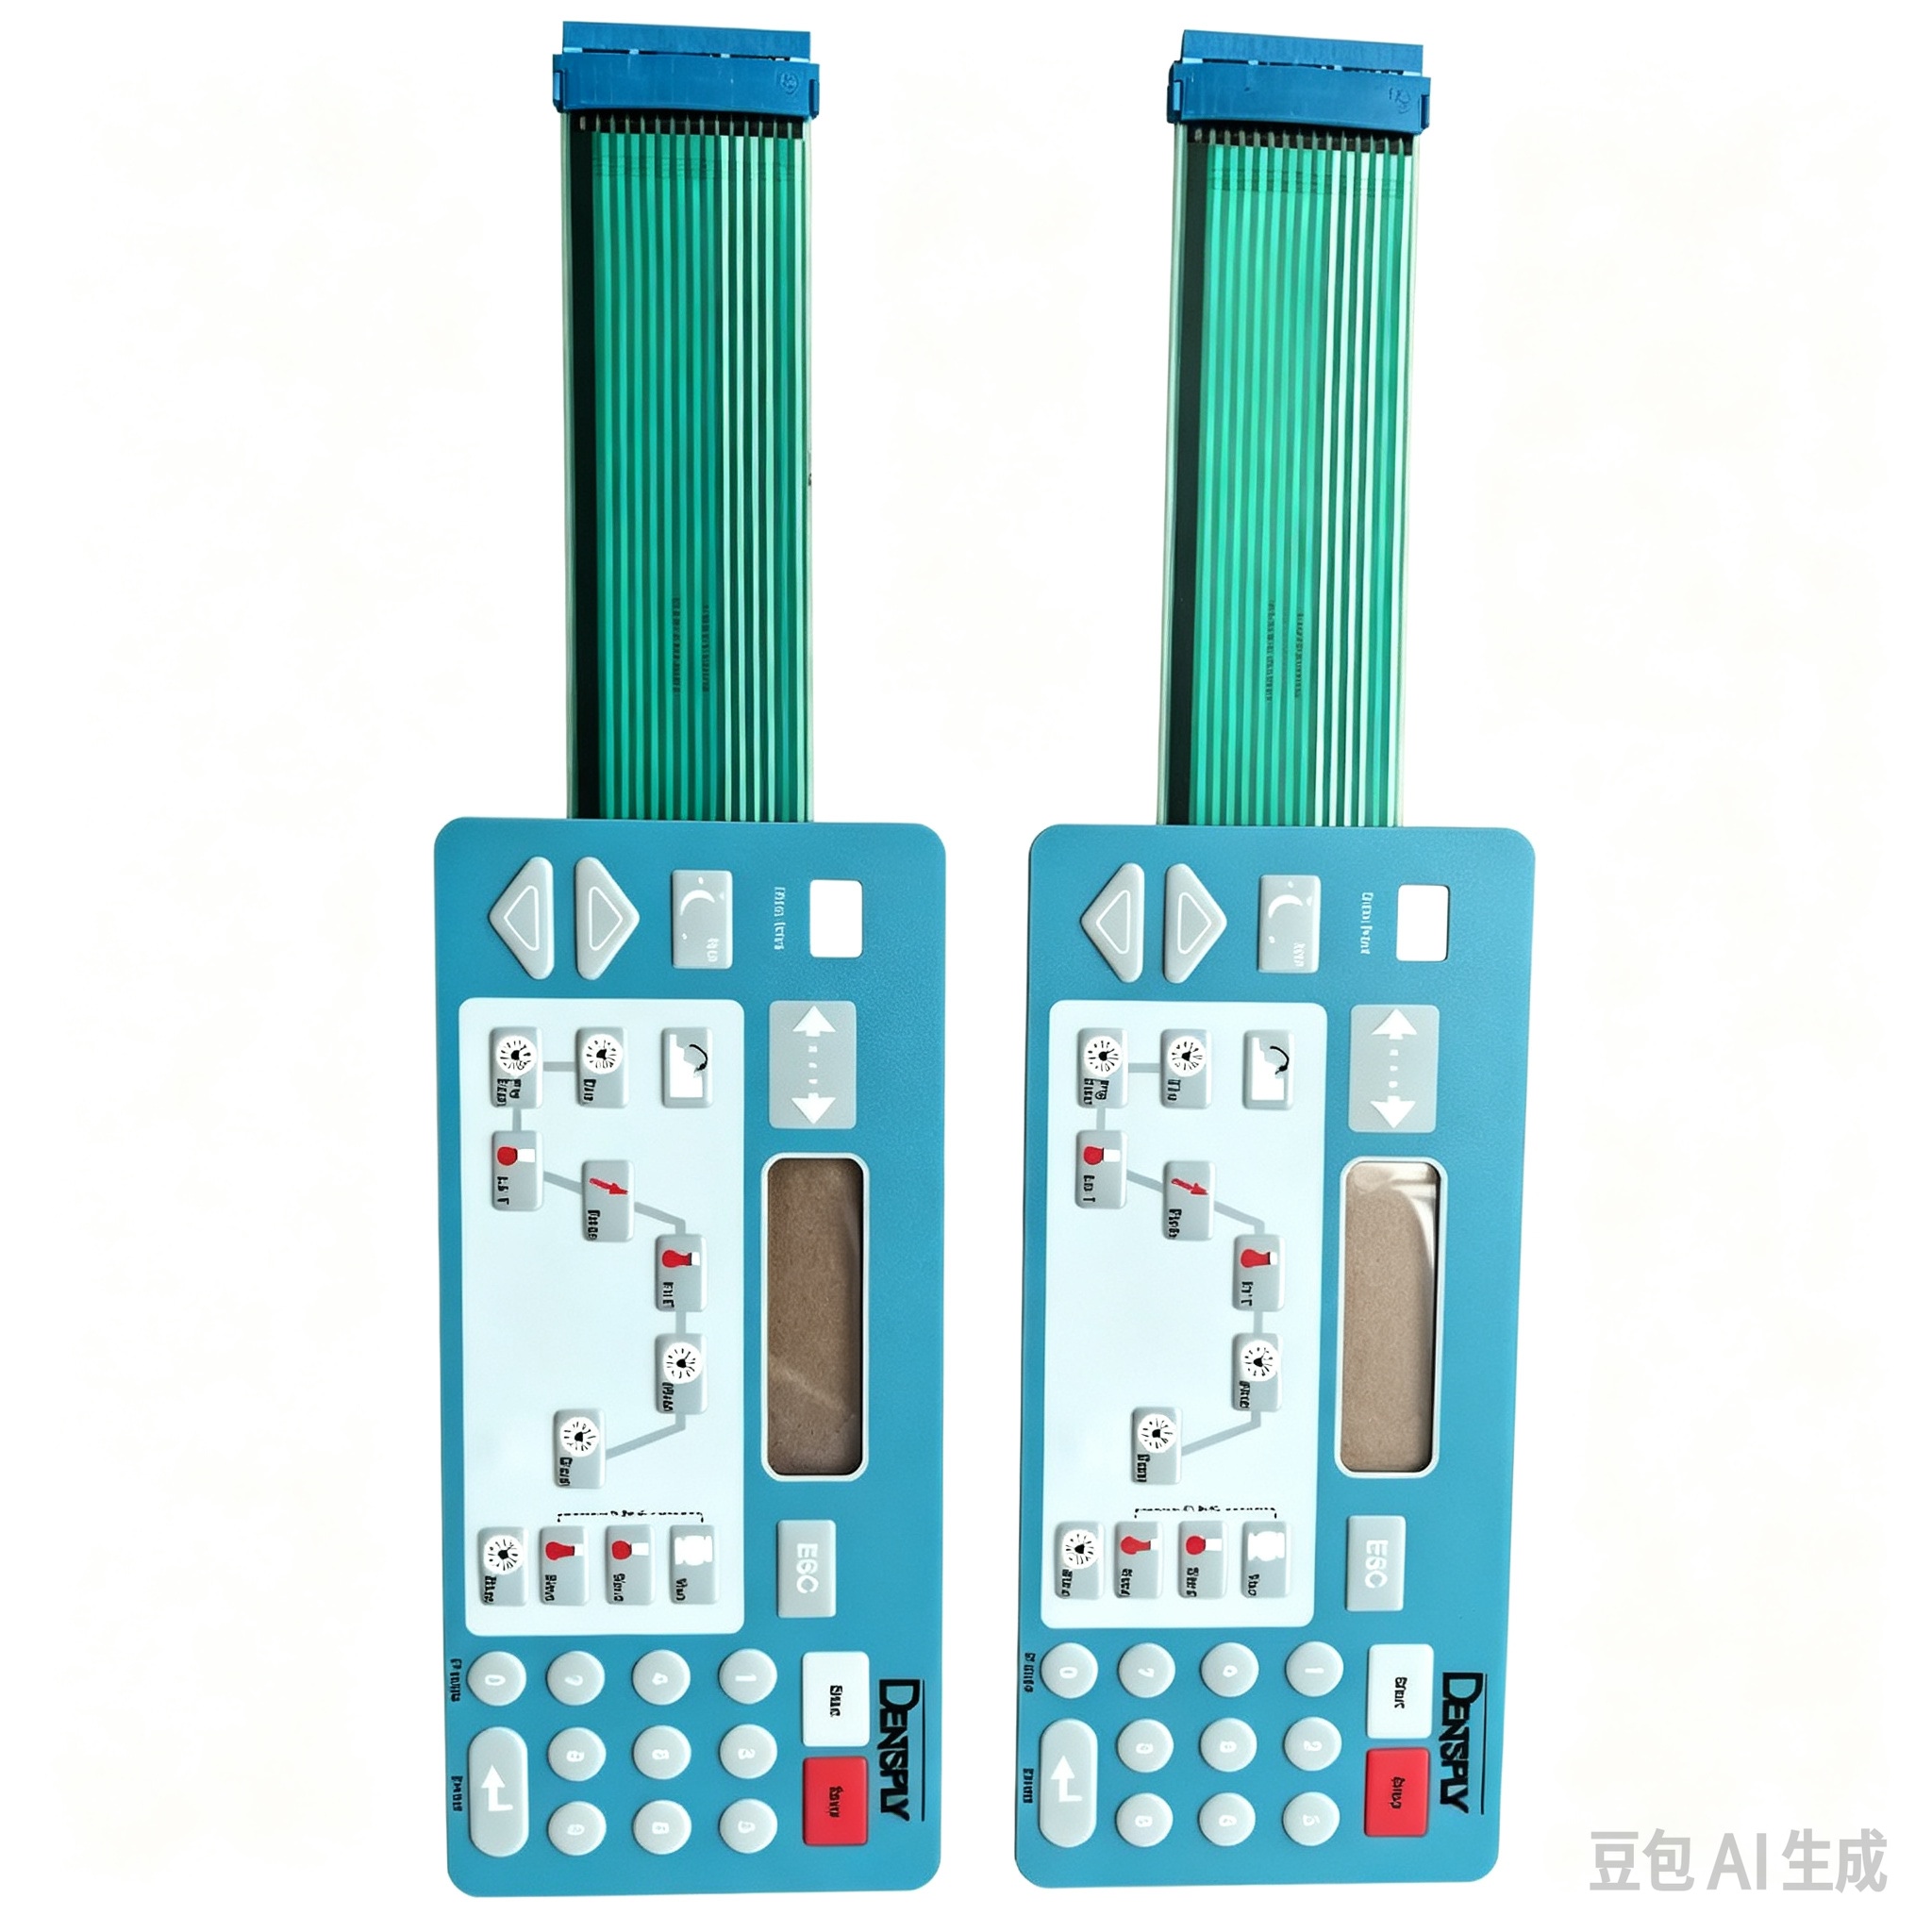
Factory Custom Waterproof Polyester Membrane Switch On Off Button Panel Autotex PET
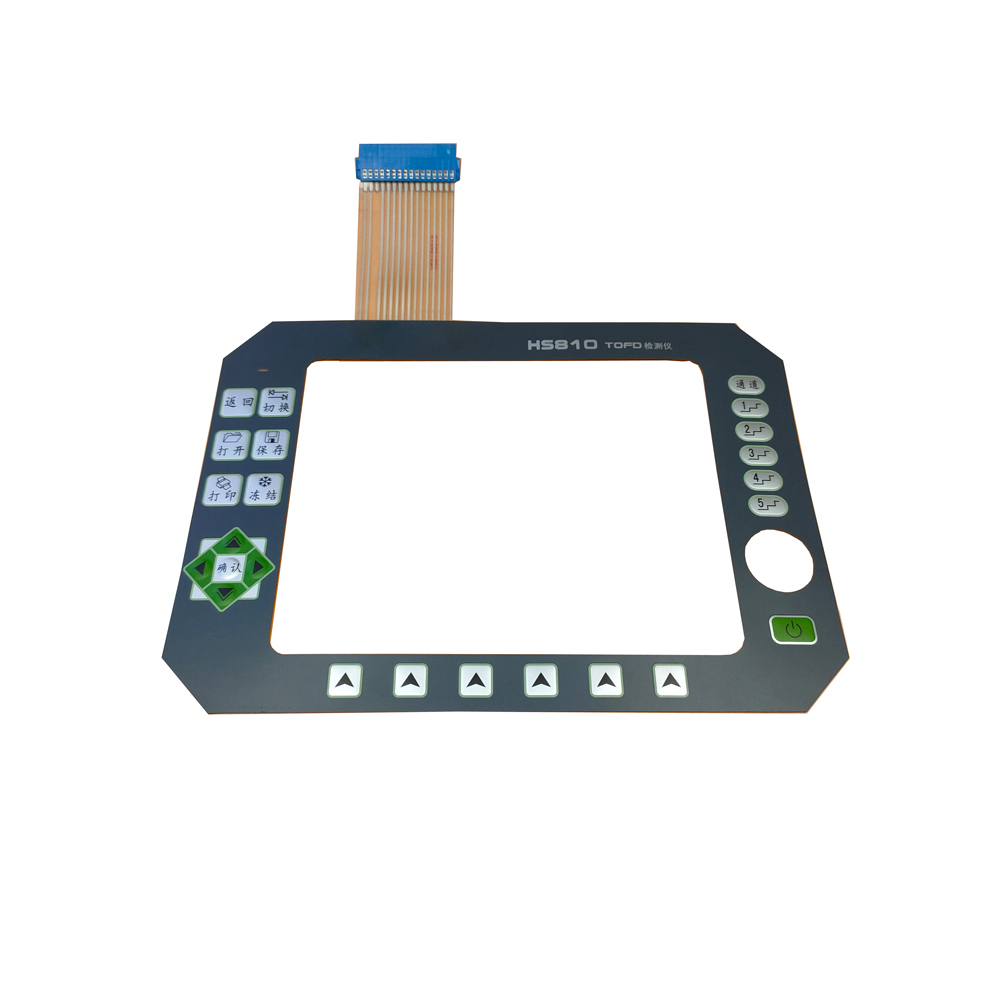
Meiborui Custom PBT Keyboard Cap Silkscreen Printed Waterproof Adhesive Sticker Computer Parts
MEIBORUI MBR PBT Keyboard Cap PET Membrane Keypad Custom Color Silkscreen Printing Replacement
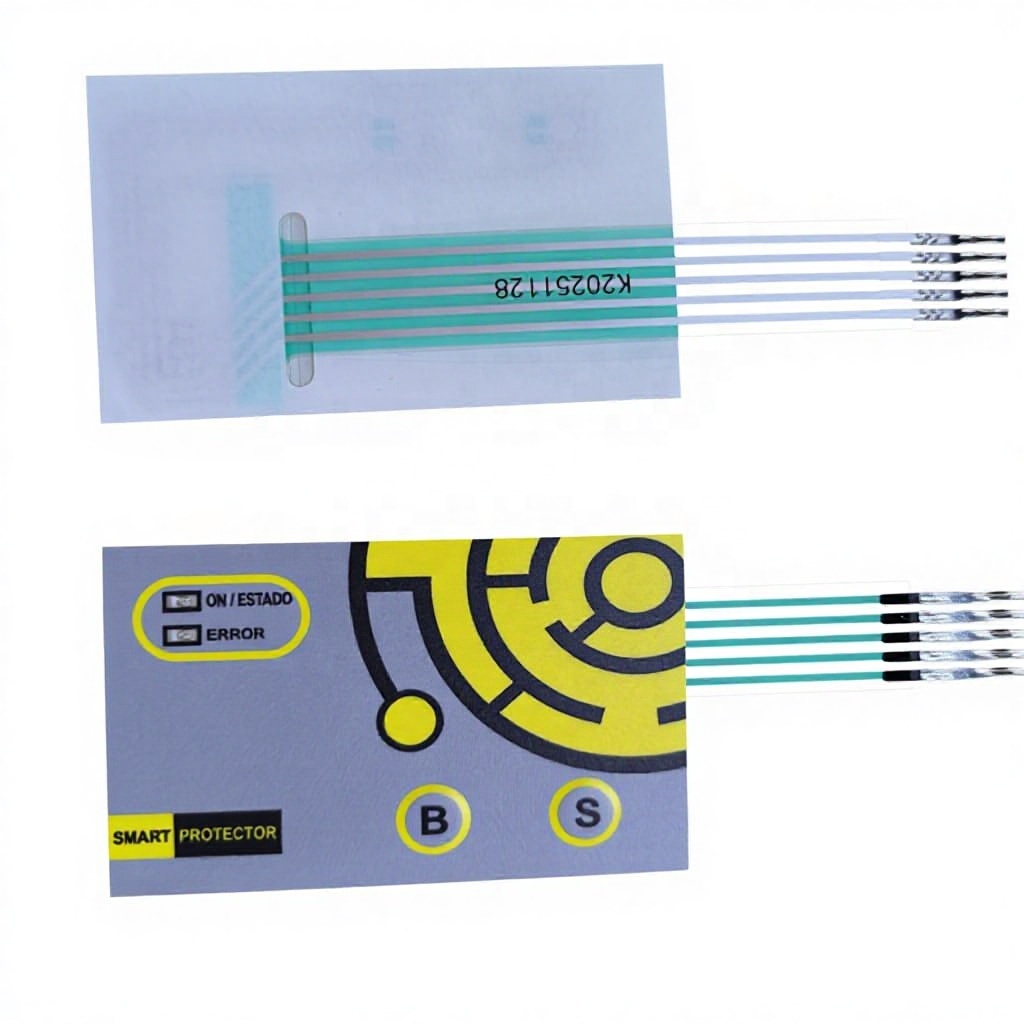
Fast Delivery OEM Waterproof Membrane Keyboard Mechanical Switch Compatible Factory Direct Supply
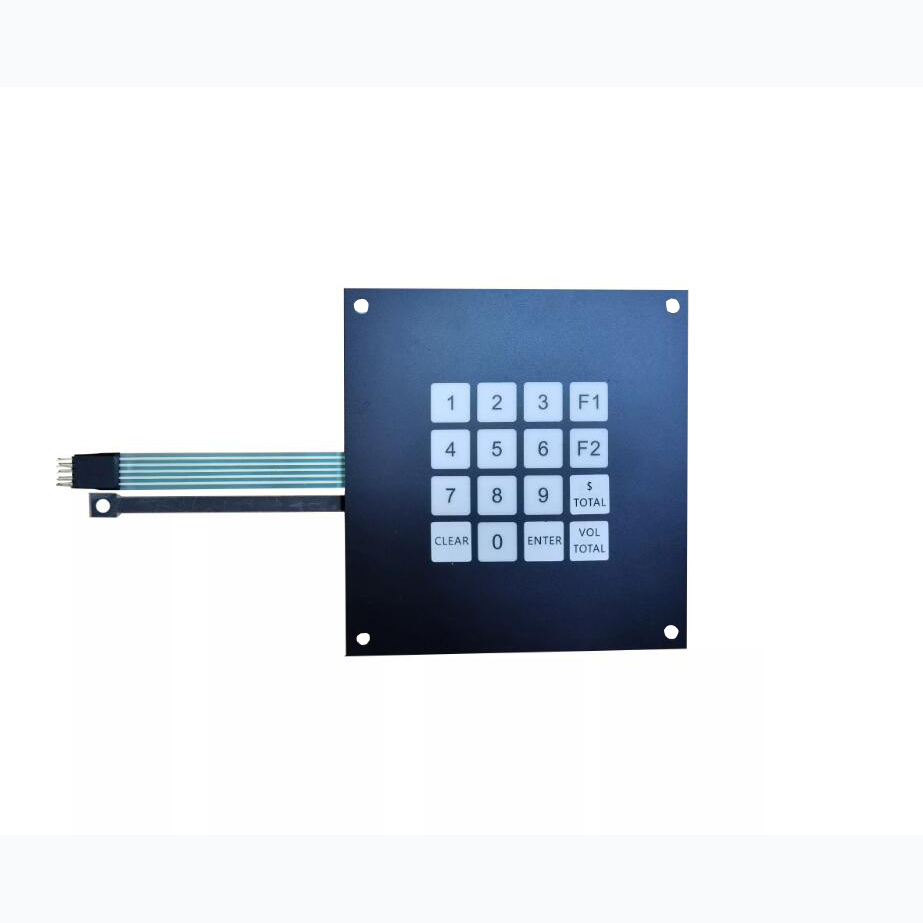
Custom Fuel Dispenser Oiling Machine with Membrane Keypad and Remote Controller ISO9001 Built
Engineering Anatomy: PCB-Backed vs. Flexible Silver Keypads
Why modern Memphis OEM applications in mission-critical logistics, automated warehousing, and medical instrumentation have shifted from flexible polyester circuit loops to rigid FR-4 backed human-machine interfaces (HMIs).
FR-4 Glass-Epoxy Core Rigidity
Traditional membrane switches utilize screen-printed conductive silver flakes on flexible PET films. While cost-effective for static applications, they suffer from trace fracture under continuous cyclic bending and thermal shock. A PCB-backed keypad incorporates single, double, or multi-layer FR-4 glass-reinforced laminates (thickness range: 0.4mm to 3.2mm) with 1oz to 2oz electro-deposited copper traces. This eliminates physical flexing behind the snap domes, guaranteeing a flat, unyielding contact surface for uniform actuation forces across every key.
Direct Surface-Mount (SMT) Integration
Flexible PET circuits cannot withstand high-temperature lead-free reflow soldering (260°C peak), forcing engineers to use conductive epoxy bonding for micro-LEDs, which exhibits high failure rates under mechanical vibration. By migrating to a rigid PCB backer, surface-mount components—including multi-color reverse-mount LEDs, optical sensors, light-guide films (LGF), buzzer drivers, decoupling capacitors, and integrated microcontrollers (MCUs)—are soldered directly onto the rear layer using standard automated pick-and-place lines.
Hermetic Ingress & Blind-Mate Termination
Polyester tail ribbons that exit from switch perimeters present vulnerability points where moisture, hydraulic fluids, and isopropyl cleaning agents wick into the switch interior. PCB-backed designs utilize blind-mate board-to-board connectors, right-angle shrouded headers, or threaded PEM studs pressed directly into the board. This allows gasketed perimeter seals (3M 300LSE / 467MP acrylic adhesives or silicone O-rings) to create IP67/IP68 and NEMA 4X hermetic barriers against harsh washdowns.
PCB Backed Keypad Applications Across Greater Memphis
From the automated sortation decks of the Memphis International Airport logistics corridor to orthopedic surgical facilities along Shelby County's medical device alley, precision switch hardware drives regional productivity.
Air Freight & Automated Hub Sortation
Memphis hosts the world's premier cargo hub operations. High-speed conveyor matrices, automated dimensioning scales, and sorting carousels operate continuously 365 days a year. PCB-backed keypads integrated into human-machine sorting terminals deliver crisp, tactile feedback through four-legged stainless steel snap domes, preventing operator entry errors while handling over 5,000 package barcode overrides per shift.
Orthopedic & Surgical Medical Devices
Memphis is recognized globally as the capital of orthopedic device manufacturing. Operating room console interfaces and motorized surgical drill controllers demand bio-compatible, chemical-resistant front surfaces. Our Autotex XE polyester overlays with antimicrobially treated hardcoats withstand aggressive sterilizing wipe-downs with glutaraldehyde, quaternary ammonium, and bleach without micro-cracking.
Cold-Chain Logistics & Reefer Terminals
Pharmaceutical cold storage and refrigerated intermodal freight yards in Southaven and DeSoto County subject HMIs to rapid thermal transitions from -25°C blast freezers to +38°C outdoor humidity. Solid FR-4 core boards paired with internal breathing vents and silica desiccating channels prevent internal condensation, contact oxidation, and false-trigger capacitance faults common in flex circuits.
AgTech & Mississippi Delta Processing
Mid-South agricultural machinery, grain handling elevators, and cotton gins generate heavy particulate dust, vibration, and hydraulic fluid splash. PCB-backed panels with mechanical fastener studs provide the mechanical rigidity needed to seal against cast aluminum enclosures, preventing conductive dust ingress that could short out sensitive digital I/O lines.
Engineering Spec Sheet: Keypad Technology Comparison
Quantitative benchmarks to assist engineering sourcing managers in evaluating substrate integrity, contact resistance, and life-cycle durability under harsh conditions.
| Performance Parameter | Rigid FR-4 PCB-Backed Keypad | Standard Flex Silver Circuit | Copper Flex Circuit (FPC) | Solid Metal Backer Assembly |
|---|---|---|---|---|
| Base Substrate Material | Glass-Reinforced Epoxy (FR-4) | Polyester Film (PET) | Polyimide (PI / Kapton) | Aluminum / Stainless Alloy |
| Conductor Metallurgy | Electro-Deposited Copper (ENIG Plated) | Screen-Printed Silver Carbon Ink | Etched Rolled Annealed Copper | Separate Sub-panel Layer |
| Contact Resistance | < 0.1 Ω (Ultra-Low) | 10 Ω to 100 Ω (Moderate/High) | < 0.5 Ω (Low) | Depends on circuit layer |
| Actuation Lifetime | > 3,000,000 to 5,000,000 Cycles | ~500,000 to 1,000,000 Cycles | > 2,000,000 Cycles | > 5,000,000 Cycles |
| SMT Component Reliability | Superior: Reflow Solder Joint | Vulnerable: Conductive Epoxy | High: Reflow Solder Joint | Rigid-Mounted SMT Base |
| Connector Termination | Shrouded Headers / Screw Terminals | ZIF / Berg Crimp Pitch Pins | Gold-Plated ZIF Tails | Direct Enclosure Threaded Pass |
| EMI/RFI Shielding Potential | Direct Grounded Copper Plane | Screened Carbon/Silver Grid | Cross-Hatched Copper Plane | Inherent Metal Backplate Attenuation |
| Thermal Range (Continuous) | -40°C to +105°C | -20°C to +65°C | -40°C to +85°C | -40°C to +125°C |
2025–2030 Trends in Mid-South Keypad & HMI Sourcing
How supply chain executives in Tennessee and Northern Mississippi are streamlining manufacturing timelines, cutting lead-times, and mitigating supply volatility.
Hybrid Rapid-Air Supply Lines
With Memphis International Airport operating as the continent's most active cargo hub, regional equipment builders have abandoned slow ocean-freight models. By partnering directly with advanced Asian manufacturing bases operating proprietary tooling and SMT assembly lines, Memphis engineering firms receive prototype revisions within 7 days via air express, reducing product realization cycles from months to weeks.
Total Turnkey Box-Build Integration
OEM engineering departments are decreasing vendor count. Sourcing managers now reject purchasing raw membrane switch overlays, bare PCBs, silicone keymats, and mounting backplates from disparate suppliers. Modern demand dictates complete, pre-tested sub-assemblies—featuring integrated LCD windows, optical clear adhesive (OCA) lamination, soldered micro-wire harnesses, and functional bench validation.
Anti-Microbial & Harsh Washdown Shift
Following post-pandemic cleanability directives across healthcare distribution centers and clinical laboratories, non-porous textured polyester overlays featuring chemically bonded microbicidal coatings have surpassed standard polycarbonate. These formulations prevent silver ionic loss during harsh chemical sanitization, prolonging equipment life across Shelby County facilities.
TAVO / Meiborui Engineering & Production Prowess
Tracing our heritage back to 1990, we deliver German-aligned manufacturing precision, verified by Intertek and governed under strict ISO 9001:2015 quality protocols.
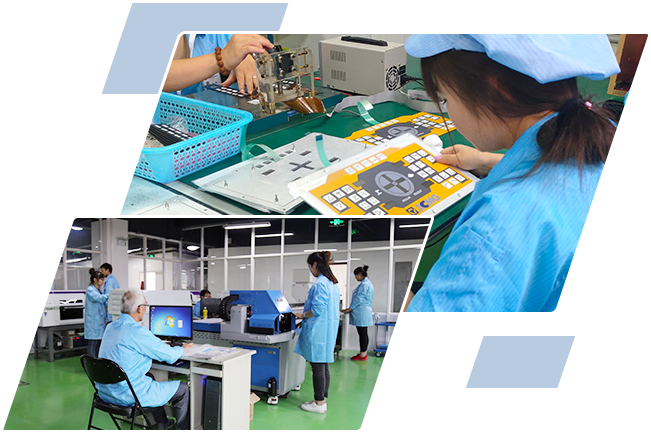
Closed-Loop Precision Under One Roof
Every stage of switch assembly—from CAD gerber engineering, silkscreen printing, and high-speed digital UV curing to CNC dome retainer stamping, laser profiling, and 100% electrical computer matrix testing—is executed internally. Our production infrastructure across Hebei and Huizhou isolates your build from external subcontractor delays.
With more than 30 senior technical engineers boasting 15+ years of tactile membrane switch experience, plus a German technical partnership covering automated equipment alignment, our facility has delivered mission-critical assemblies to global Tier-1 leaders including Siemens, ABB, and Haier.
Frequently Asked Questions for Memphis Hardware Buyers
Actionable technical answers addressing DFM file submissions, lead times to Memphis, tooling amortization, and harsh environment testing.
What files are required to obtain a DFM analysis and quote for a PCB-backed keypad?
We require the front graphic overlay artwork in vector format (Adobe Illustrator .AI, vector .PDF, or CorelDraw .CDR) with defined Pantone color codes, along with the PCB electrical layer design in standard Gerber RS-274X format or Altium/Eagle schematics. If you have mechanical tolerances and enclosure mounting constraints, please include a 3D STEP or DXF file showing stud locations, cutouts, and connector orientation.
How fast can prototypes and production runs be delivered to our facility in Memphis?
Rapid prototyping runs (5 to 20 units) are typically engineered, manufactured, and bench-tested within 5 to 8 business days following drawing signoff. Utilizing express air freight directly through the Memphis International Airport (MEM) international cargo processing facility, shipments clear customs and arrive at your dock within 3 to 4 days, enabling end-to-end design turnarounds in under two weeks.
What tactile feedback options are available for operators wearing gloves?
In cold storage and heavy sorting facilities where personnel wear thick work gloves, tactile sensation is critical. We utilize stainless steel snap domes ranging from 12mm to 20mm with actuation forces between 350g to 550g (snap ratio > 50%). When paired with custom rim-embossed or pillow-embossed polyester overlays, users receive an unmistakable mechanical click, eliminating double entries.
How does your factory qualify long-term reliability against environmental stress?
Our internal testing laboratory features computer-controlled button life-cycle testers (verifying switches to 1M–5M cycles), programmable high/low temperature humidity chambers (-40°C to +150°C), xenon arc accelerated UV aging cabinets, and automatic salt fog chambers (ASTM B117 standards). We guarantee our switch contact points against plating corrosion, contact bounce, and silver migration.
Do you support lower NRE costs and low-volume pilot production runs?
Yes. Unlike traditional commodity membrane vendors that enforce restrictive minimum order quantities (MOQs) of 5,000+ pieces, our facility leverages precision digital UV flatbed printing (Mimaki series) and automated laser die-cutting. This eliminates hard tooling requirements for short-run prototypes and pilot batches (50 to 500 units), substantially reducing up-front NRE capital costs.
Connect With a Senior HMI Design Specialist
Upload your CAD gerbers, key layouts, and enclosure schematics. Receive a comprehensive DFM review, stackup diagram, and formal factory-direct quotation within 24 hours.